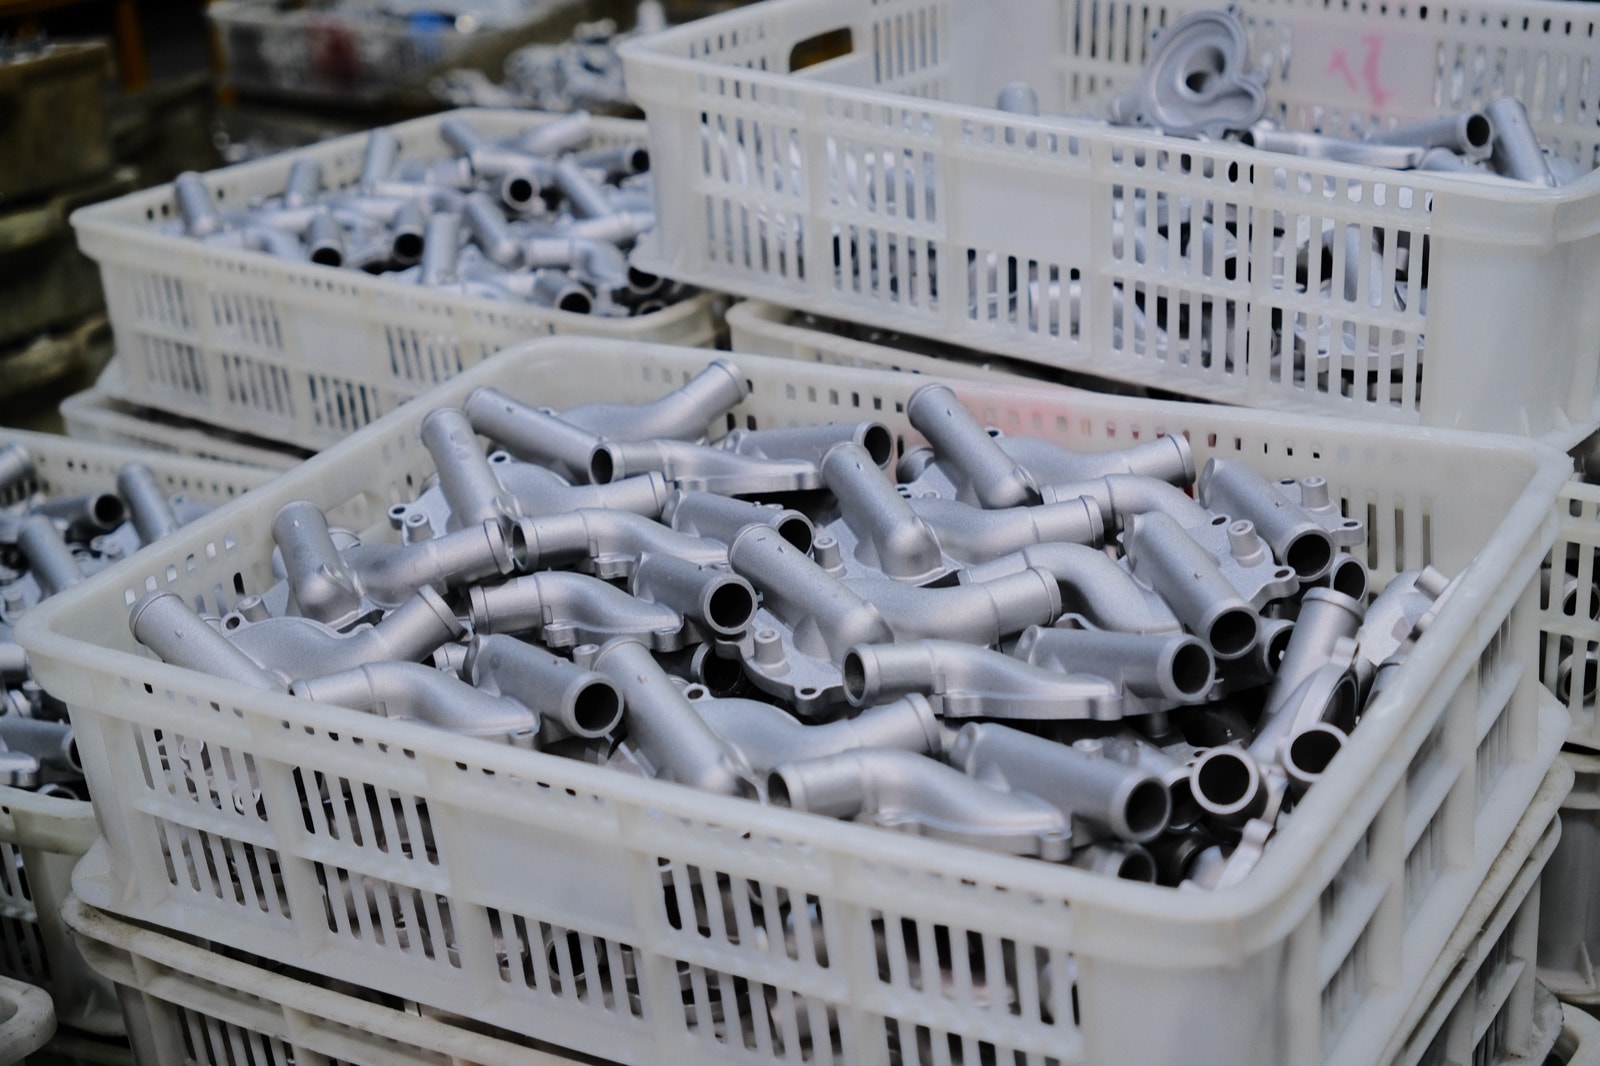
INDUSTRIES SERVED
Where our die castings are used
Every sector asks something different of a die casting: motorcycles need sealing and true bores, locks need a flawless face and strength, heat sinks need thin fins and flat faces, robot housings need coaxial bearing bores and low weight. We set tooling, process and inspection to what each sector demands. Each sector page sets out the parts we make for it, the cases and the capabilities behind them.
- Supplying OEMs in volume since 2003
- Ten 160–800 t machines, zinc and aluminum
- Tooling to assembly under one roof
- ISO 9001:2015 quality system
SECTORS
Browse by sector
Each sector has its own page setting out the parts we make for it, the figures we hold, and the cases — or the same-requirement production parts — behind them.
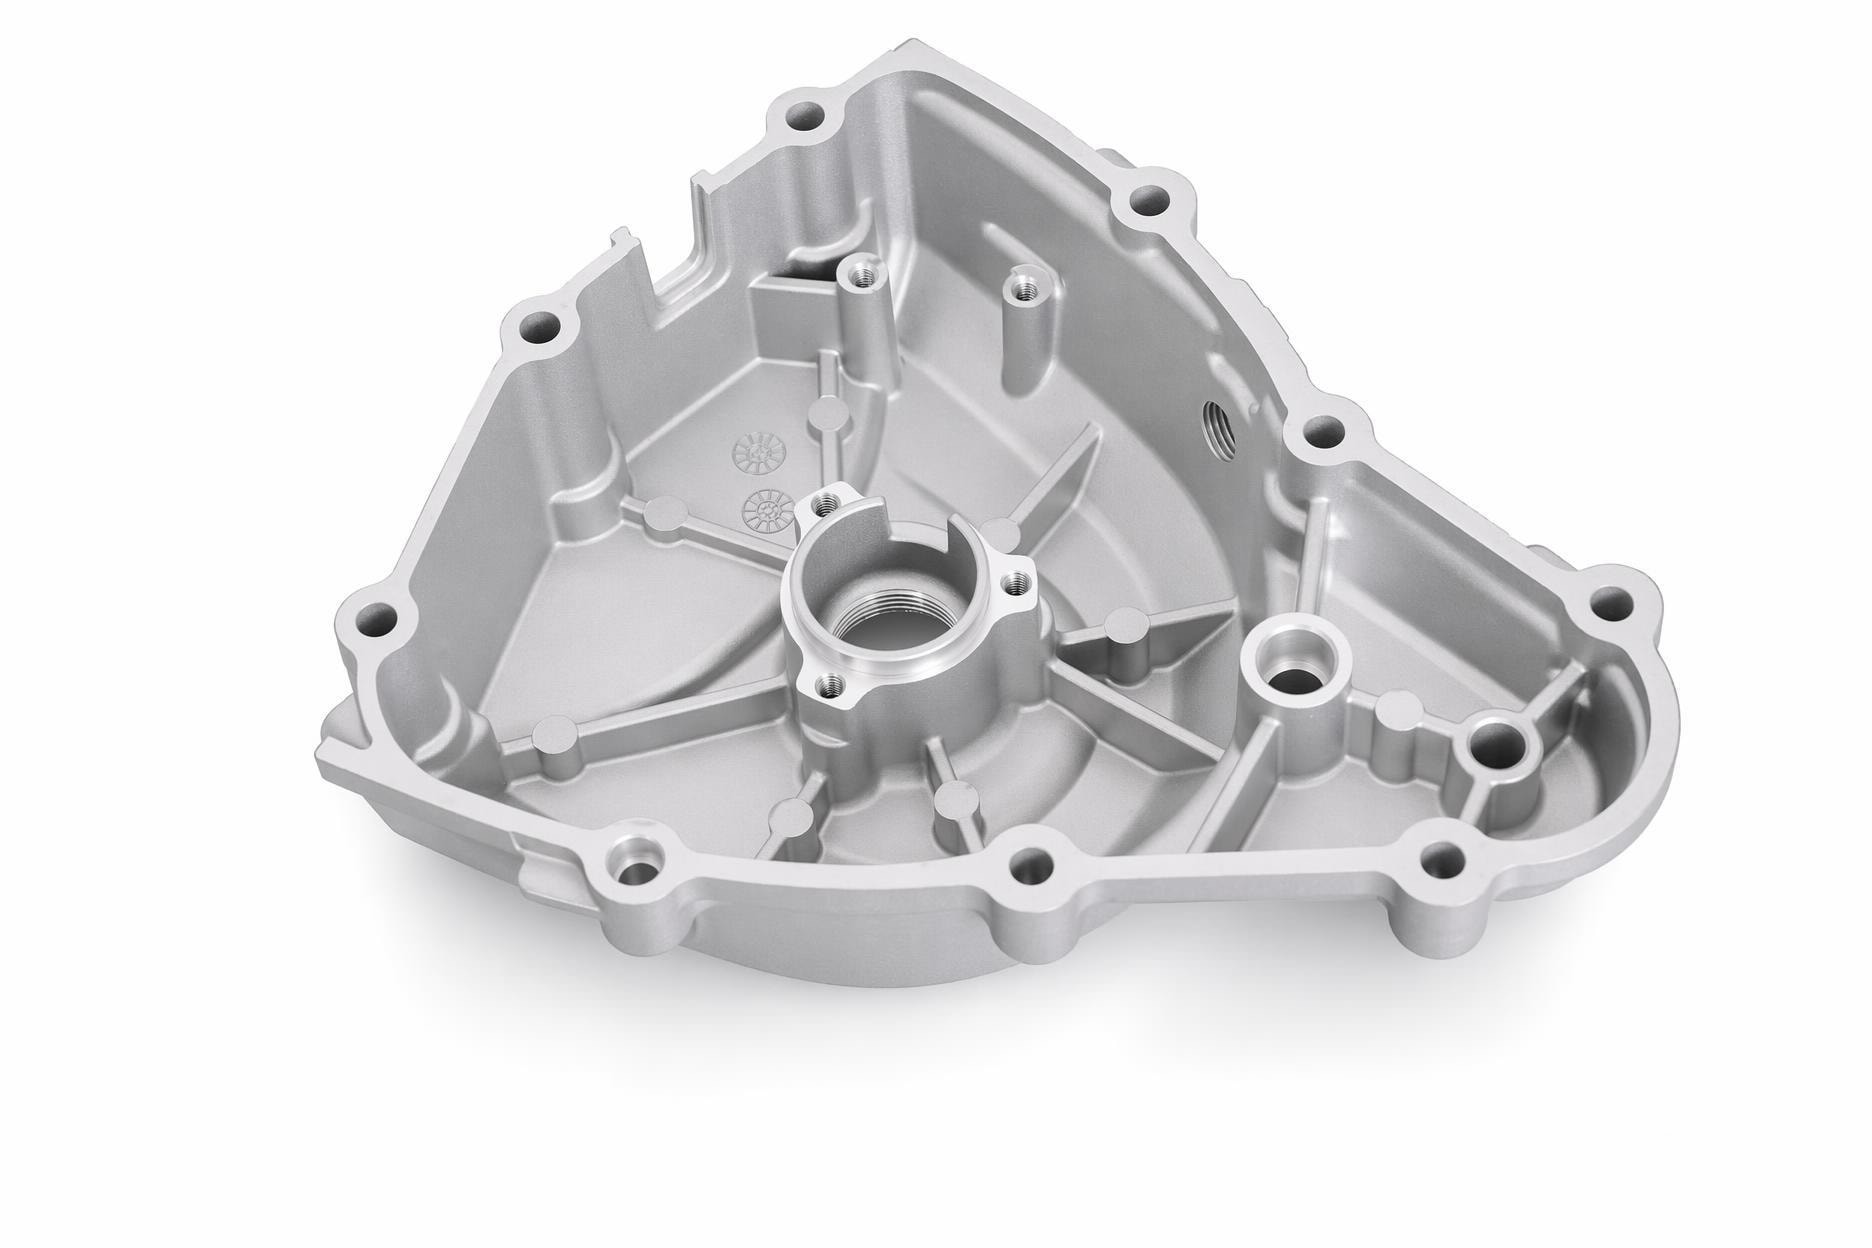 01Motorcycle & Two-WheelerPPAP / APQP on request · 100% leak tested
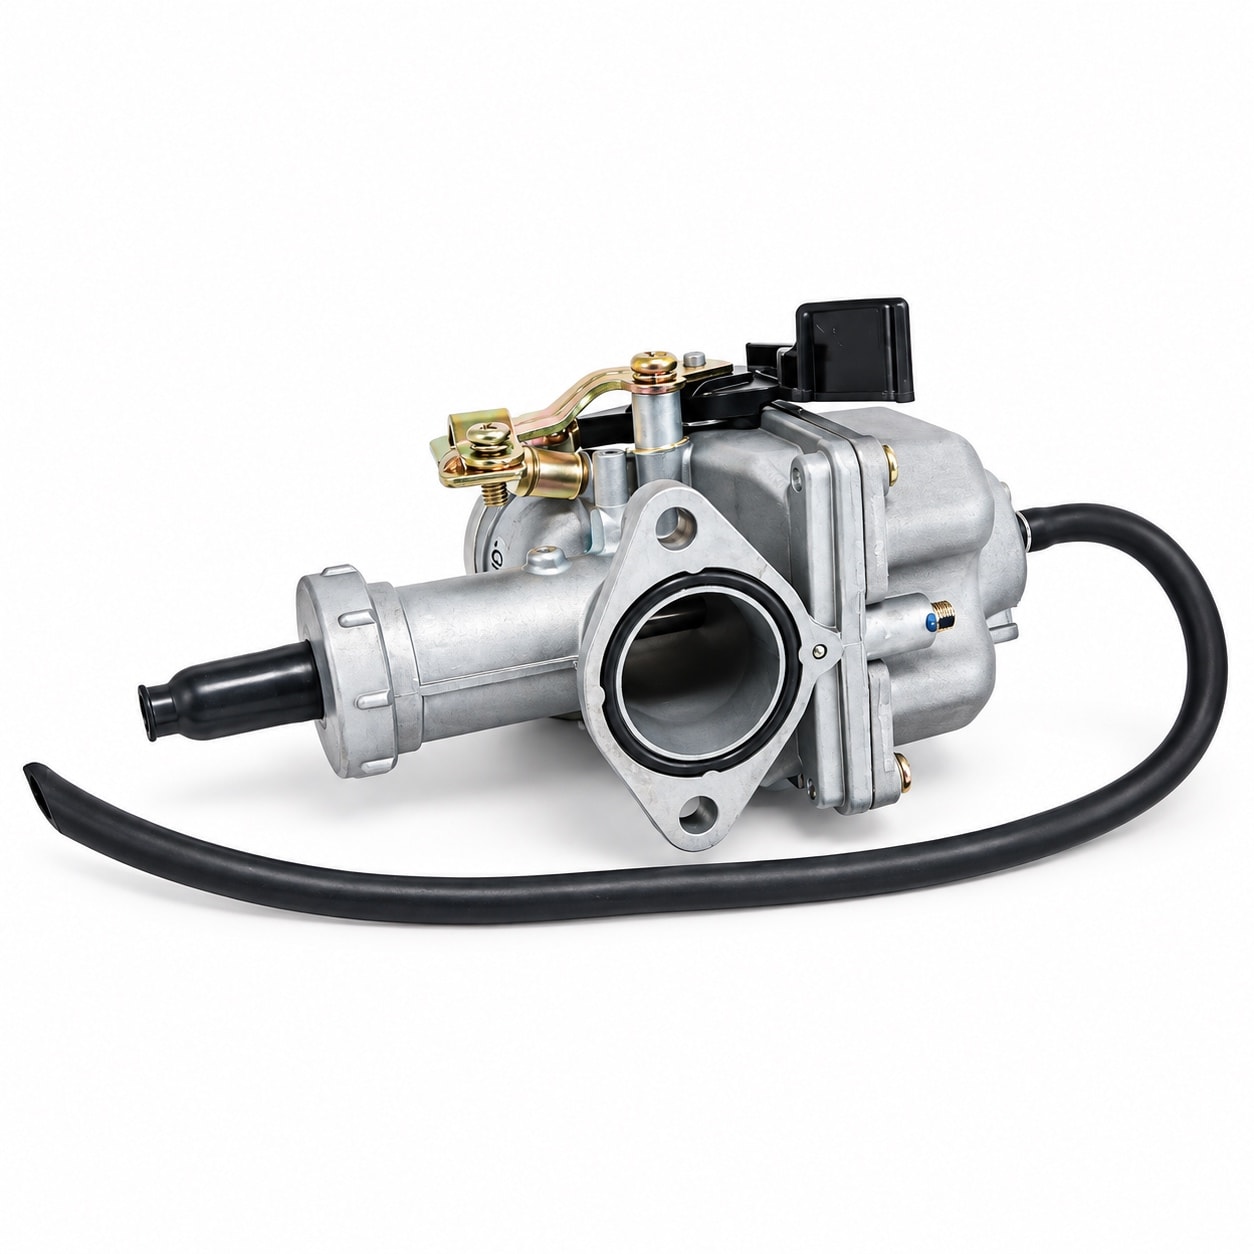 02General Power & Garden Machinery3,000,000 / year · 100% flow tested
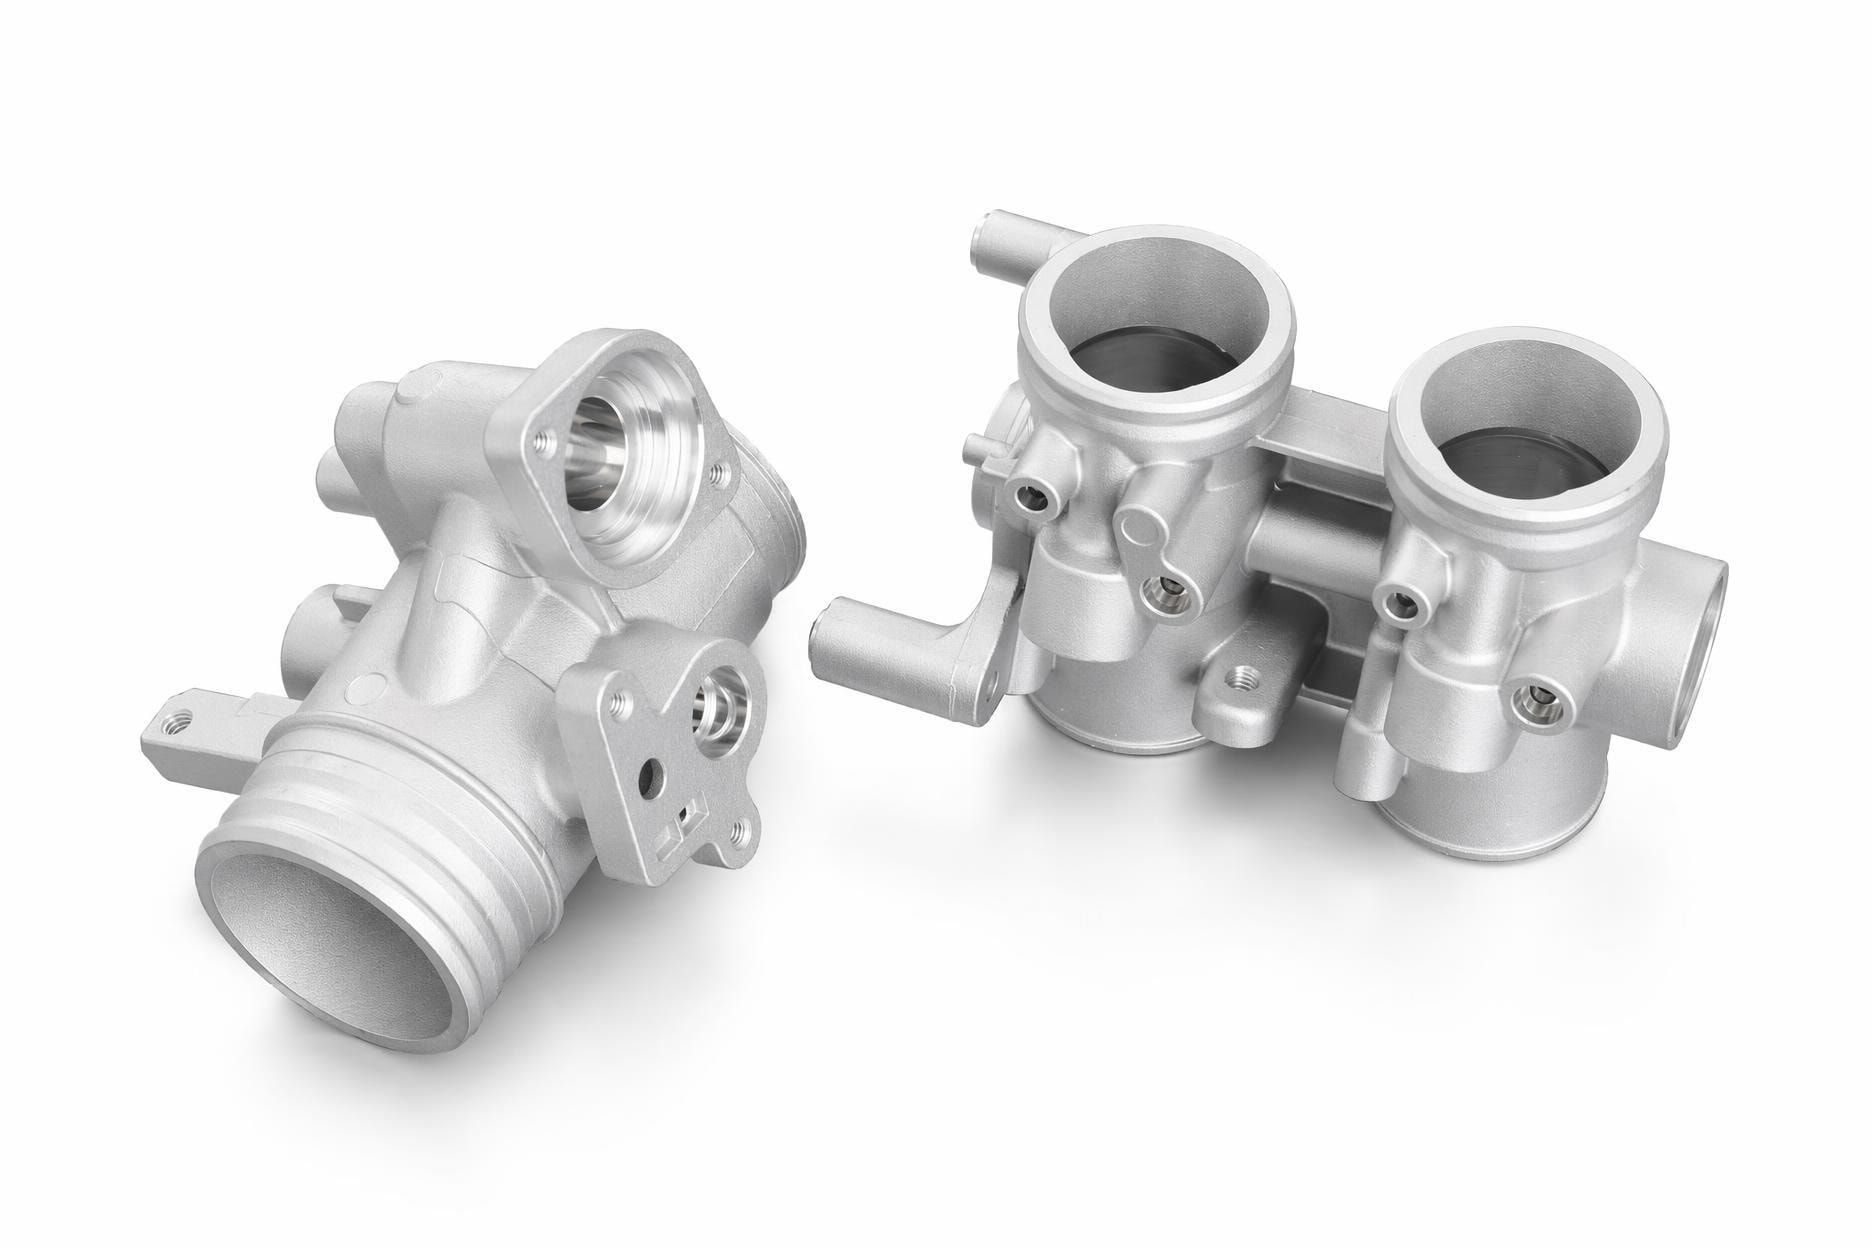 03Pumps, Valves & Fluid ComponentsLocal squeeze · 100% leak tested · <0.5% leak rate
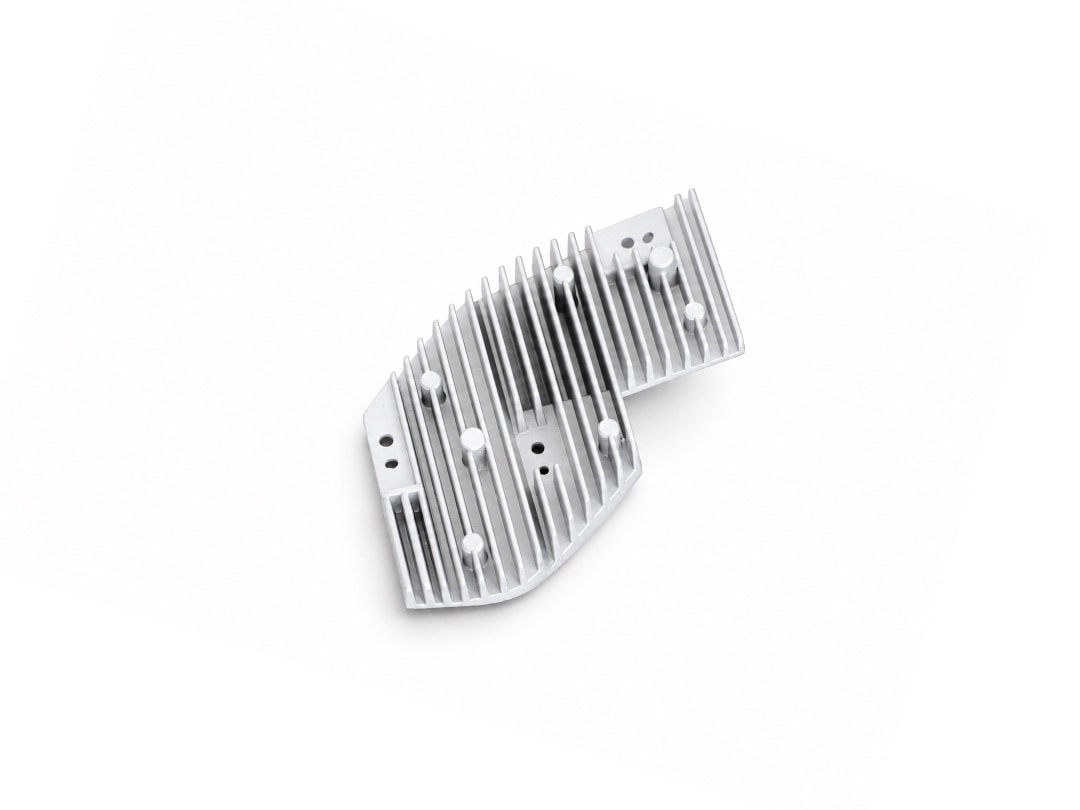 04Heat Sinks & Structural EnclosuresFins 1.5–2.5 mm · 0.05 mm/100 mm flatness
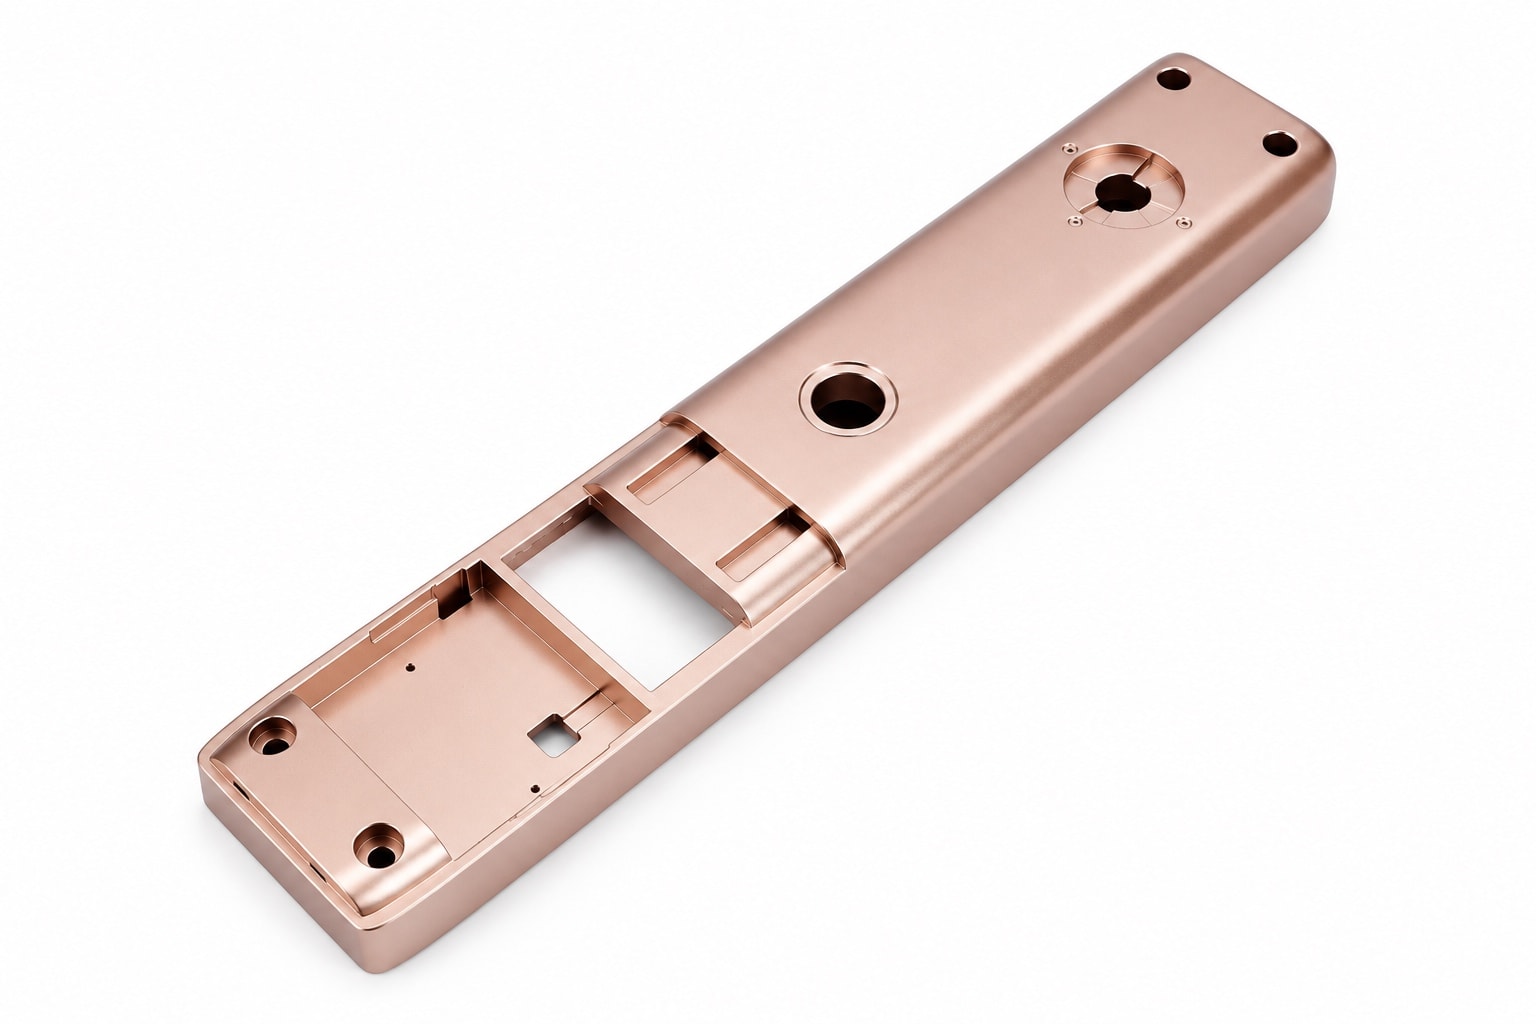 05Smart Locks & Door HardwareZamak 3/5 · ZA-12 · In-house PVD and powder coat
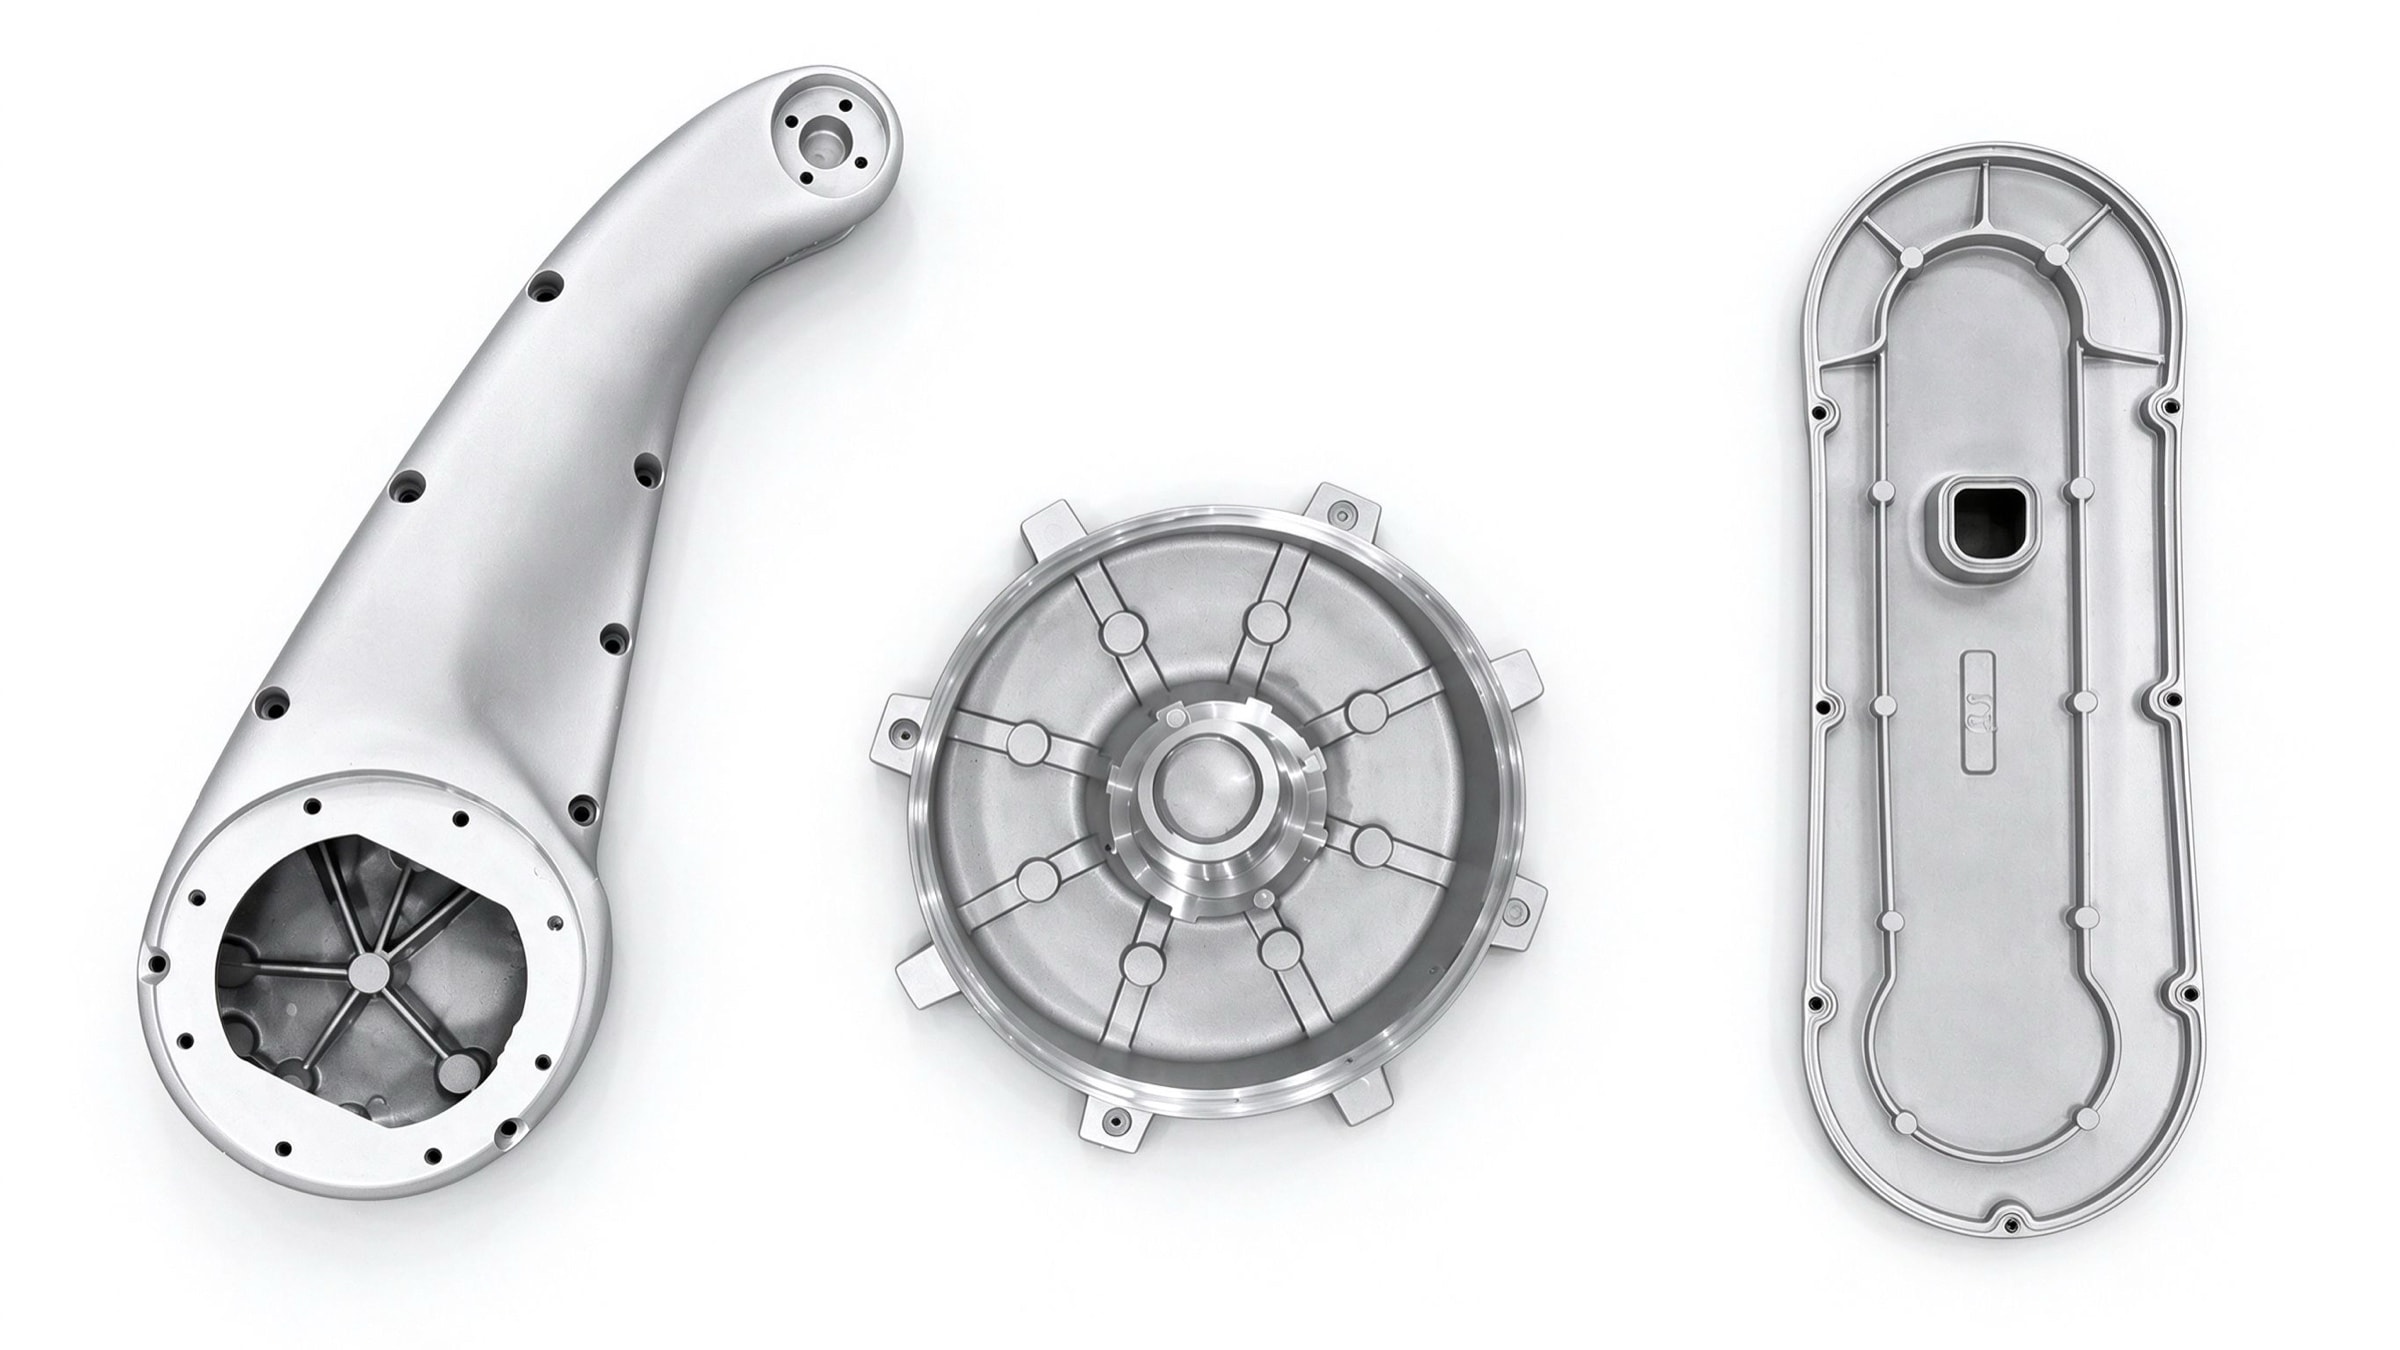 06Robotics & Automationφ0.05 mm bore coaxiality · CMM inspected
CORE CAPABILITIES
Our core capabilities
Years of manufacturing across industries have given us proven core capabilities in the following four areas:
Pressure tightness
Sealed parts get gating and venting optimised at DFM, with local squeeze on heavy sections; every finished part is leak tested — at 0.25 MPa for 30 s, for example, leaks normally stay under 0.5%.
USED IN
About this capability →Precision and flatness
Critical bores in a single setup to φ0.05 mm concentricity and ±0.02 mm bearing seats; large covers split roughing and finishing with stress relief, holding joint faces within 0.08 mm.
USED IN
About this capability →Cooling fins and appearance
Fins of 1.5–2.5 mm at up to 6:1; zinc cosmetic parts with weld lines routed off the show face, and PVD, powder coating and anodizing done in-house.
USED IN
About this capability →Finished assemblies
Bought-out parts sourced and inspected, press-fits monitored in-line, and every assembly flow or leak tested — one supplier instead of several.
USED IN
About this capability →
Sectors not listed here are welcome too
Any zinc or aluminum die casting from 20 g to 5.5 kg that the process can make, we will look at. Send a drawing and at the DFM stage we come back with specific comments on wall, draft, sealing and tolerances, plus a quotation that includes the tooling plan.