JINXIONGMANUFACTURING
Die-cast parts in production

CASE STUDIES

Die casting cases: the problem, the method and the production data

All the cases below are real parts in series production, covering zinc and aluminum die casting, CNC machining, surface finishing and assembly. Each one sets out the technical problem the customer faced, how we controlled it in the process, and the measured figures once production settled.

Alloy
Industry
Part type
Process
Key requirement

26 / 26 cases

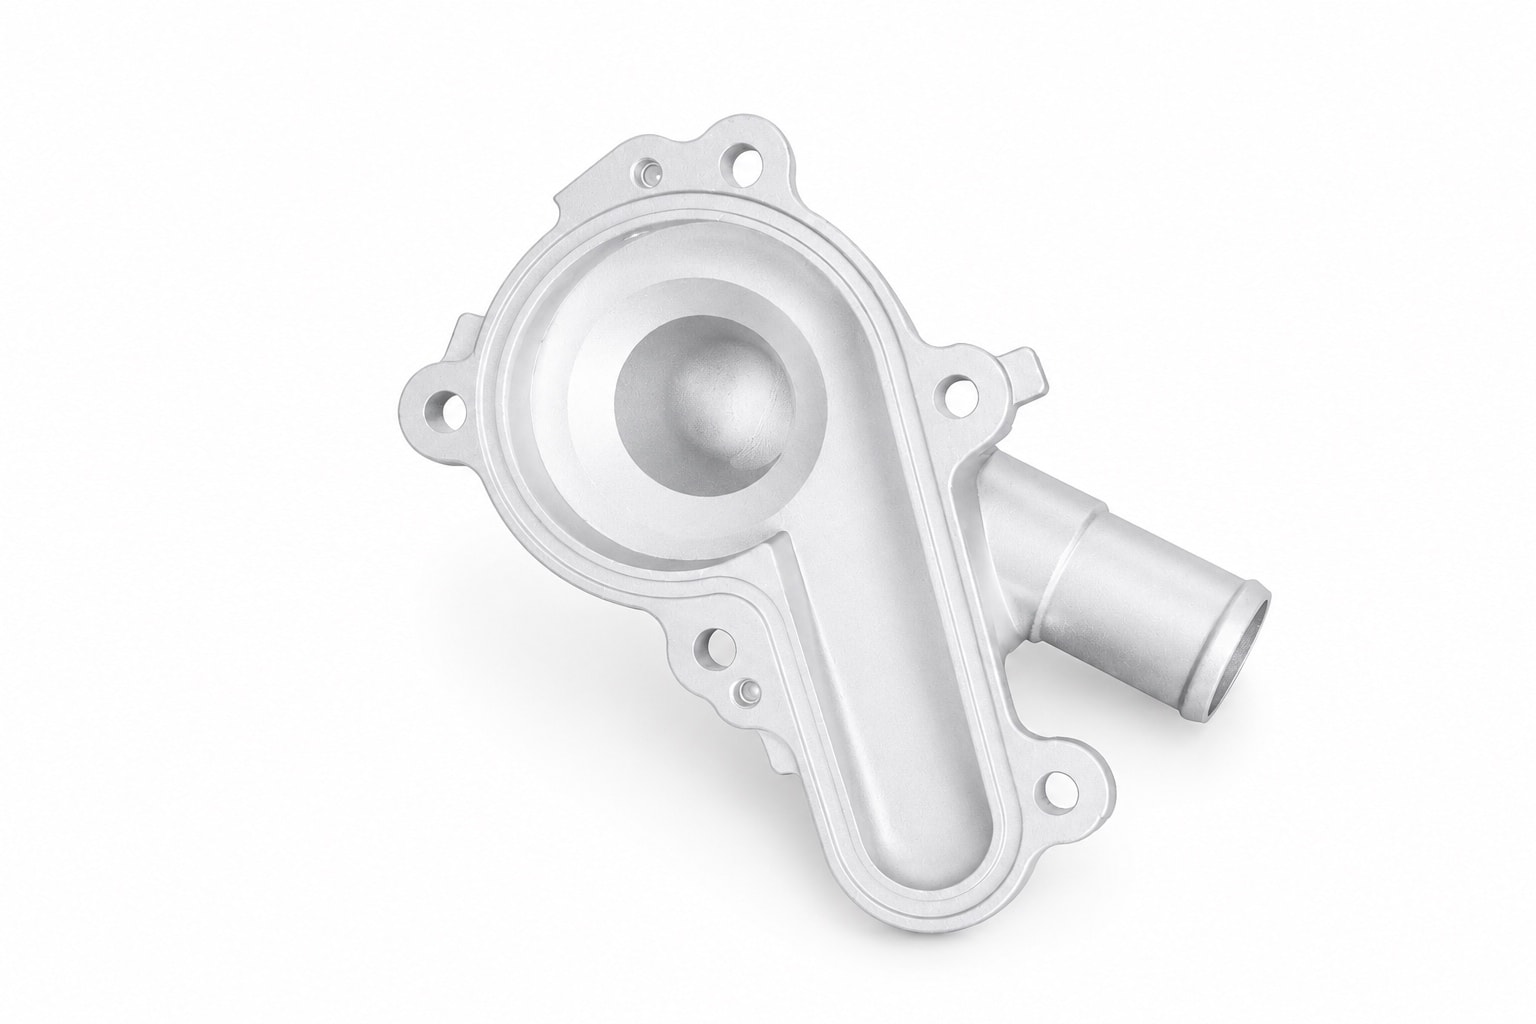
Motorcycle Aluminum Water Pump Housing

Motorcycle Aluminum Water Pump Housing

AluminumPumps, Valves & Fluid ComponentsDie castingCNC machiningPressure tightPrecision

Three suppliers had failed on this housing, with 6.2% leaking on test. A new parting line, reworked gating and venting, and one-setup boring cut leaks to under 0.5%.

ADC12 (JIS H5302) · 约 380 g
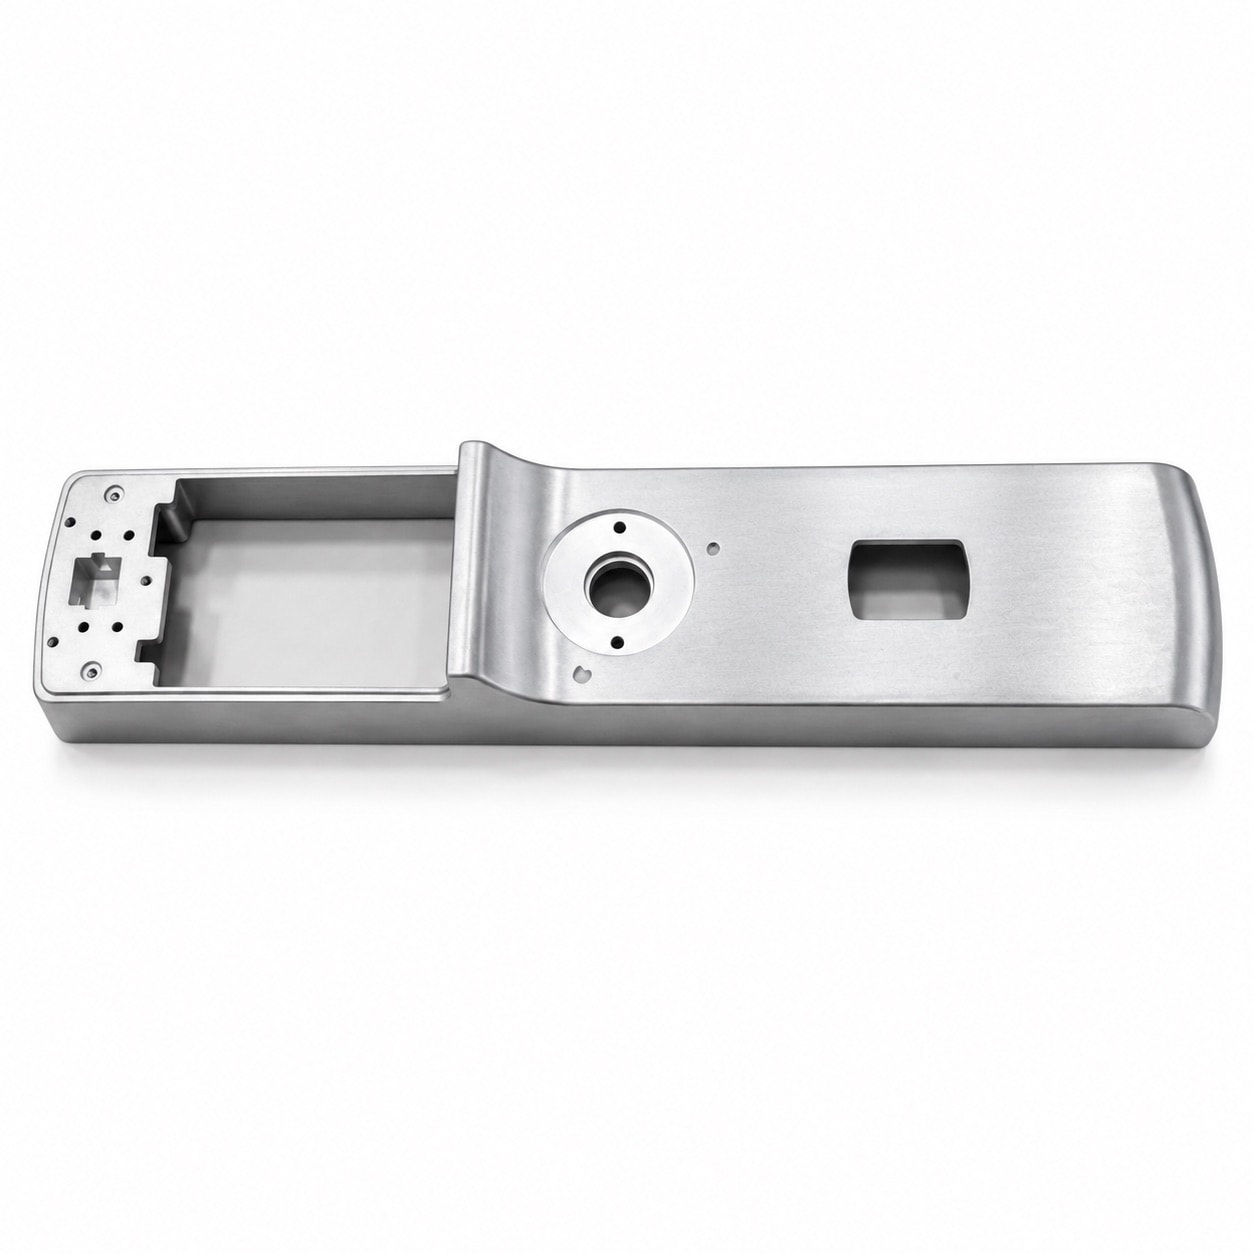
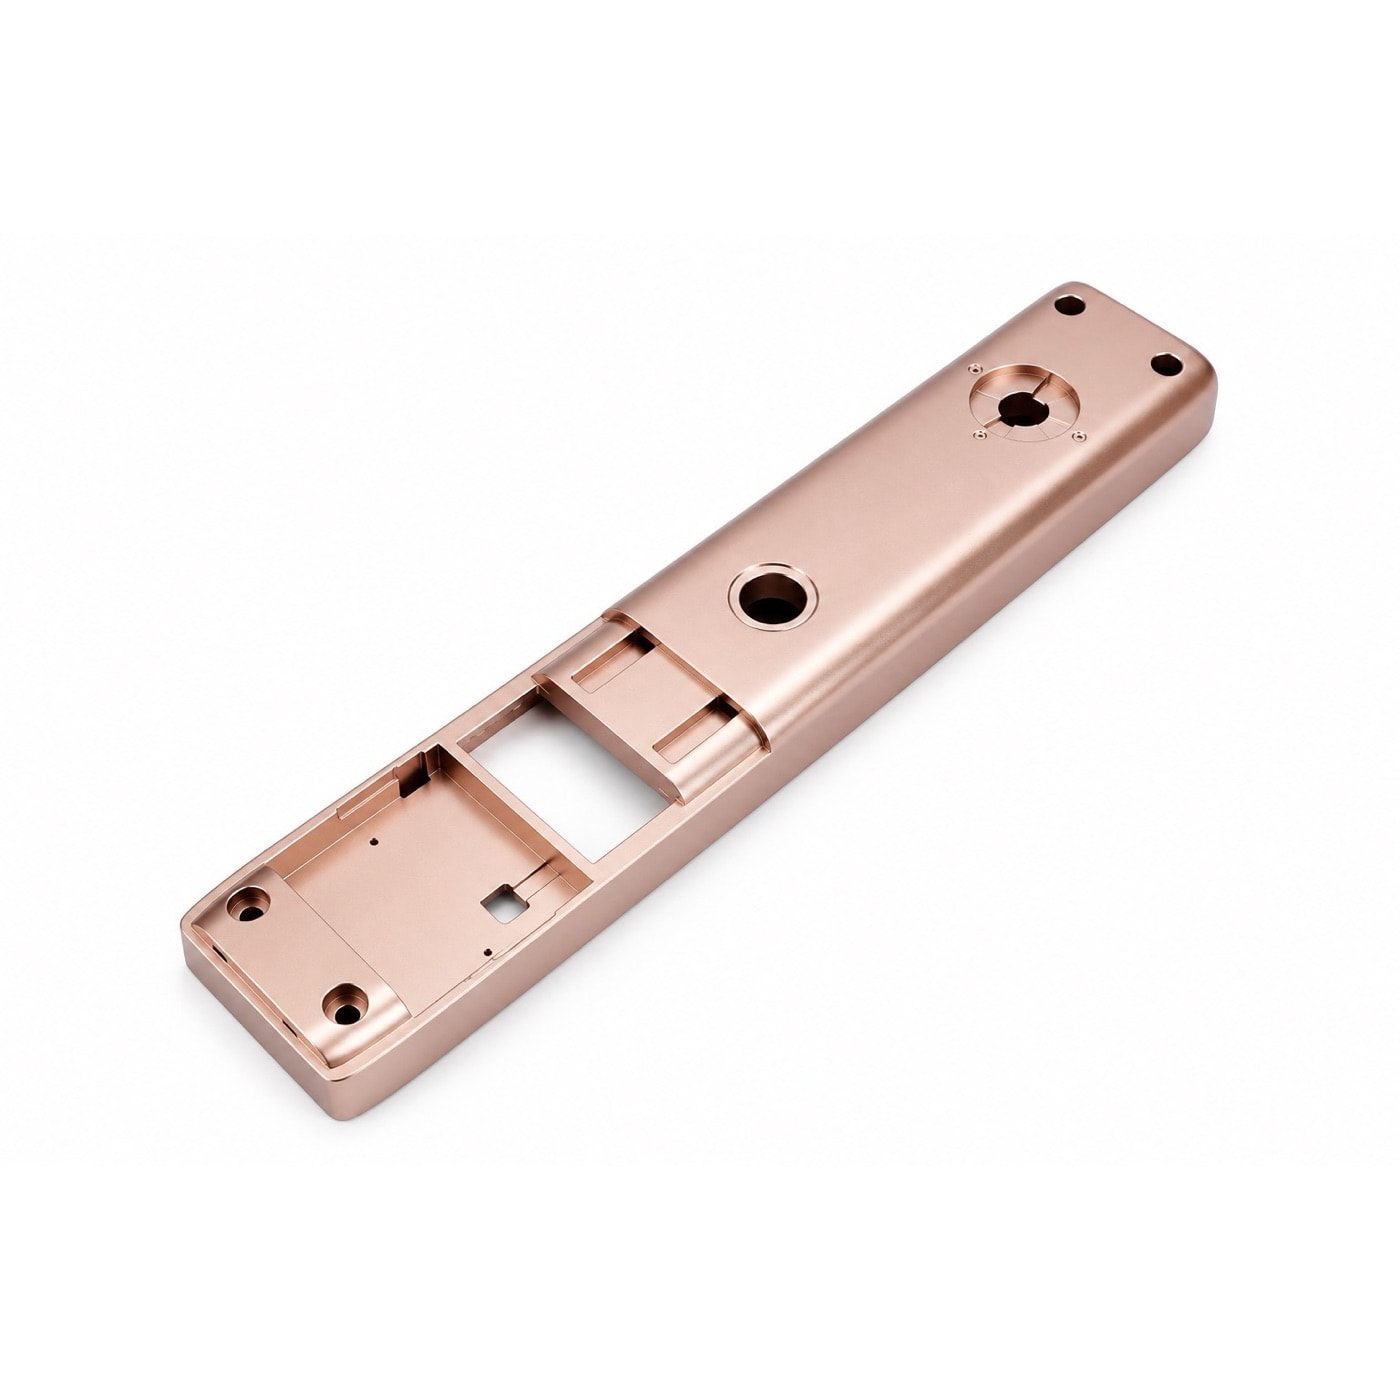
Zinc Alloy Smart Door Lock Front Panel

Zinc Alloy Smart Door Lock Front Panel

ZincSmart Locks & Door HardwareDie castingFinishingCosmetic

Plating blistered and flow marks marred the show face. Gates sized to each region and knit lines moved off it cut blisters from about 8% to under 0.5%.

Zamak 5 / YZZnAl4Cu1 (GB/T 13818-2024) · 约 450 g
Zinc Alloy Smart Lock Panel with Rose-Gold PVD

Zinc Alloy Smart Lock Panel with Rose-Gold PVD

ZincSmart Locks & Door HardwareDie castingFinishingCosmetic

A 300 mm panel that warped after casting, under a PVD film too thin to hide sink marks. Cored bosses, zoned cooling and per-load colour checks give 0.15 mm flatness and ΔE ≤ 1.0.

Zamak 3 / YZZnAl4A (GB/T 13818-2024) · 约 420 g
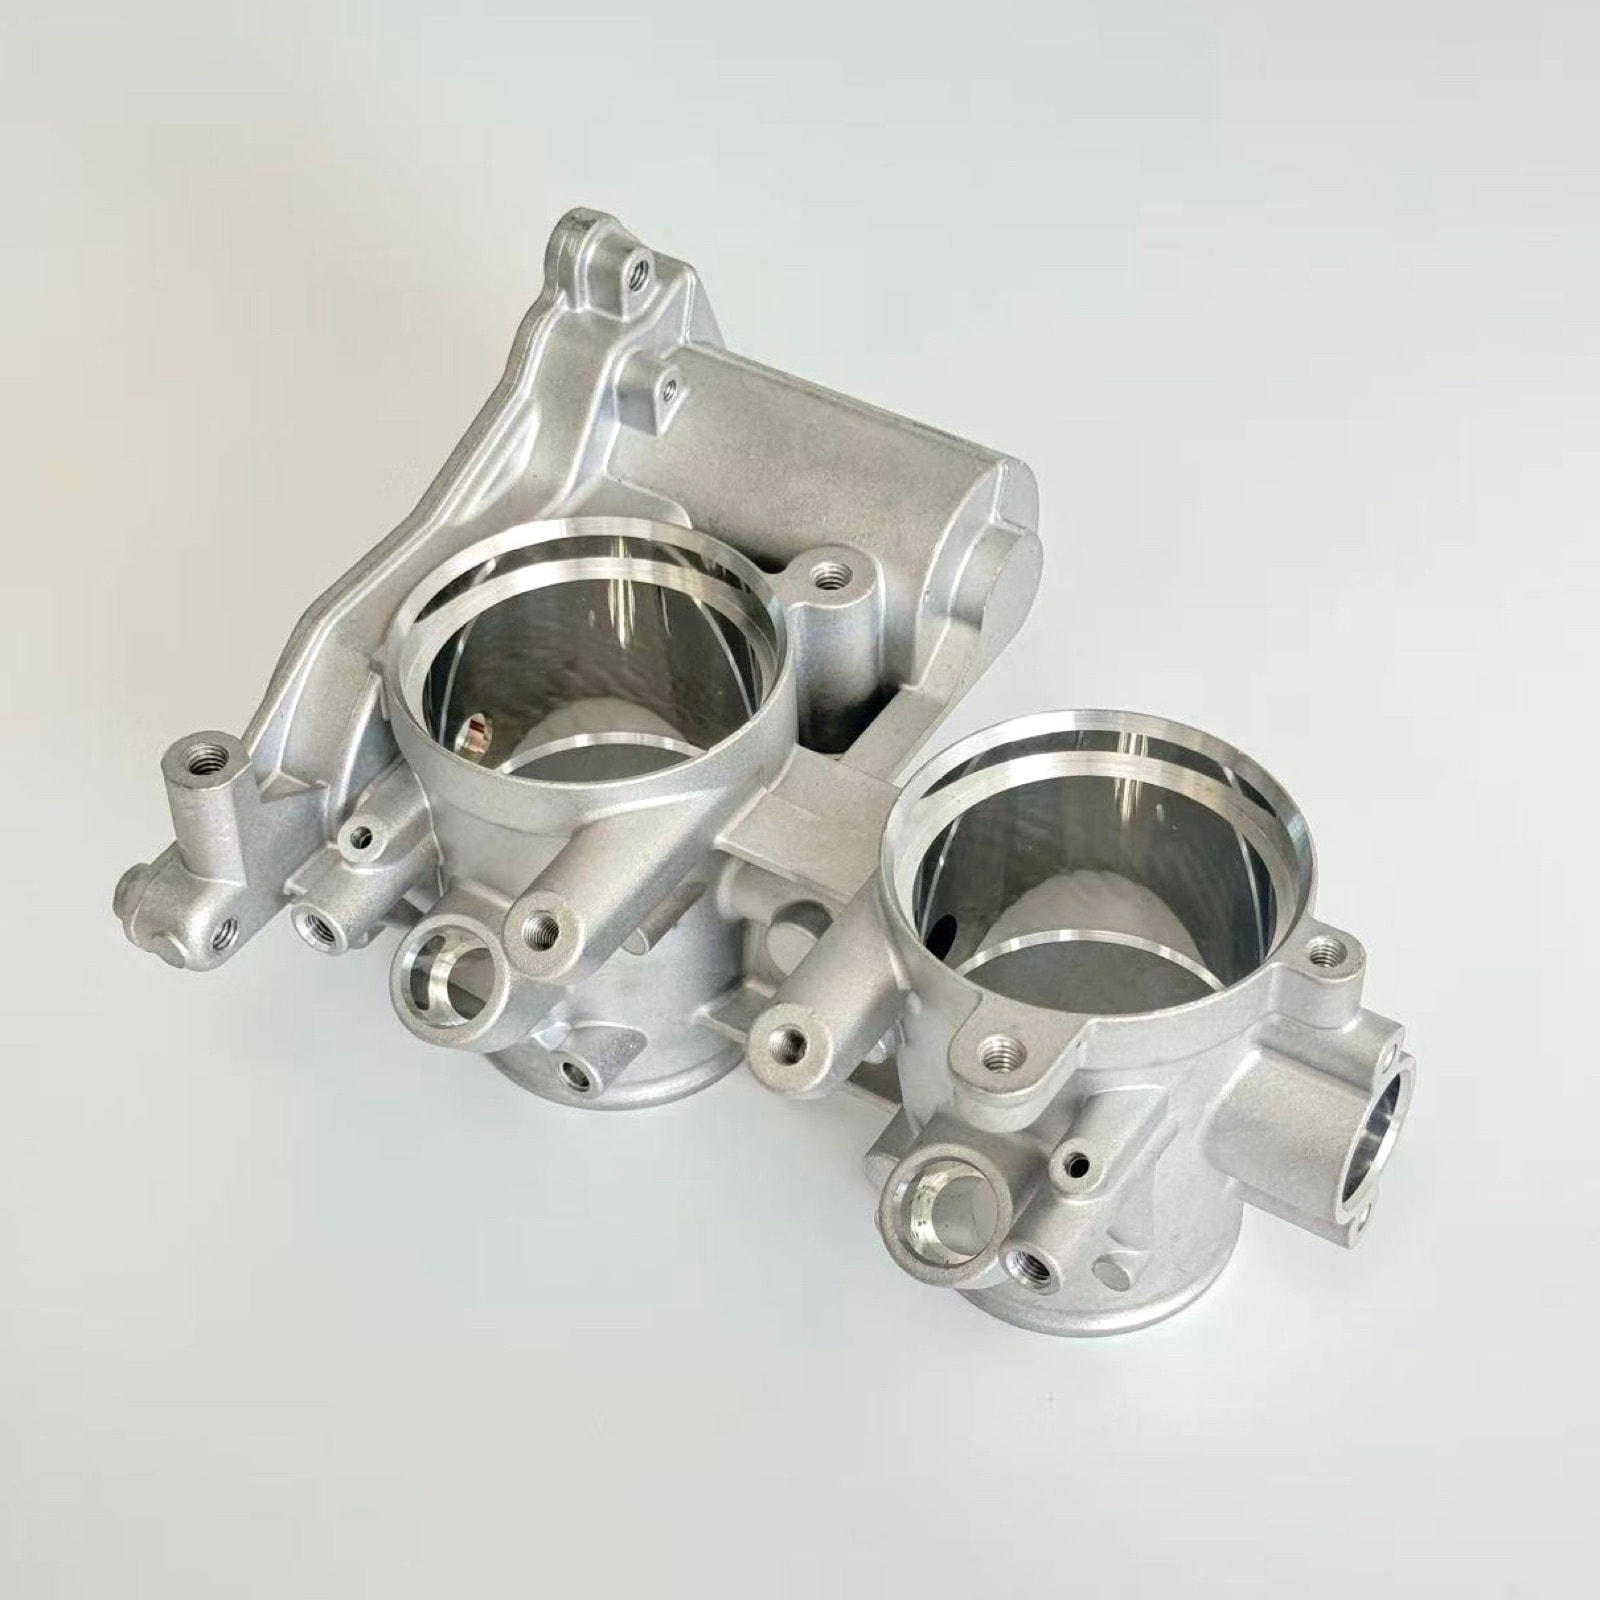
Motorcycle Twin Throttle Body

Motorcycle Twin Throttle Body

AluminumMotorcycle & Two-WheelerDie castingCNC machiningPressure tightPrecision

Machined in two setups, the twin bores differed by up to 0.05 mm and the engine idled rough. One-setup boring and soft jaws now match them within 0.02 mm.

ADC12 (JIS H5302) · 约 520 g
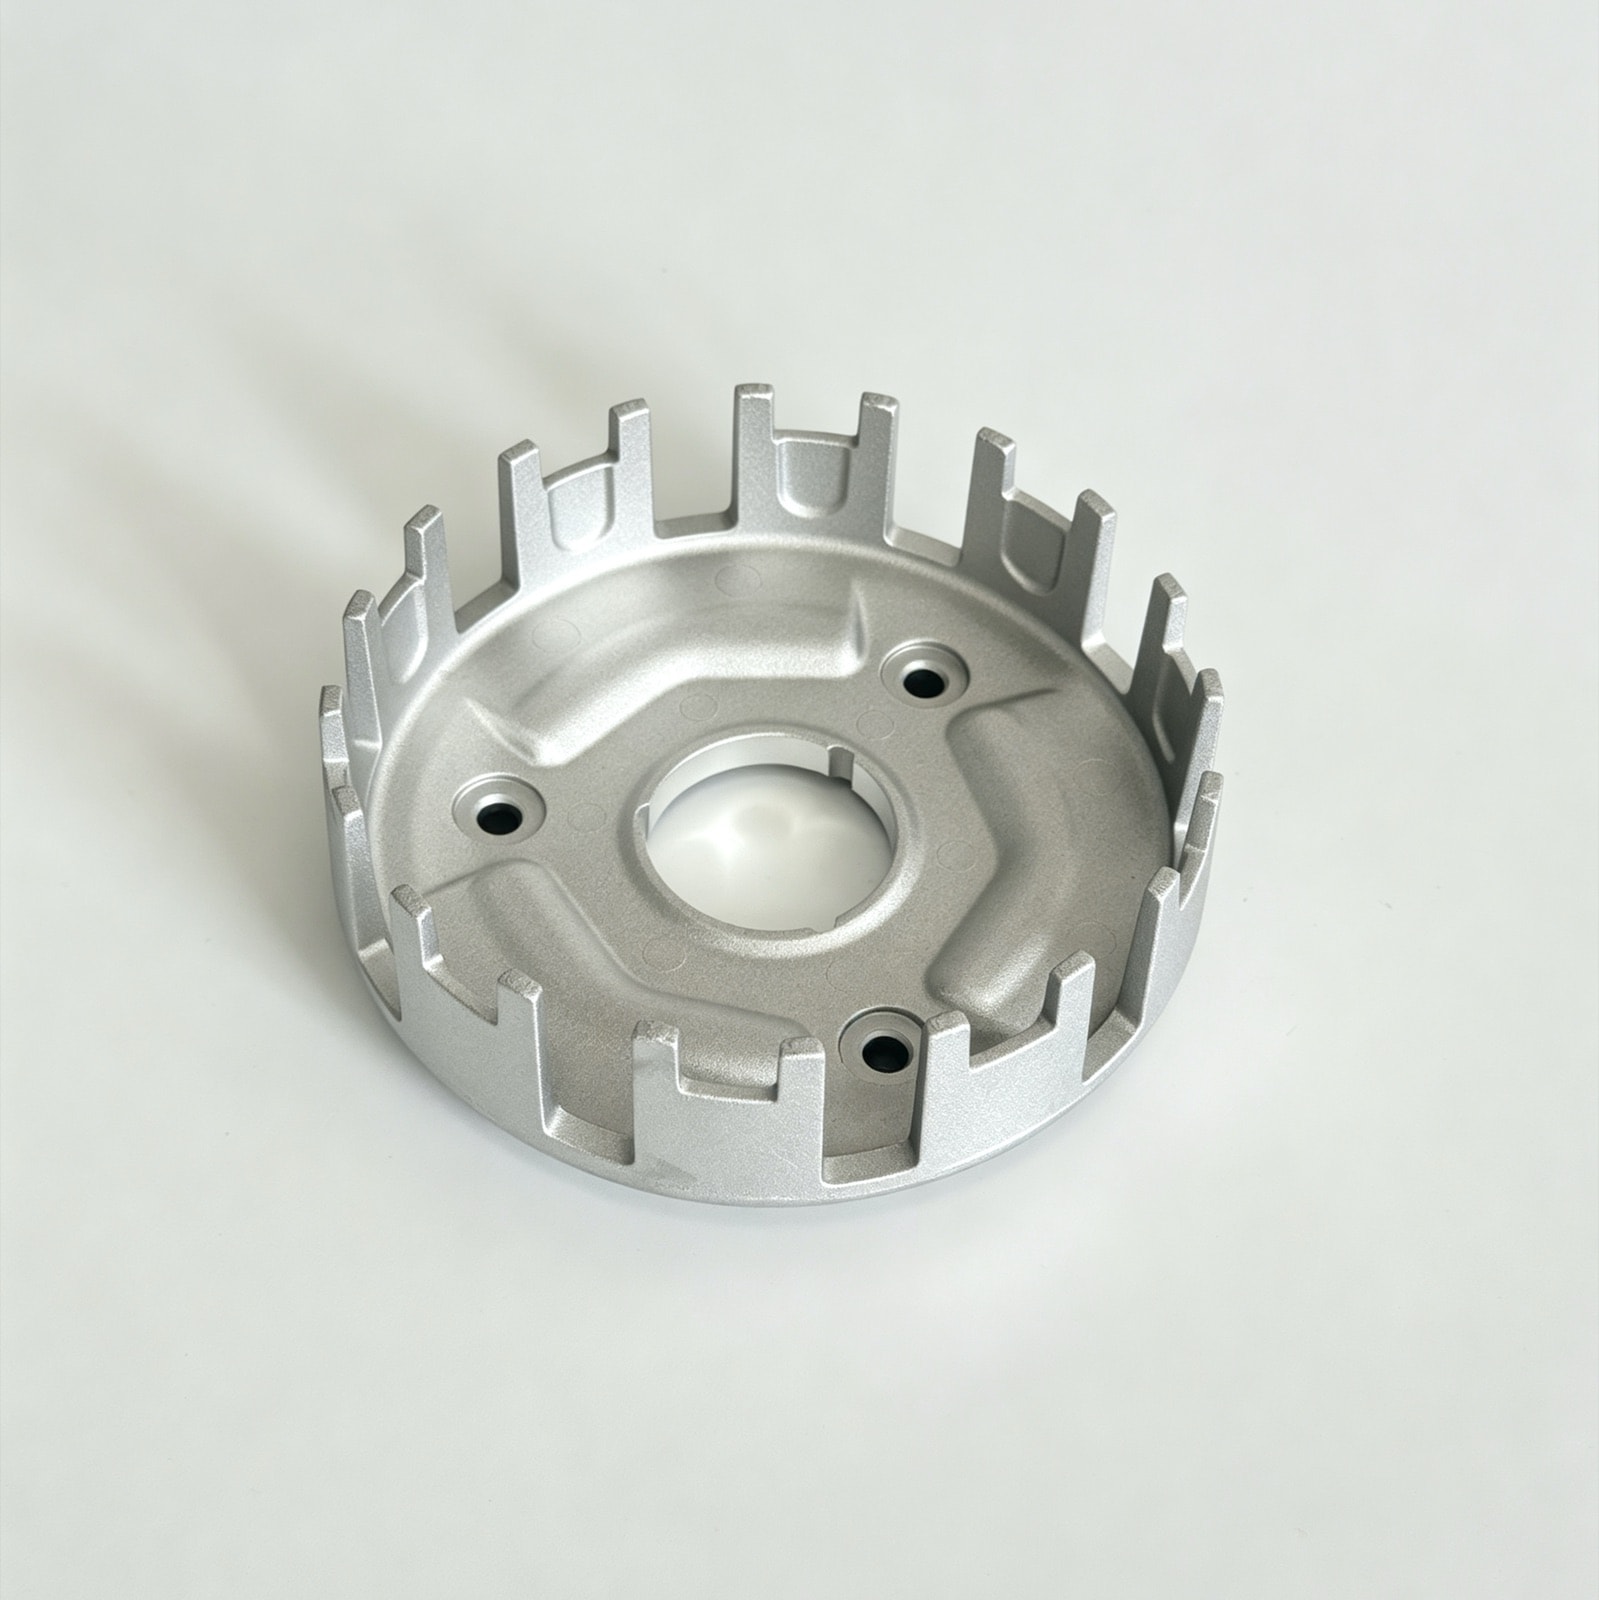
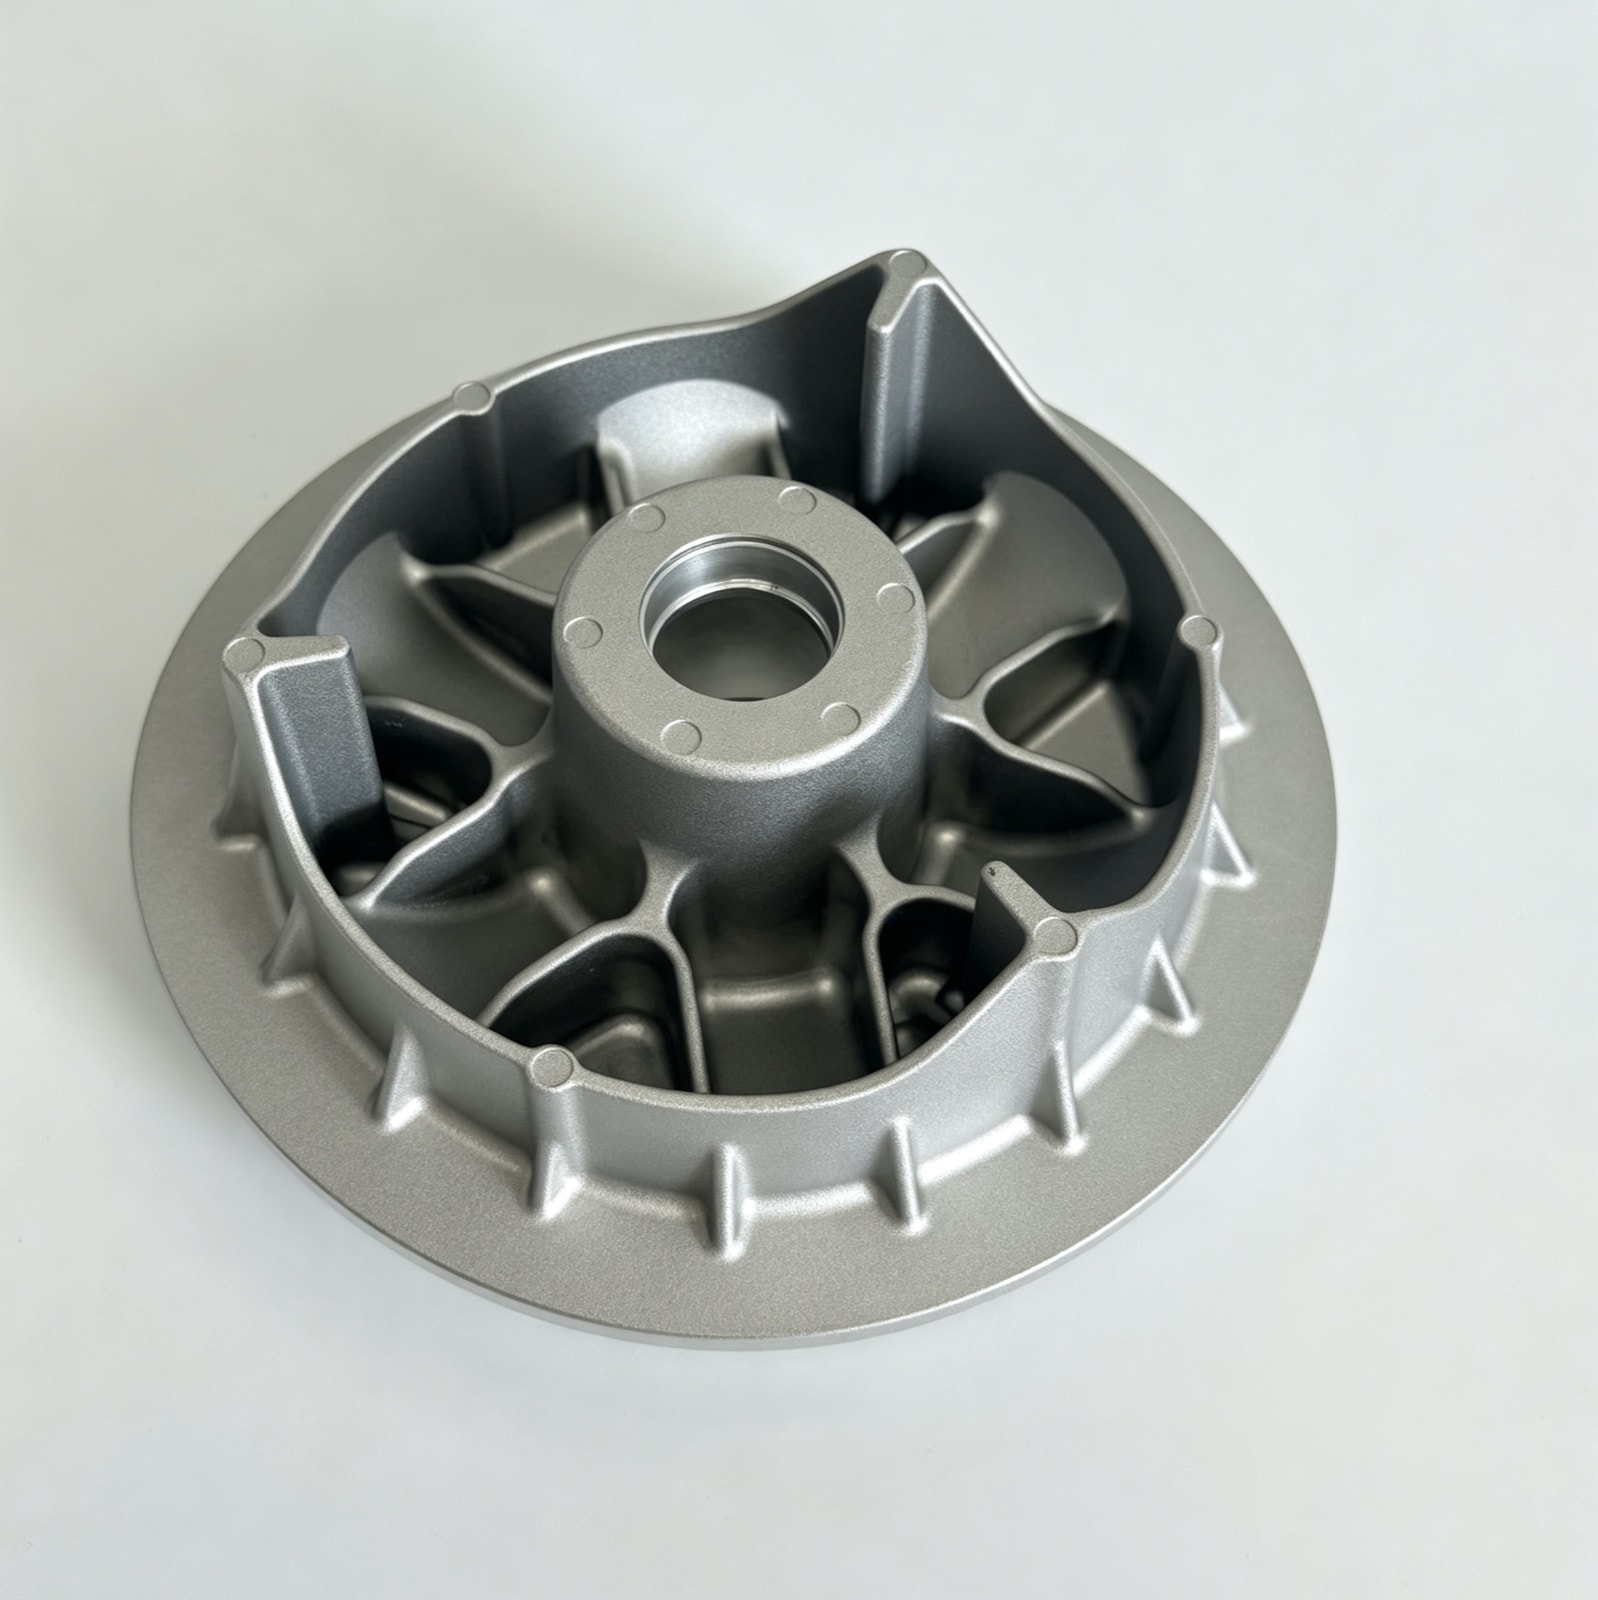
Motorcycle Clutch Basket

Motorcycle Clutch Basket

AluminumMotorcycle & Two-WheelerDie castingCNC machiningFinishingPrecision

Slot widths once varied by 0.08 mm between batches and the friction plates bound. Core cooling, scheduled core changes and 100% gauging now hold ±0.05 mm.

ADC12 (JIS H5302) · 约 330 g
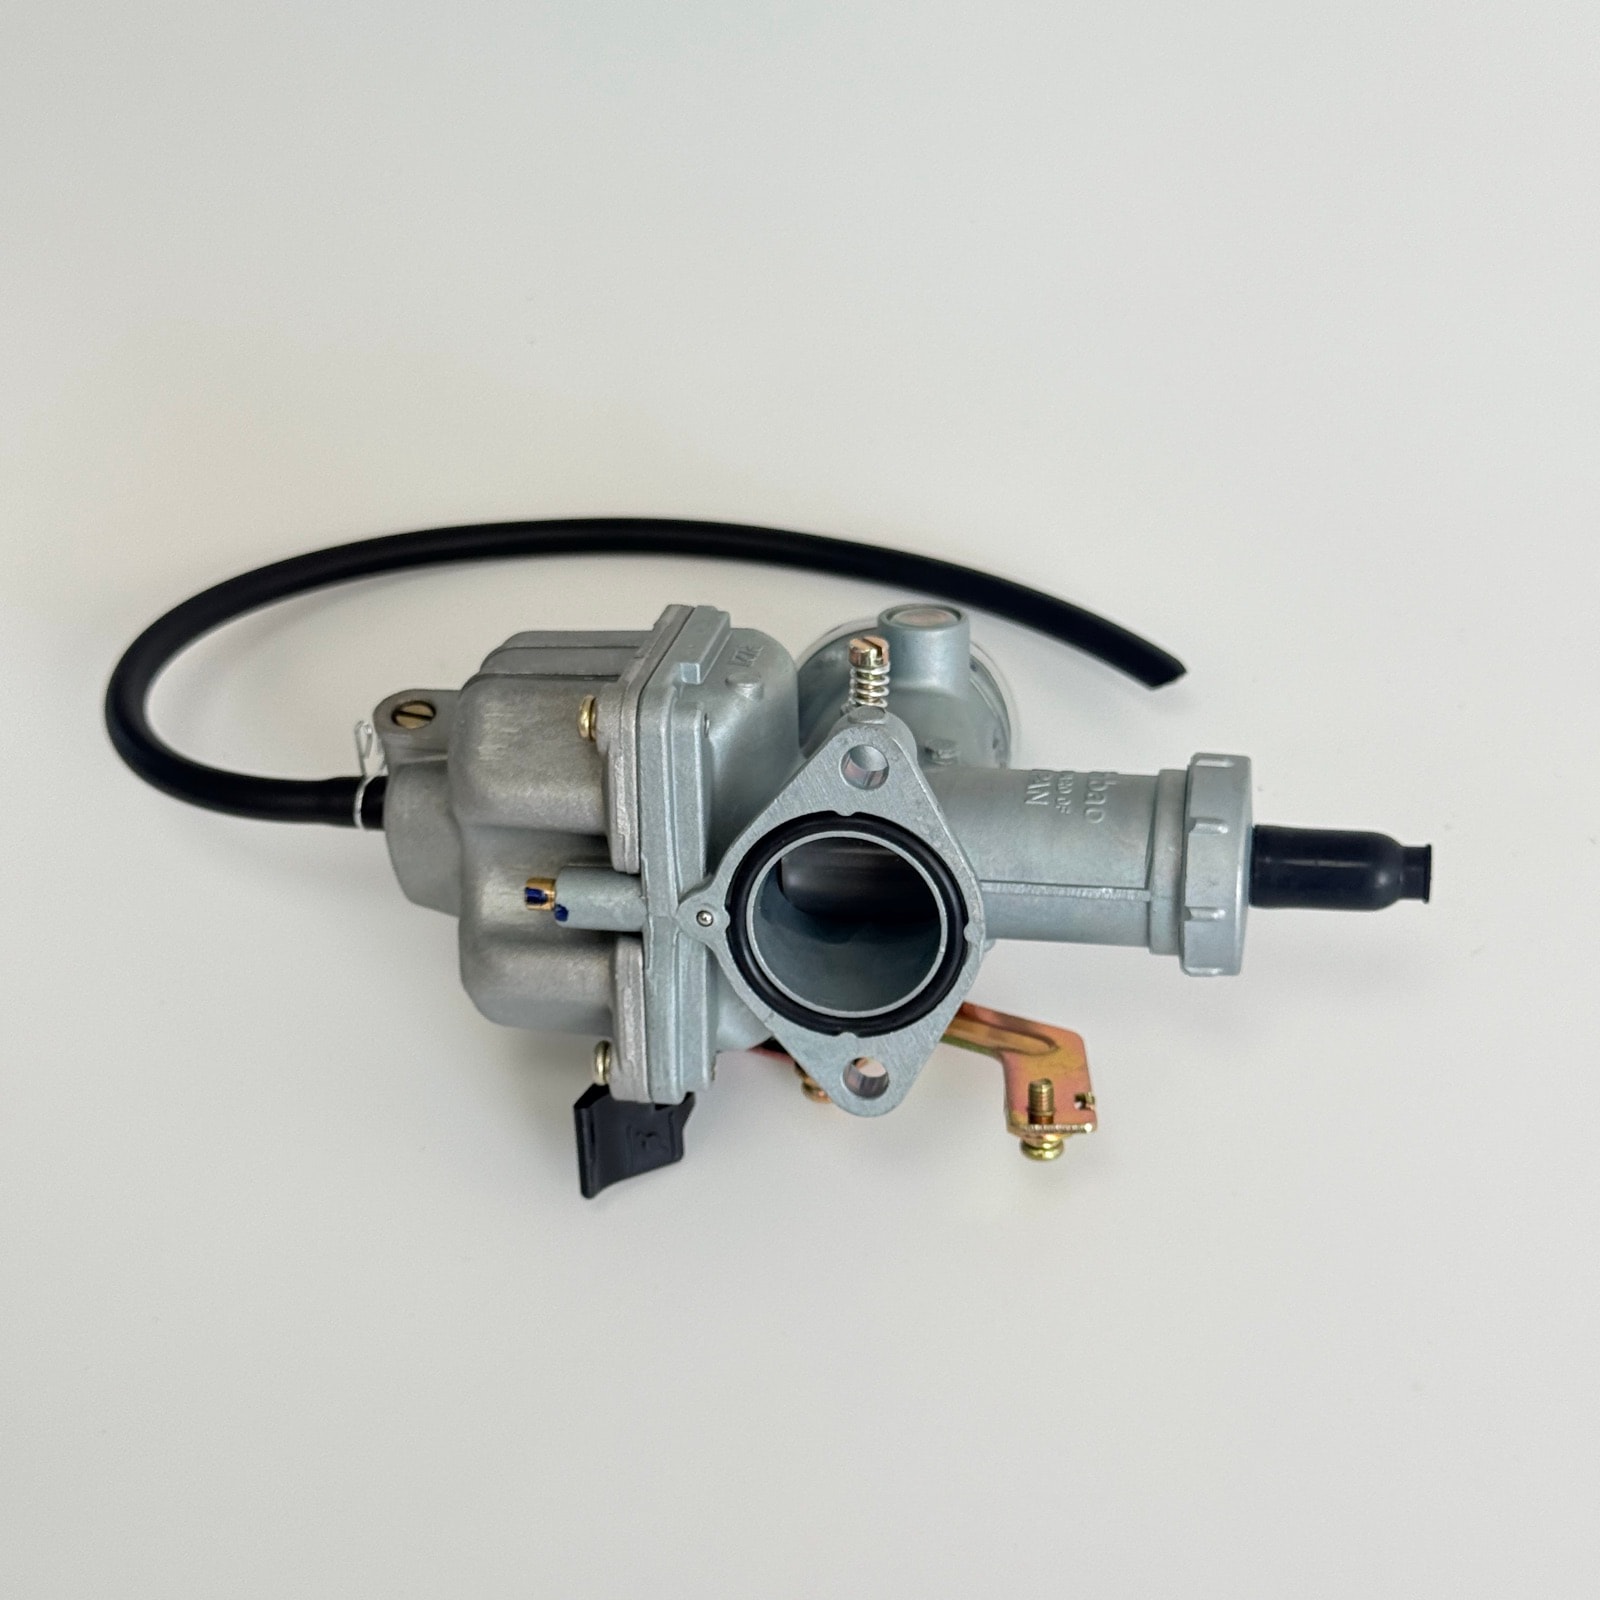
PZ27 Motorcycle Carburetor Assembly

PZ27 Motorcycle Carburetor Assembly

AluminumMotorcycle & Two-WheelerDie castingCNC machiningAssemblyPressure tightPrecision

A 0.1 mm jet shift moves idle flow by over 5%. One-datum machining, flow-sorted jets and 100% bench testing hold ±2%, with over a million delivered.

ADC12 (JIS H5302) · 约 420 g(总成)
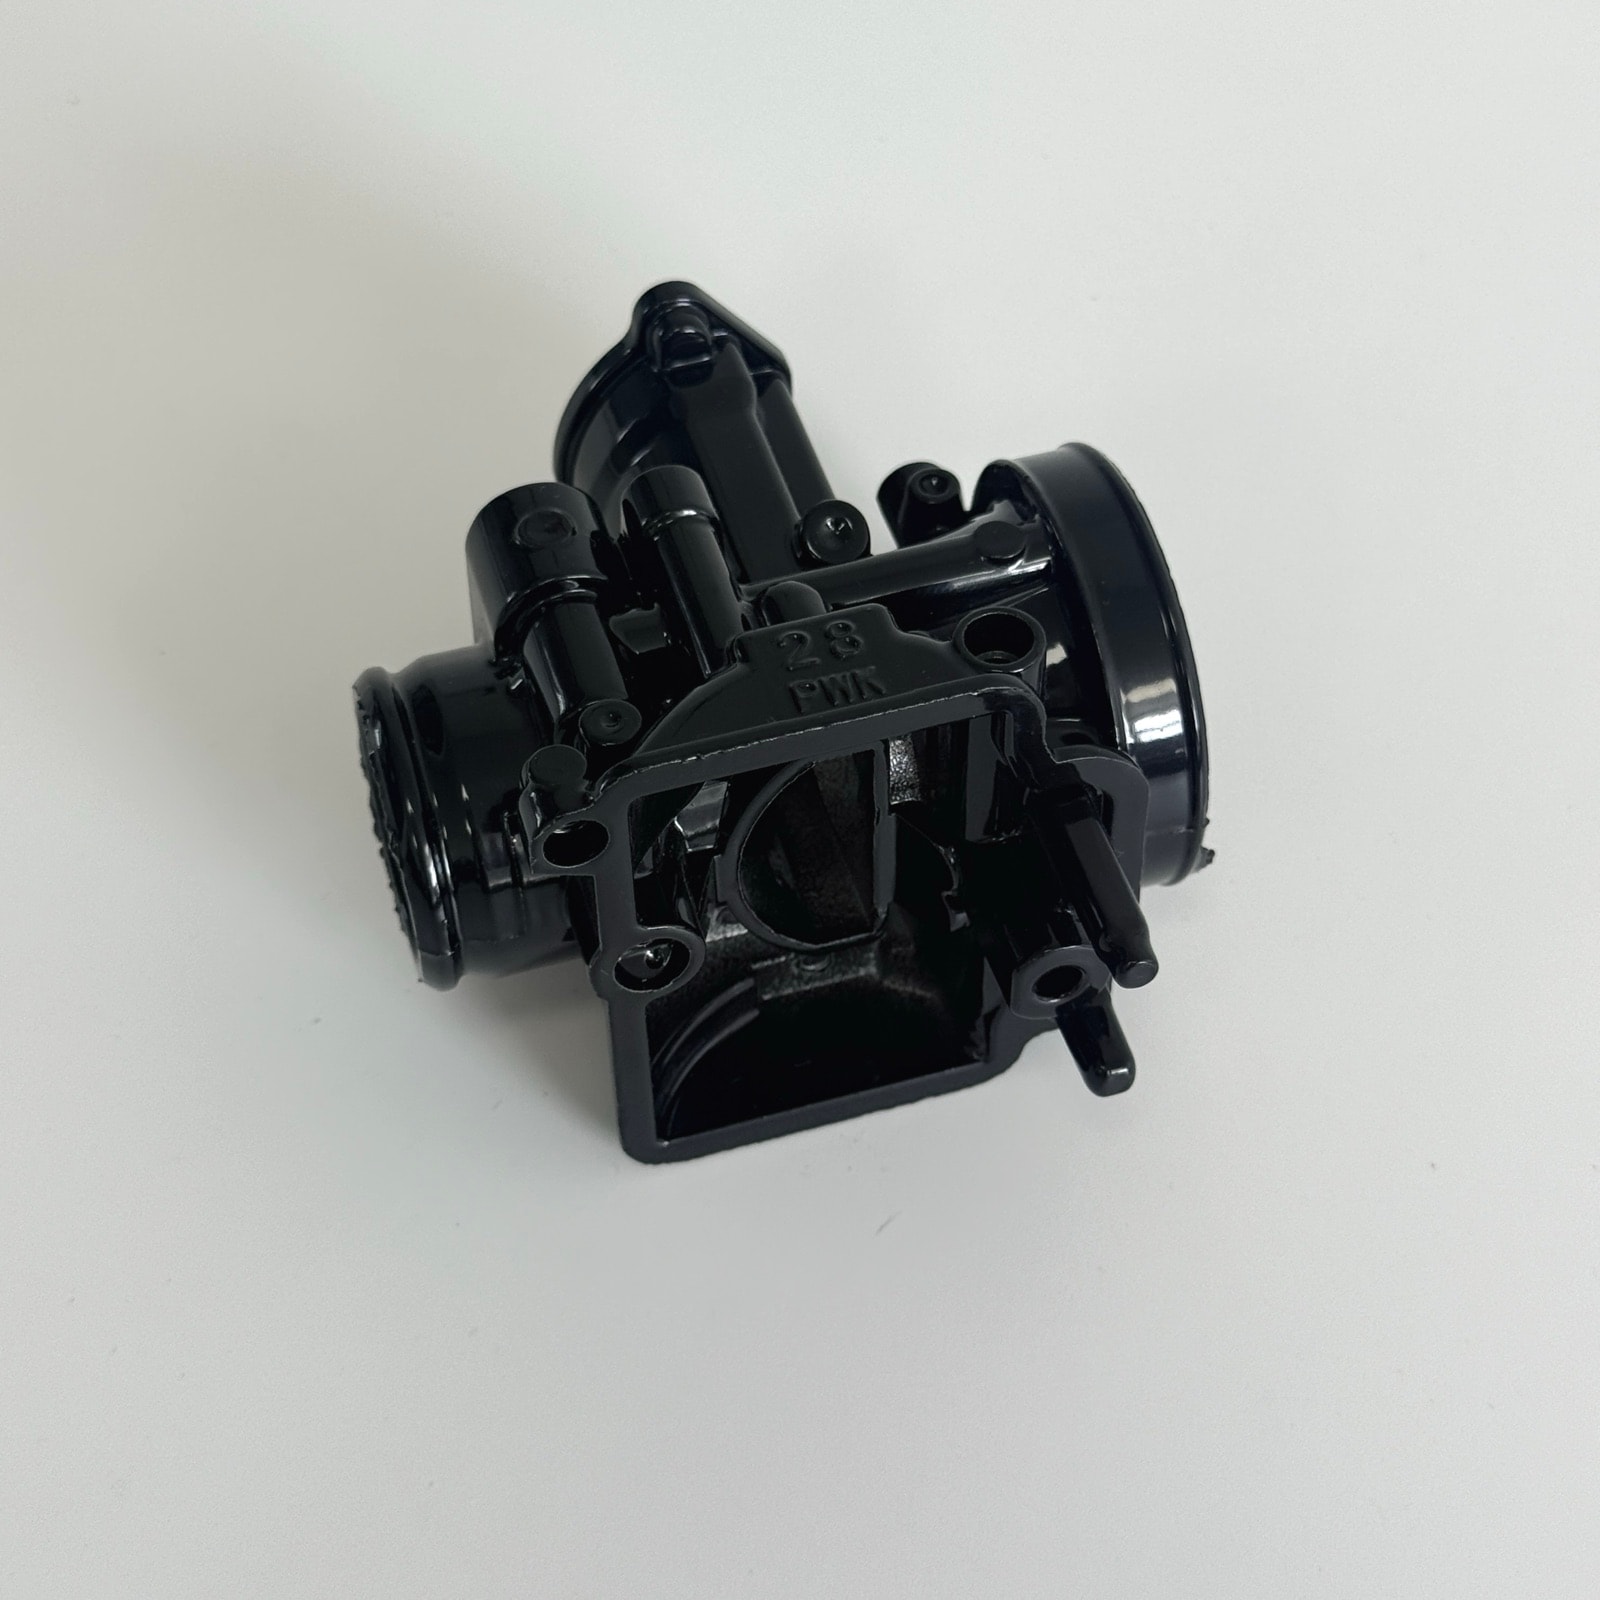
PWK28 Carburetor Body

PWK28 Carburetor Body

AluminumMotorcycle & Two-WheelerDie castingCNC machiningFinishingCosmeticPrecision

A gloss black coat magnifies every flow mark. Knit lines moved off the show faces, 100% pre-coat inspection and fixed blasting keep cosmetic rejects under 1%.

ADC12 (JIS H5302) · 约 300 g
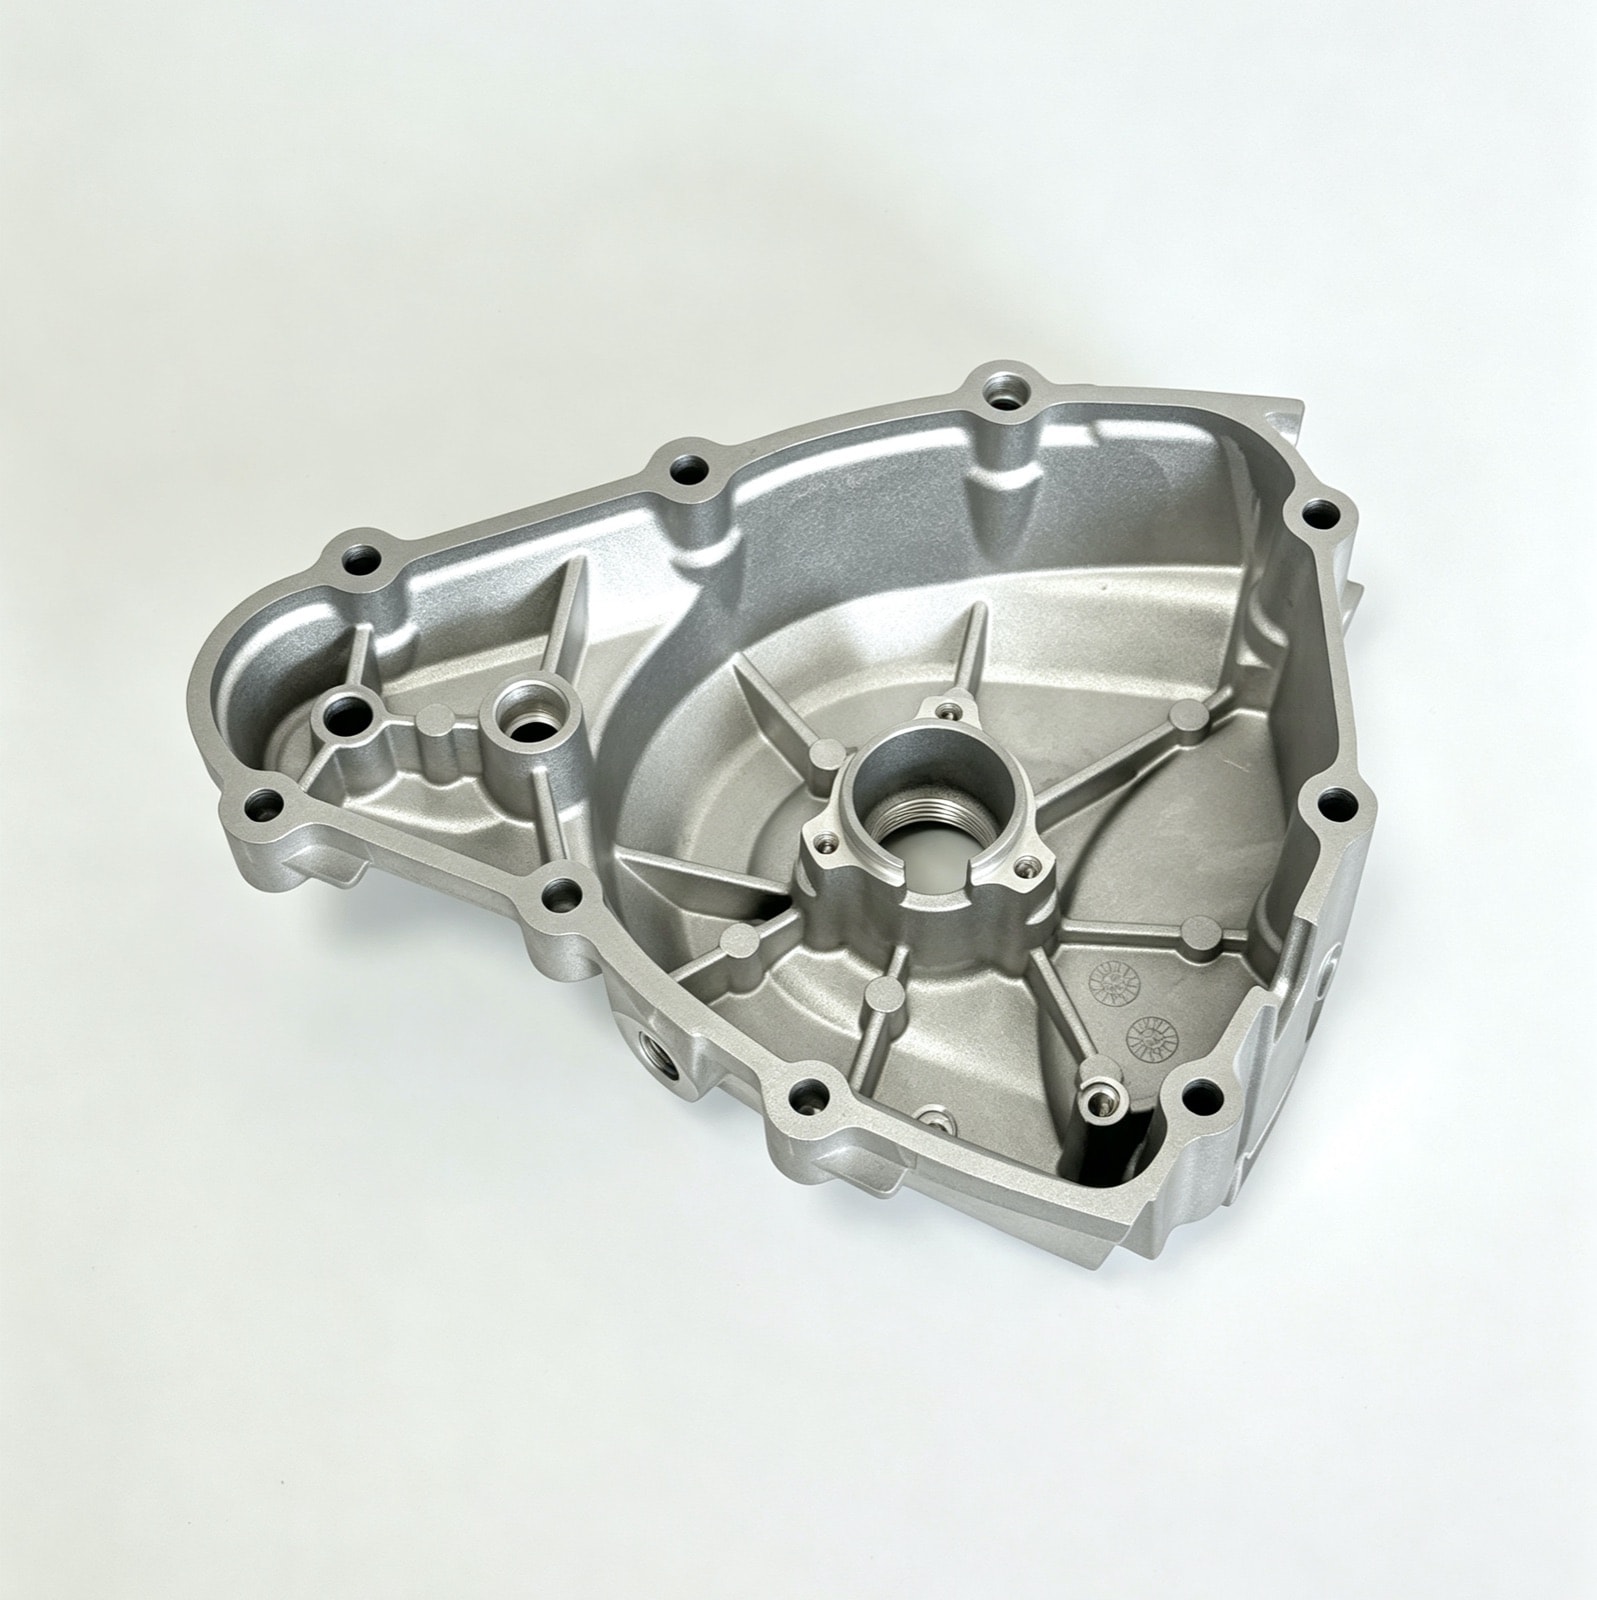
Motorcycle Crankcase Side Cover

Motorcycle Crankcase Side Cover

AluminumMotorcycle & Two-WheelerDie castingCNC machiningFinishingPressure tightPrecision

The 230 mm cover came off the die 0.15 mm out of flat. Even ejection, stress relief and gentle fixturing now hold 0.08 mm; oil-weep complaints are under 0.1%.

ADC12 (JIS H5302) · 约 780 g
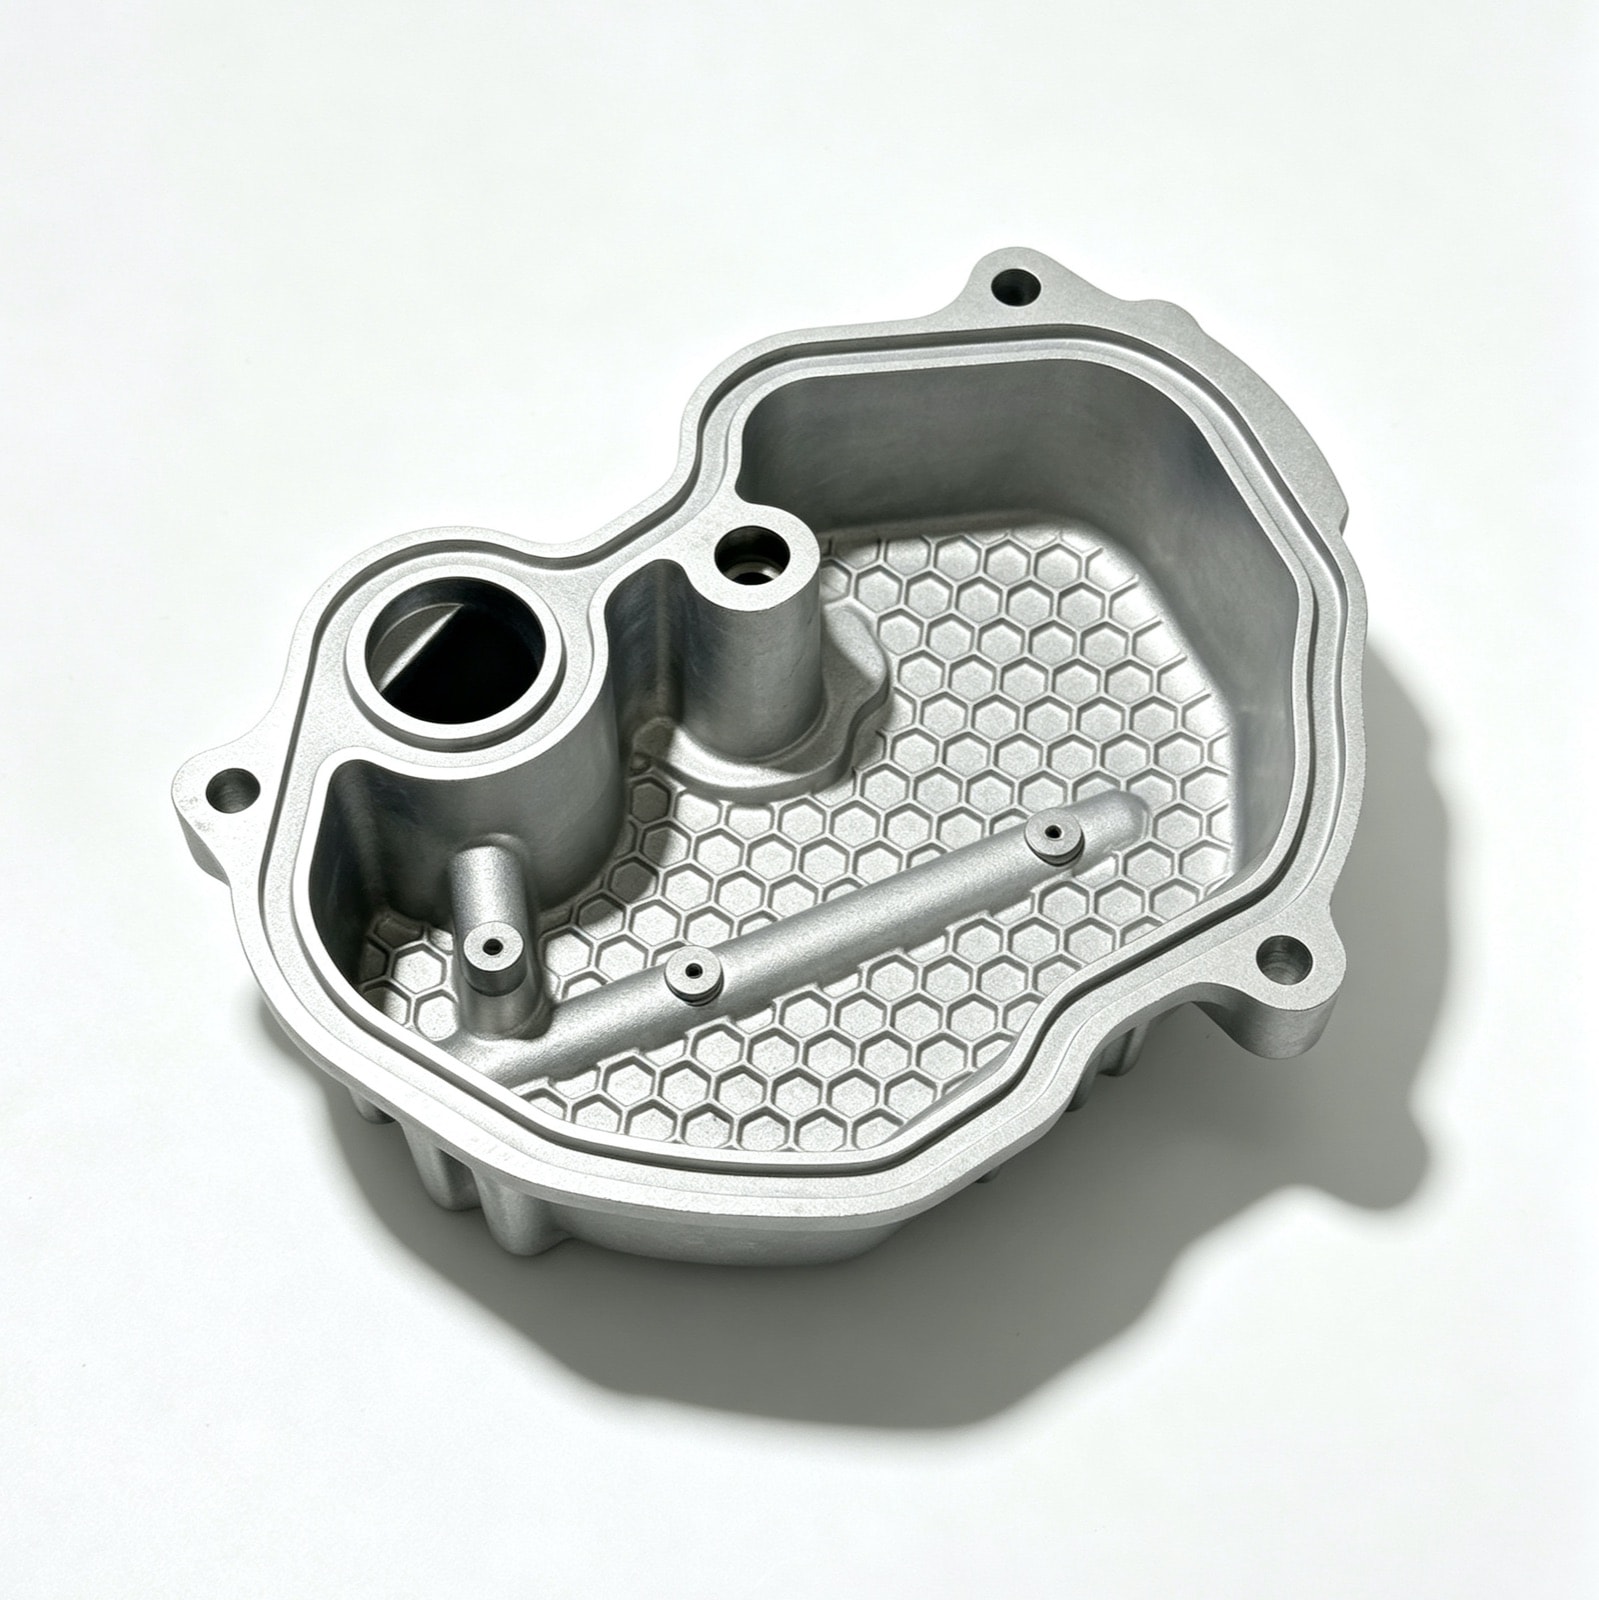
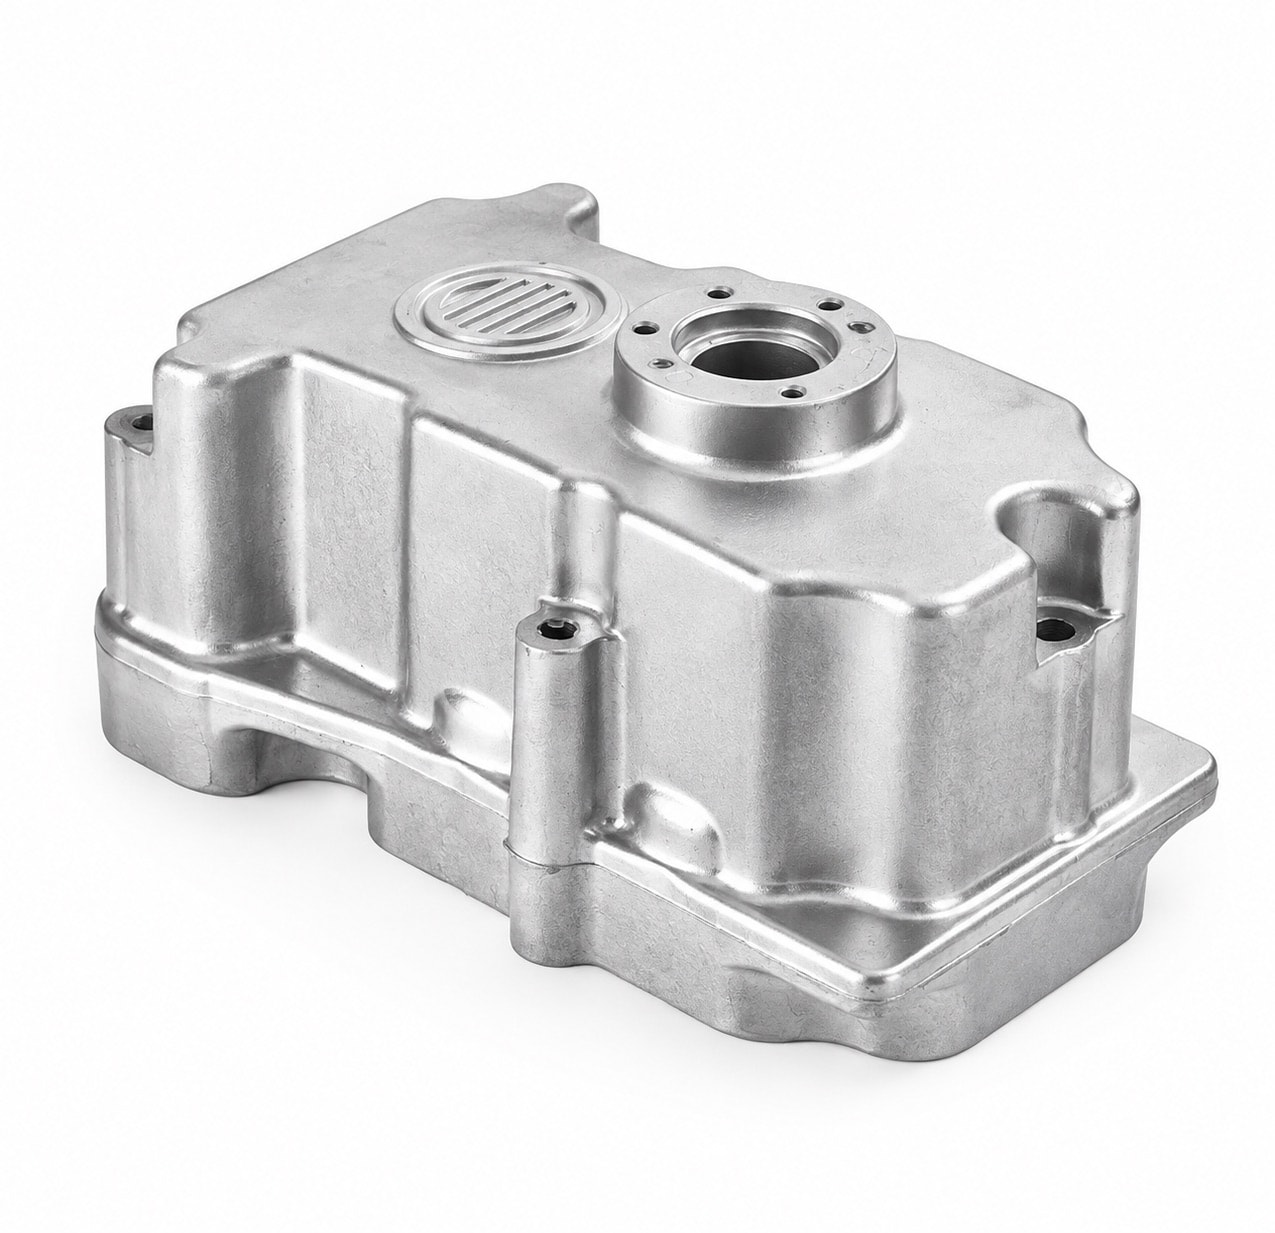
Motorcycle Cylinder Head Cover

Motorcycle Cylinder Head Cover

AluminumMotorcycle & Two-WheelerDie castingCNC machiningPressure tightPrecision

Where honeycomb ribs meet, the metal freezes last and shrinks. Ribs near 0.6× wall, thinned intersections and added venting now pass X-ray at over 99%.

ADC12 (JIS H5302) · 约 460 g
Motorcycle Clutch Pressure Plate

Motorcycle Clutch Pressure Plate

AluminumMotorcycle & Two-WheelerDie castingCNC machiningFinishingThermalPrecision

2 mm fins short-filled at the tips and warped the face. Hotter fin cavities, tip vents and flow-length control now fill over 99%, with runout within 0.05 mm.

ADC12 (JIS H5302) · 约 260 g
Motorcycle Intake Manifold Adapter

Motorcycle Intake Manifold Adapter

AluminumMotorcycle & Two-WheelerDie castingCNC machiningFinishingPressure tight

Milled in two setups, the flanges ran 0.2 mm out of parallel and the gasket leaked. One-setup machining and 100% leak testing now hold 0.1 mm.

ADC12 (JIS H5302) · 约 150 g
Motorcycle Engine Valve Cover

Motorcycle Engine Valve Cover

AluminumMotorcycle & Two-WheelerDie castingCNC machiningFinishingPressure tightCosmetic

A 6 mm land and a porous breather root caused sporadic leaks. A larger root radius, an overflow and single-pass milling now give 99% first-pass leak yield.

ADC12 (JIS H5302) · 约 130 g
Small Engine Carburetor Body

Small Engine Carburetor Body

AluminumGeneral Power & Garden MachineryDie castingCNC machiningPressure tightPrecision

Drilled galleries opened casting porosity where they crossed, and plugs caused new leaks. Layout changes and 100% re-testing after plugging now pass over 98%.

ADC12 (JIS H5302) · 约 170 g
Diaphragm Carburetor Pump Cover

Diaphragm Carburetor Pump Cover

AluminumGeneral Power & Garden MachineryDie castingCNC machiningPrecision

Far cavities cold-shut and hand deburring bent the 2 mm cover. Balanced runners and fixtured, pressure-controlled brushing now hold 0.03 mm flatness.

ADC12 (JIS H5302) · 约 45 g
Engine Water Pump Cover

Engine Water Pump Cover

AluminumPumps, Valves & Fluid ComponentsDie castingCNC machiningFinishingPressure tight

Shrinkage at the outlet-spigot root caused leaks. A graded root radius, local squeeze and leak testing before coating now give 99% first-pass yield.

ADC12 (JIS H5302) · 约 210 g
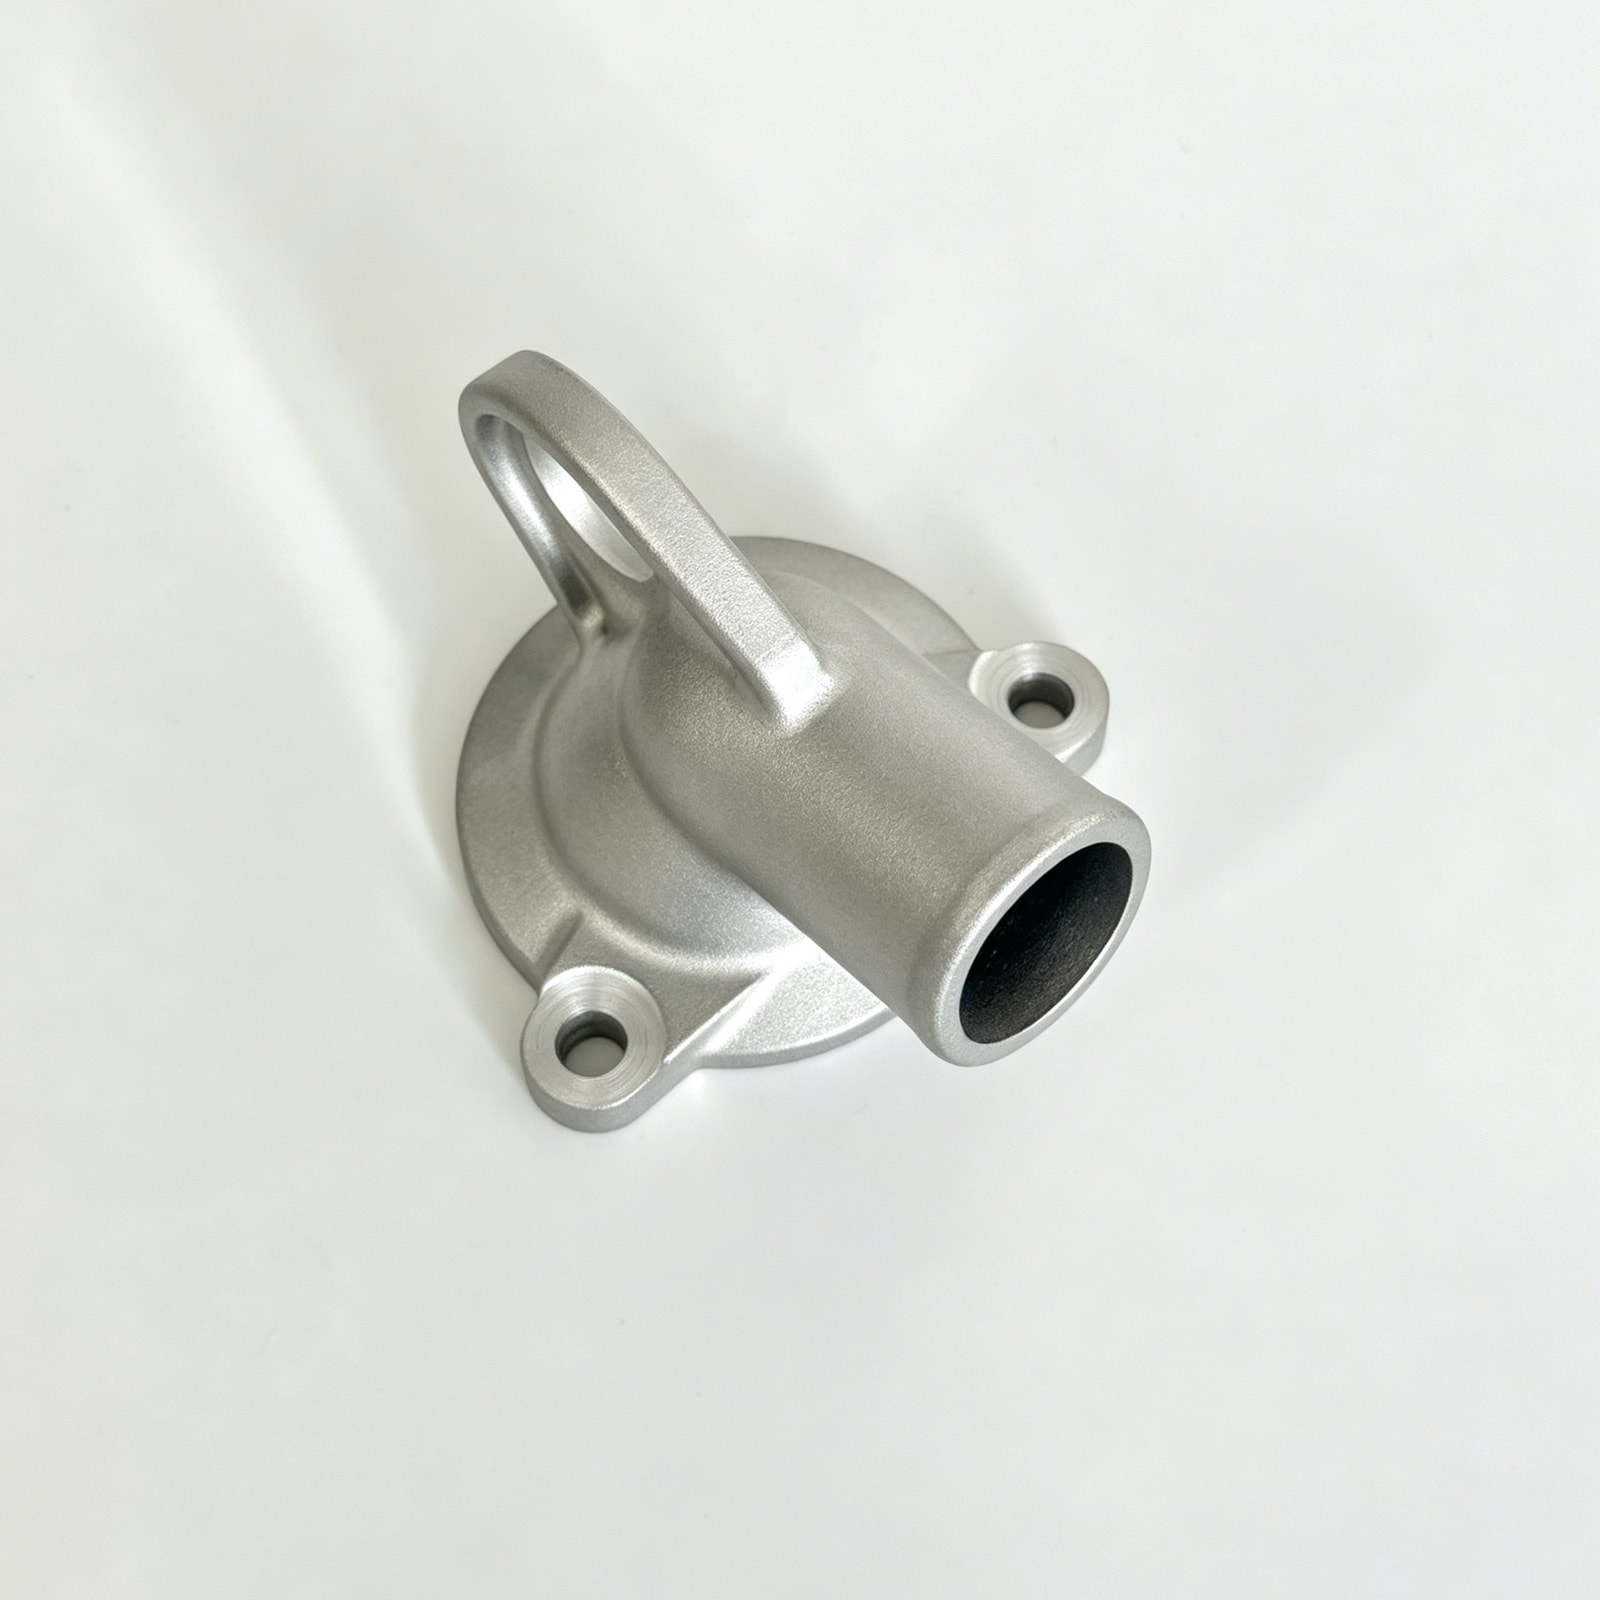
Engine Thermostat Housing

Engine Thermostat Housing

AluminumPumps, Valves & Fluid ComponentsDie castingCNC machiningFinishingPressure tight

Thermal cycling moved the sealing face and coolant attacked porosity. Stress relief, impurity control and 100% leak testing keep field leaks under 0.1%.

ADC12 (JIS H5302) · 约 230 g
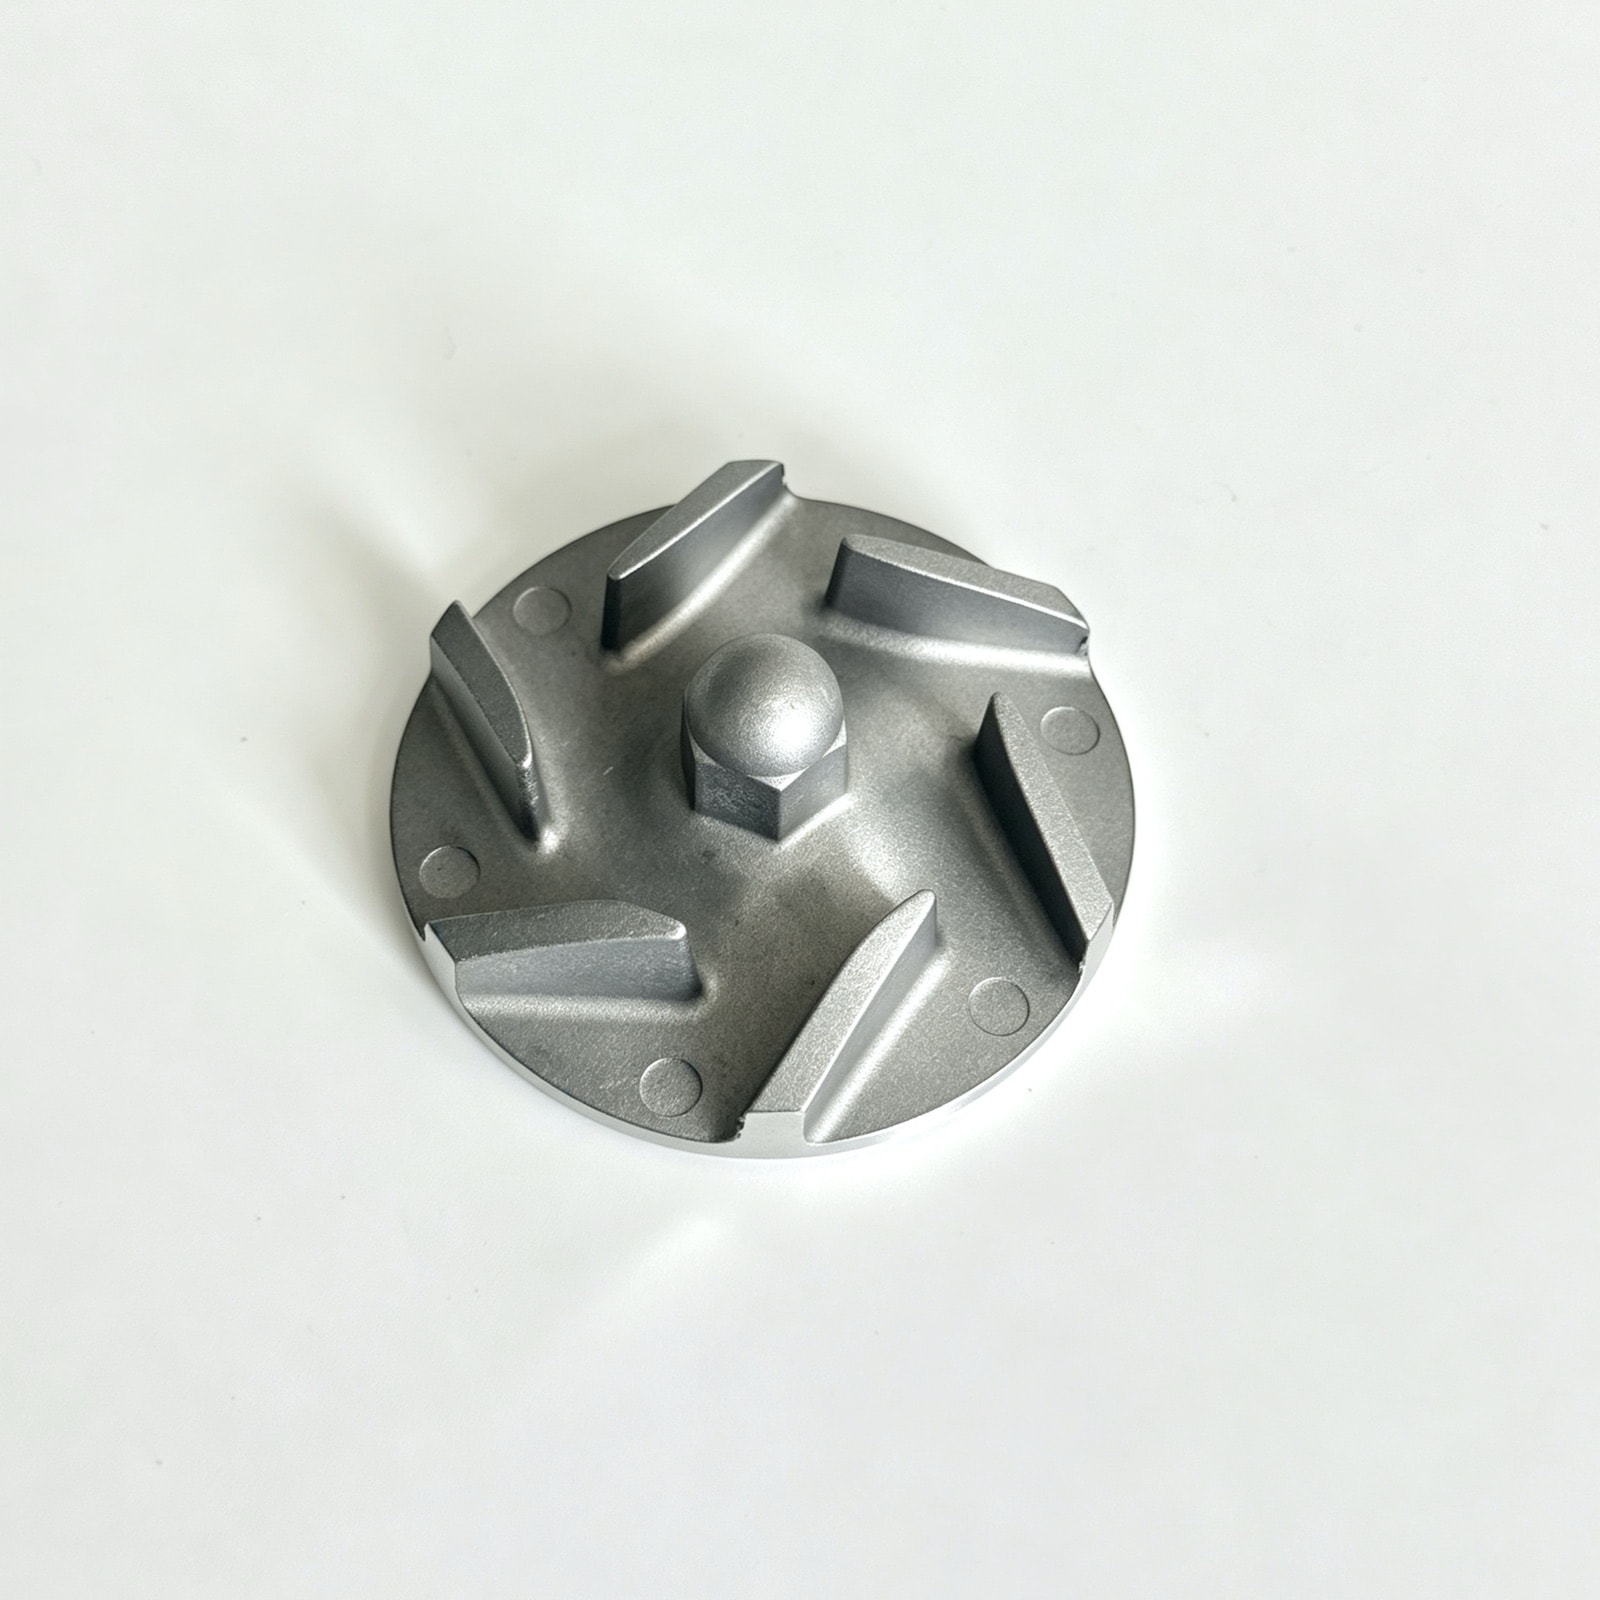
Engine Water Pump Impeller

Engine Water Pump Impeller

AluminumPumps, Valves & Fluid ComponentsDie castingCNC machiningPrecision

Core shift left one side of the impeller thick and the other thin. Double-guided cores and symmetric gates hold blades within 0.15 mm and imbalance to 1 g·mm.

ADC12 (JIS H5302) · 约 85 g
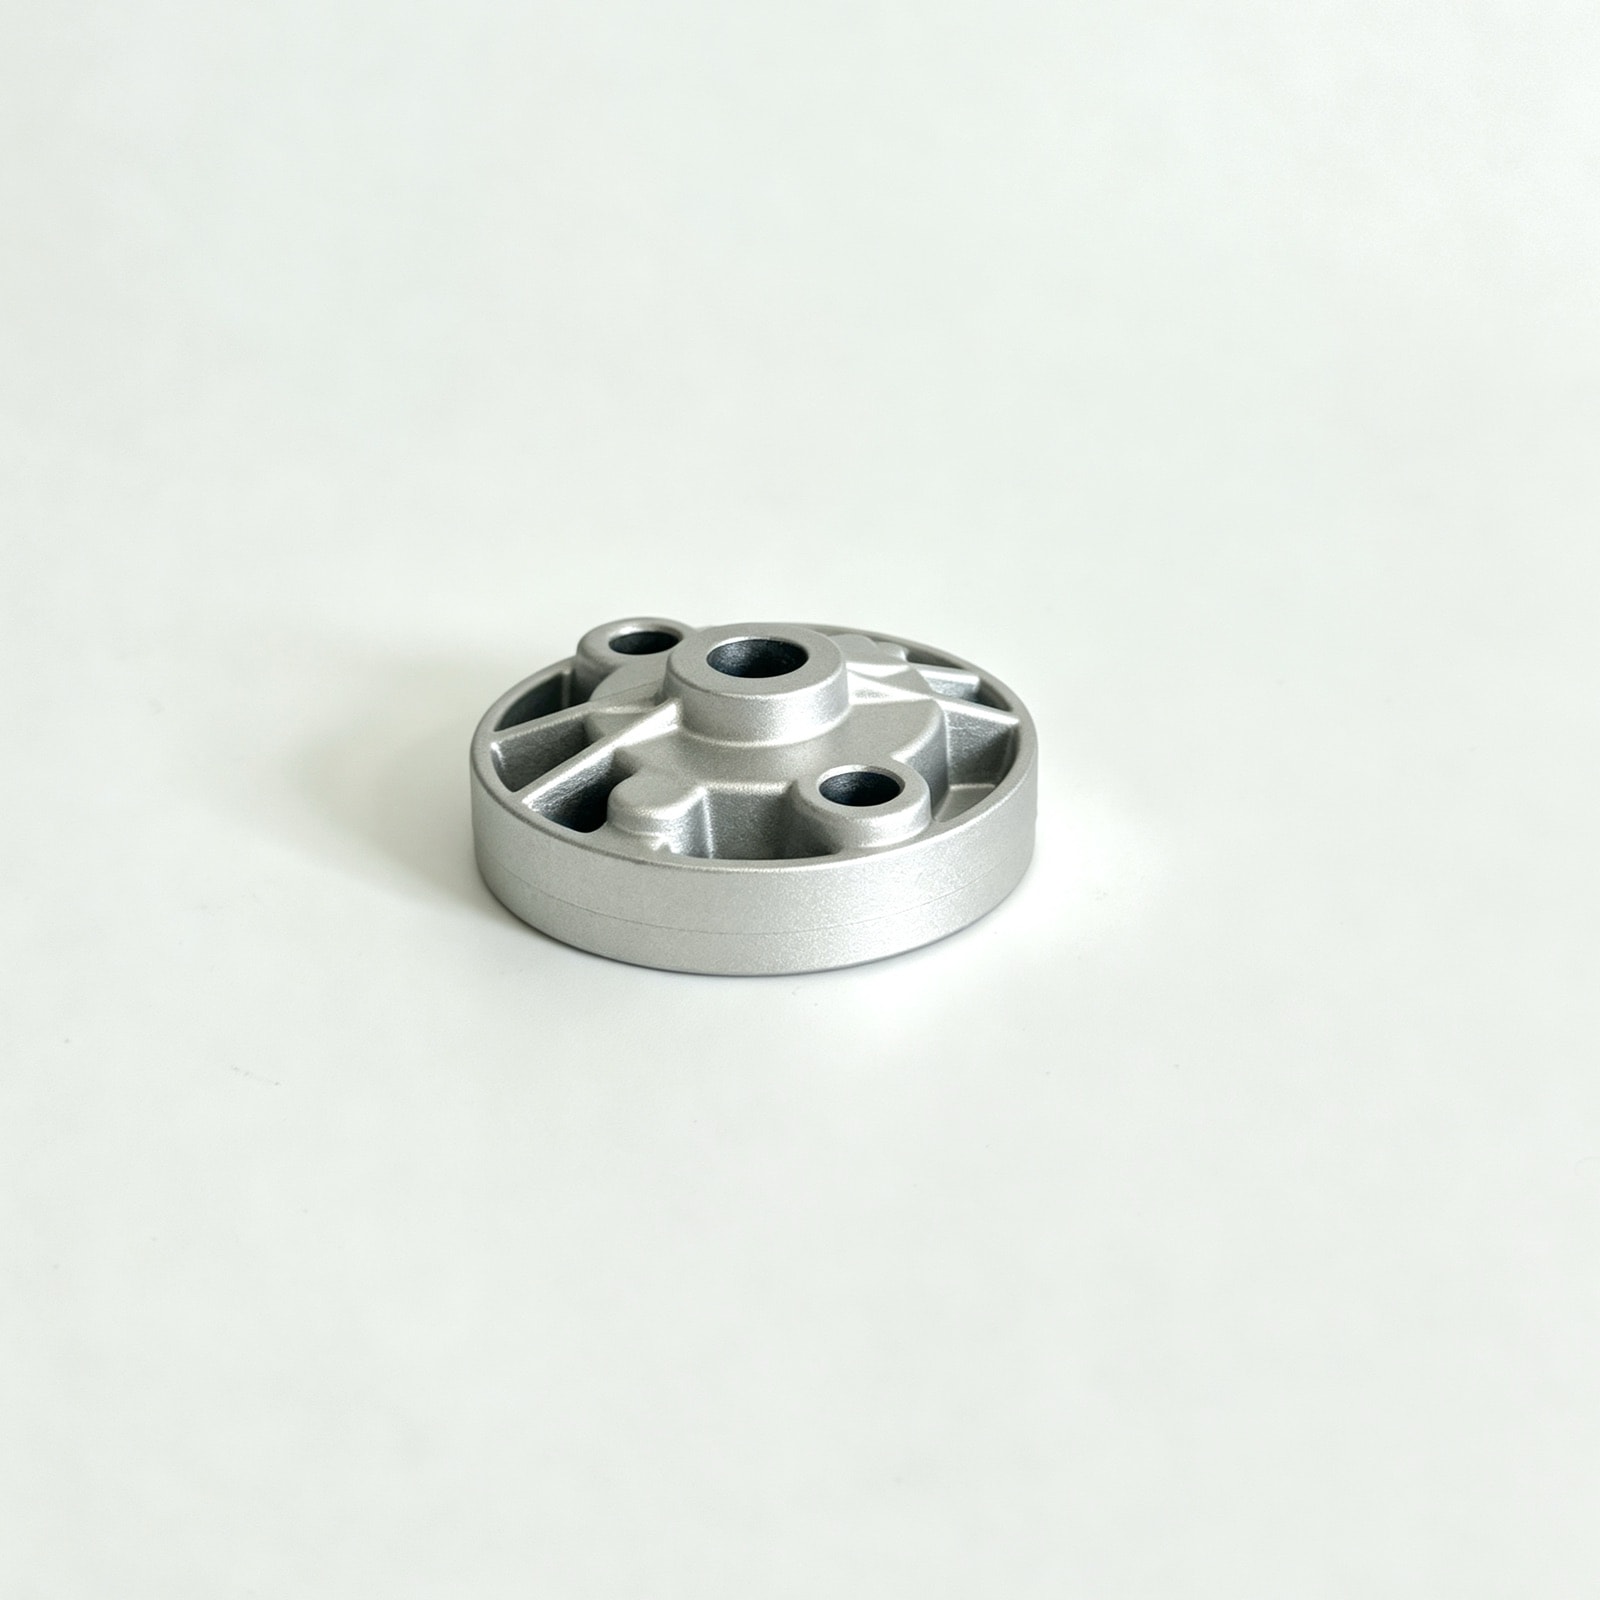
Engine Oil Pump End Cover

Engine Oil Pump End Cover

AluminumPumps, Valves & Fluid ComponentsDie castingCNC machiningFinishingPressure tightPrecision

A 0.05 mm thickness error drops pump pressure by over 10%. Ground faces, vacuum chucking and thickness banding hold ±0.02 mm; over 99% pass pump pressure.

ADC12 (JIS H5302) · 约 120 g
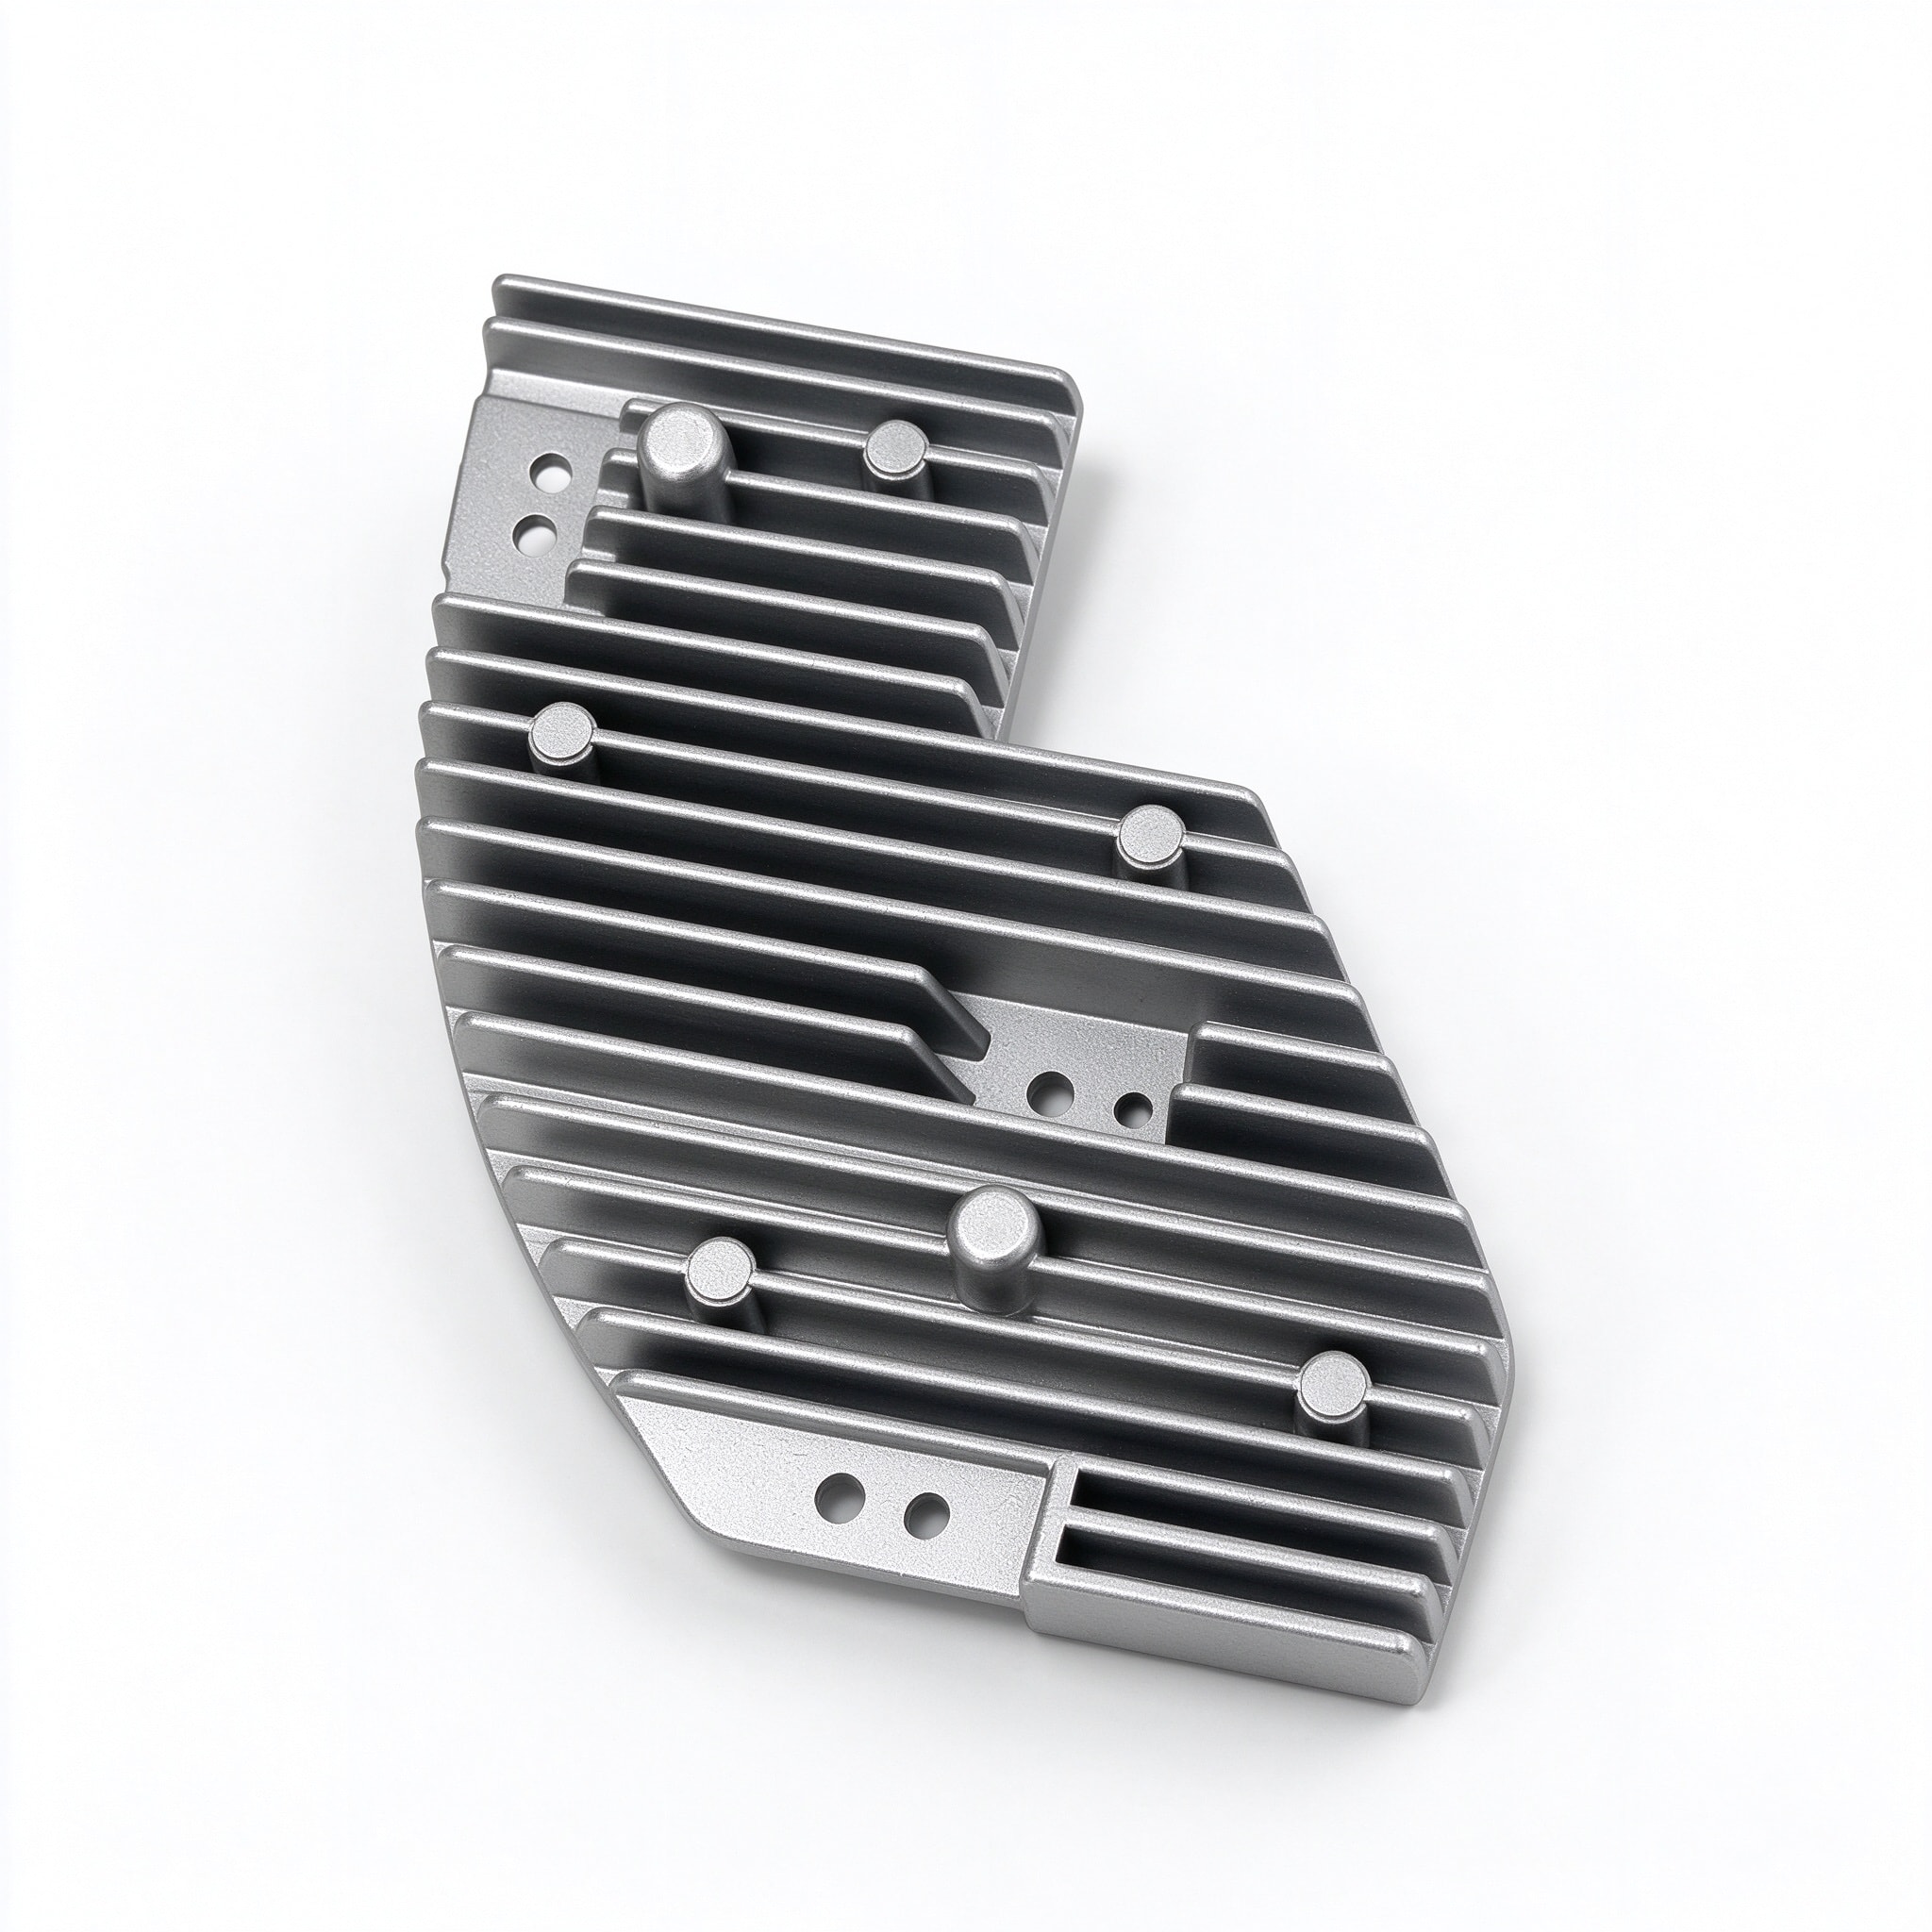
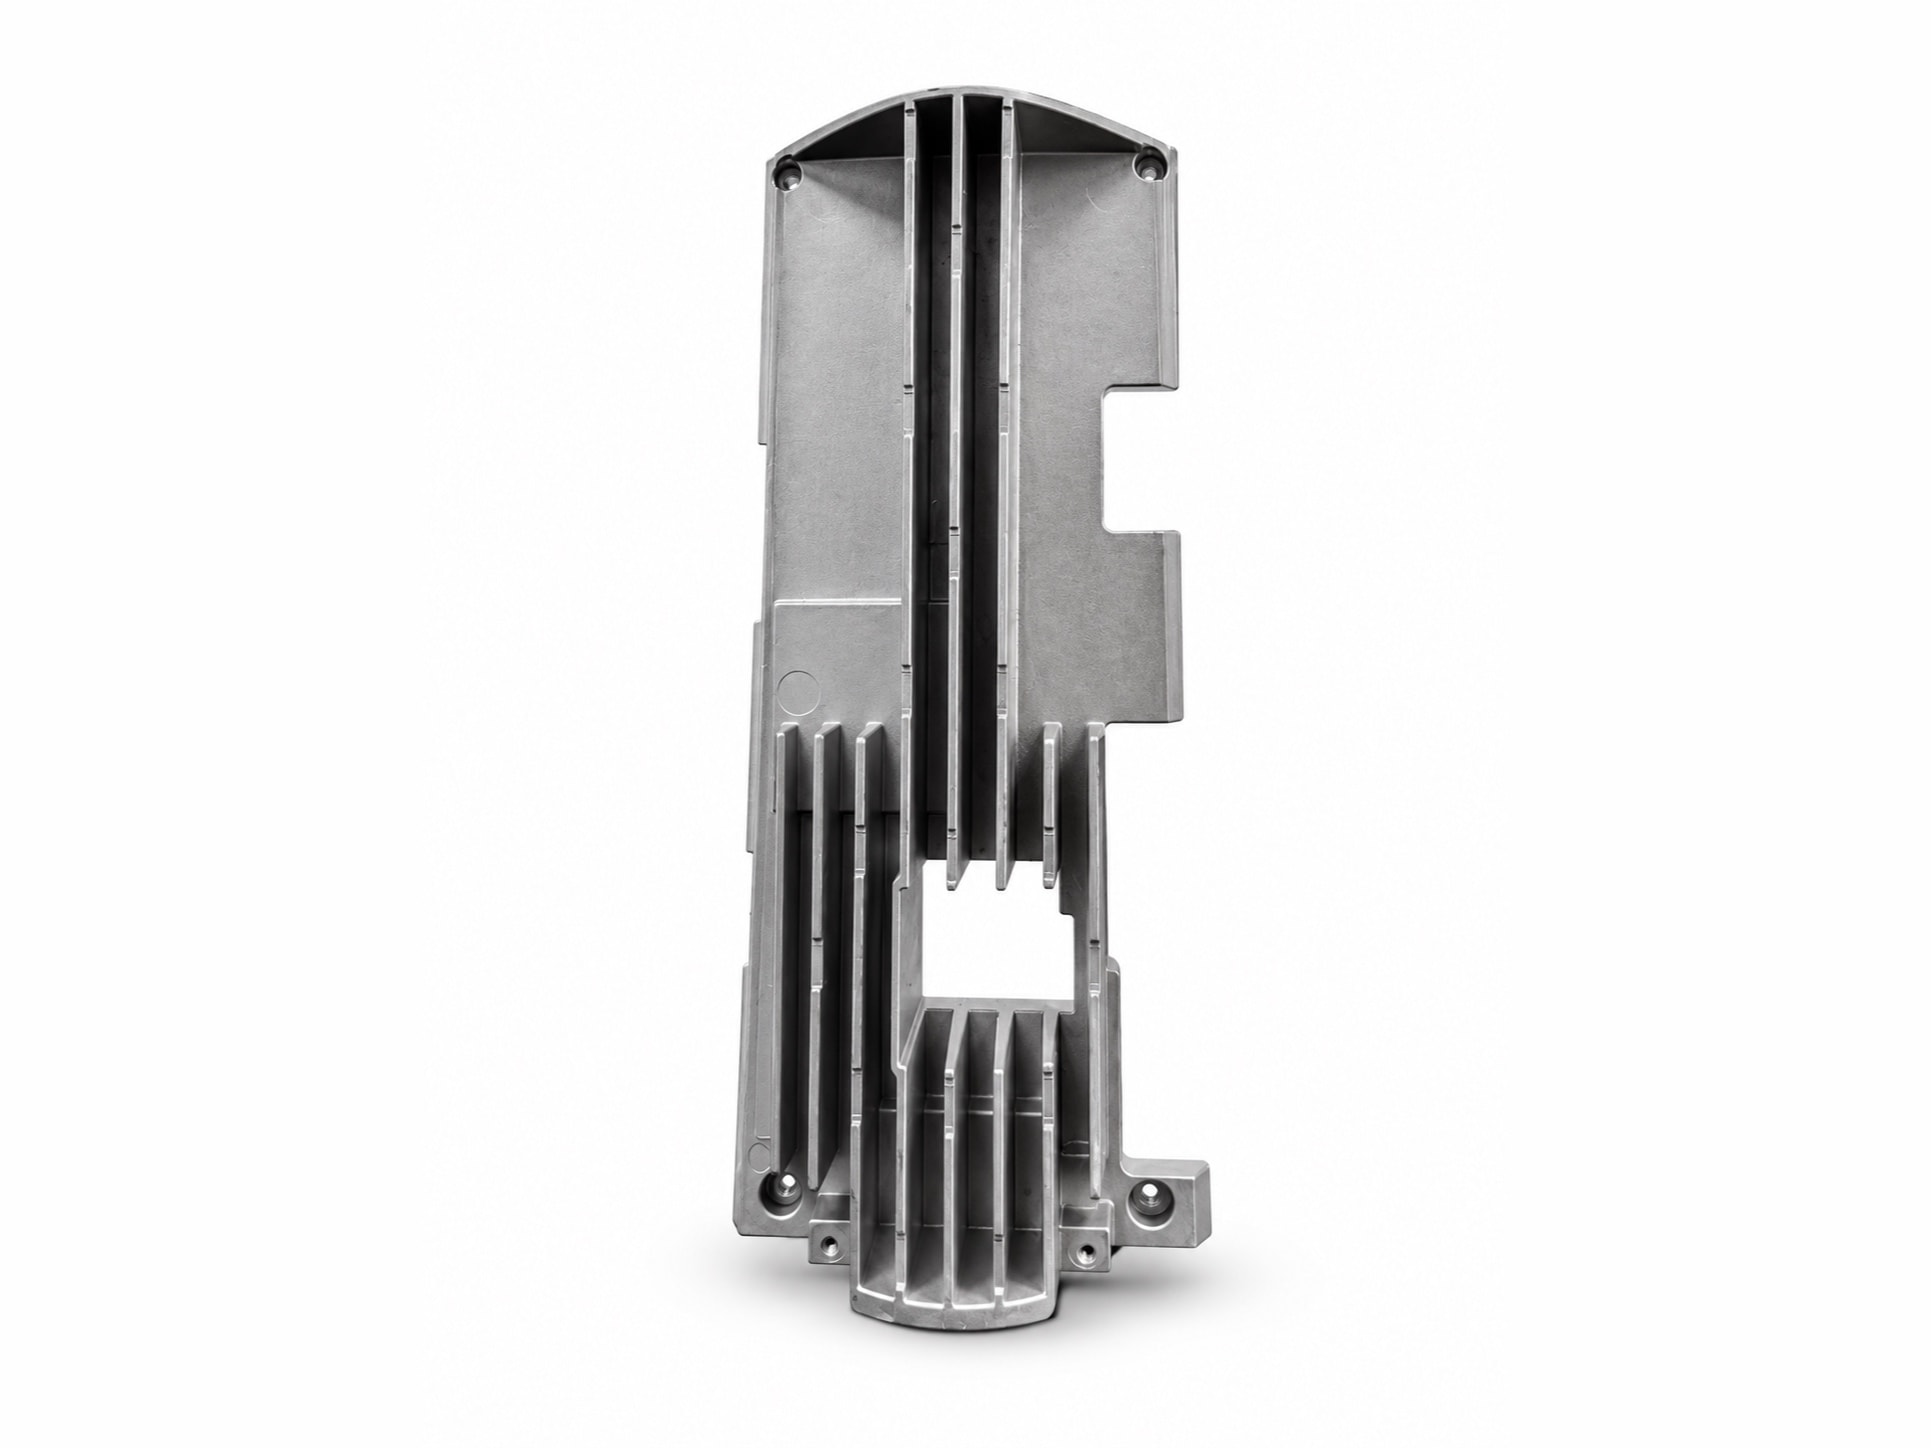
Shaped Aluminum Finned Heat Sink Plate

Shaped Aluminum Finned Heat Sink Plate

AluminumHeat Sinks & Structural EnclosuresDie castingCNC machiningFinishingThermalPrecision

An irregular plate with 2 mm fins and seven bosses among them. Flow-led gating, spot-cooled boss cores and more draft give over 99% fin fill and cut drag marks from 4% to under 0.5%.

ADC12 (JIS H5302) · 约 480 g
Long Aluminum Heat Sink Base Housing

Long Aluminum Heat Sink Base Housing

AluminumHeat Sinks & Structural EnclosuresDie castingCNC machiningFinishingThermalPrecision

A 320 mm housing with long internal fins and an asymmetric section warped 0.6 mm. Multi-point gating, zoned cooling and stress relief brought it within 0.15 mm, base flat to 0.05 mm/100 mm.

ADC12 (JIS H5302) · 约 780 g
Aluminum Gearbox Housing

Aluminum Gearbox Housing

AluminumOther sectorsDie castingCNC machiningFinishingPressure tightPrecision

Bearing bosses opened porosity on boring, and bores machined apart from the joint face did not line up. Cored bosses and one-setup machining now hold ±0.03 mm and 98% first-pass leak test.

ADC12 (JIS H5302) · 约 1.2 kg
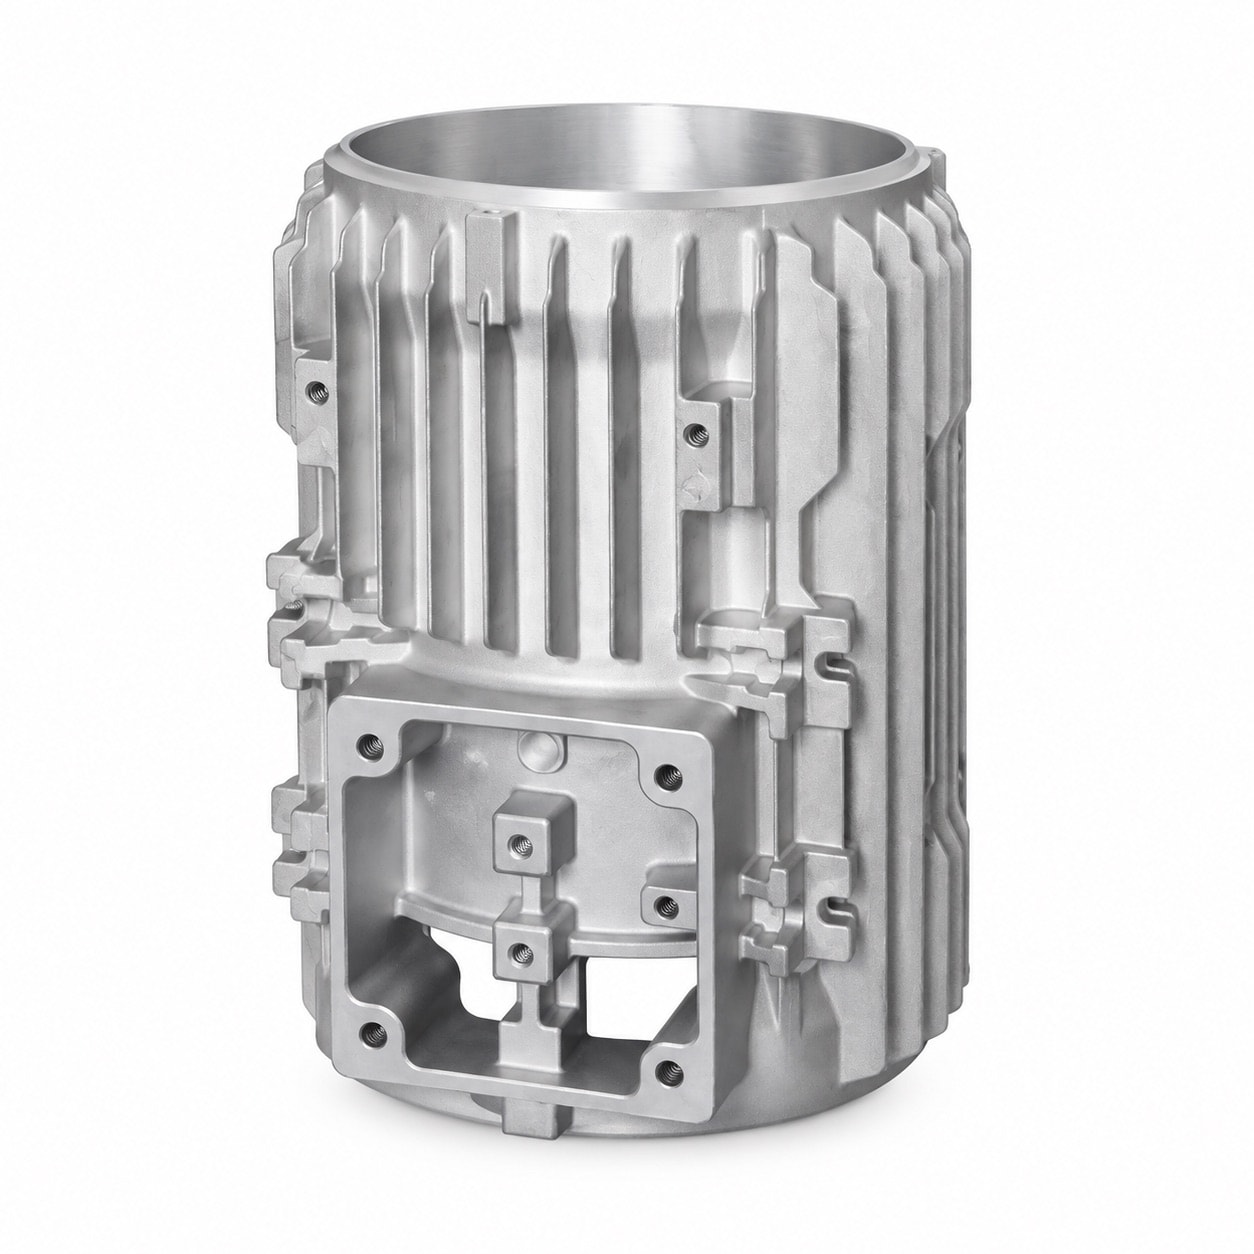
Finned Aluminum Motor Housing

Finned Aluminum Motor Housing

AluminumOther sectorsDie castingCNC machiningFinishingPrecisionThermal

A thin-walled bore, two pilots and a coating step between roughing and finishing. A fin-located, axially clamped fixture and one datum throughout hold 0.02 mm roundness and φ0.03 mm coaxiality.

ADC12 (JIS H5302) · 约 2.6 kg
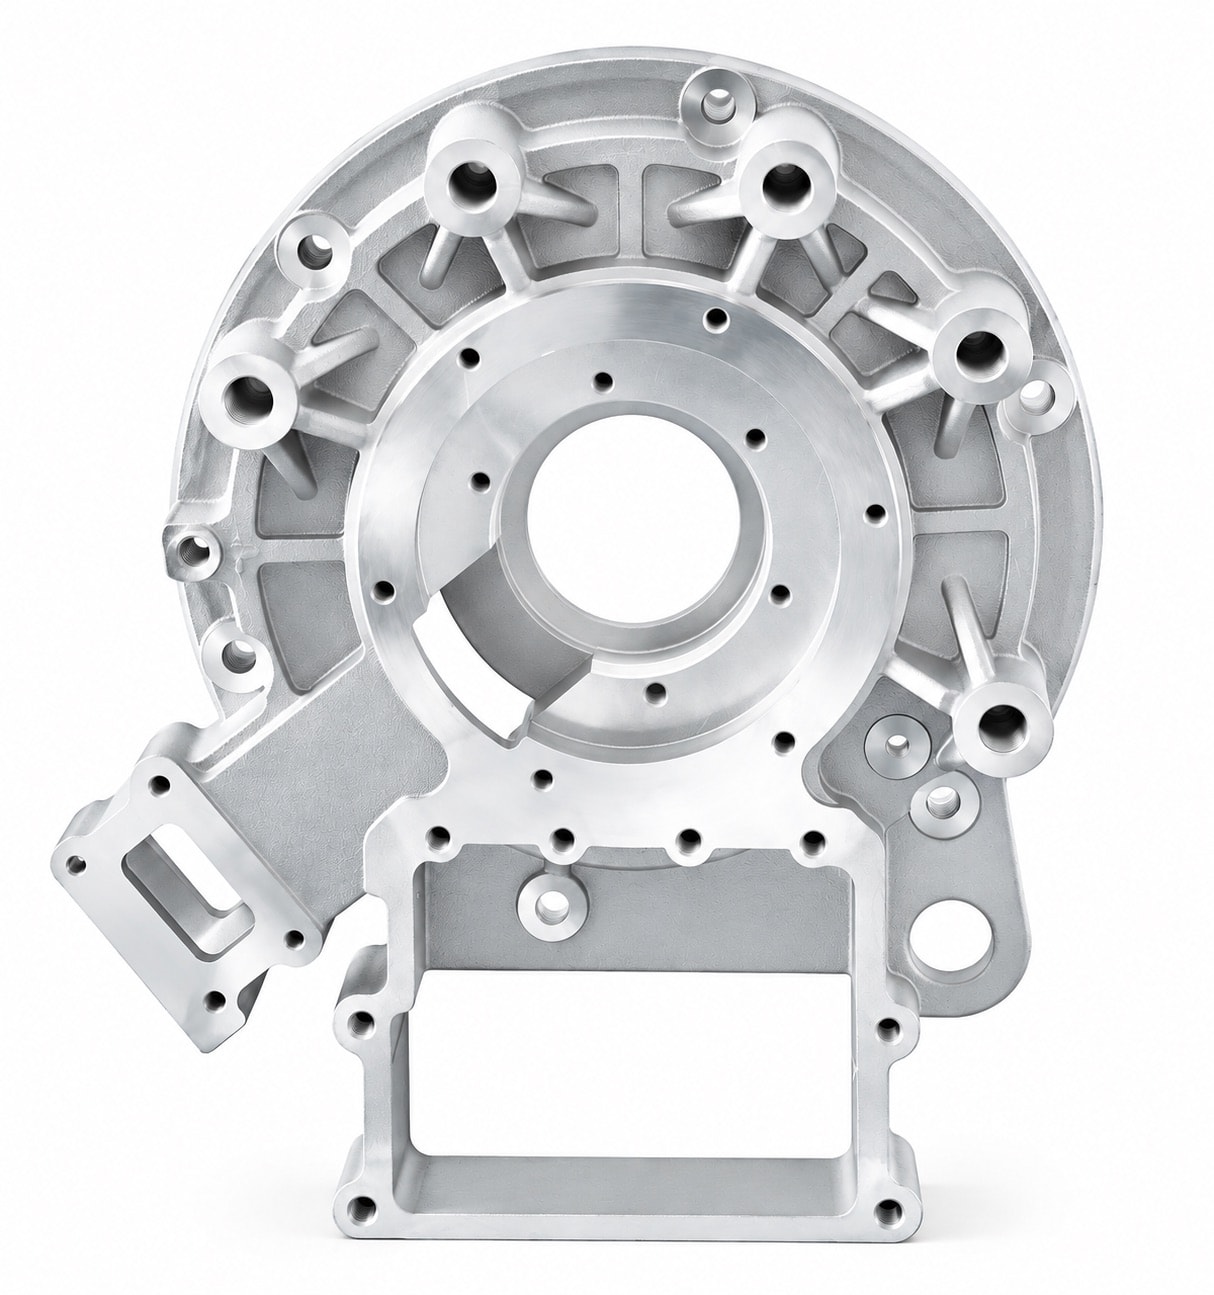
Aluminum Motor Rear End Cover

Aluminum Motor Rear End Cover

AluminumOther sectorsDie castingCNC machiningPrecision

Heavy mounting bosses on this bearing-carrying end cover showed shrinkage on X-ray. Split, re-angled gates and local squeeze cleared it to ASTM E505 level 2; bearing bore coaxial within φ0.03 mm.

ADC12 (JIS H5302) · 约 2.2 kg