JINXIONGMANUFACTURING
Die-cast parts in production

CASE STUDIES

Die casting cases: the problem, the method and the production data

All the cases below are real parts in series production, covering zinc and aluminum die casting, CNC machining, surface finishing and assembly. Each one sets out the technical problem the customer faced, how we controlled it in the process, and the measured figures once production settled.

Alloy
Industry
Part type
Process
Key requirement

9 / 26 cases

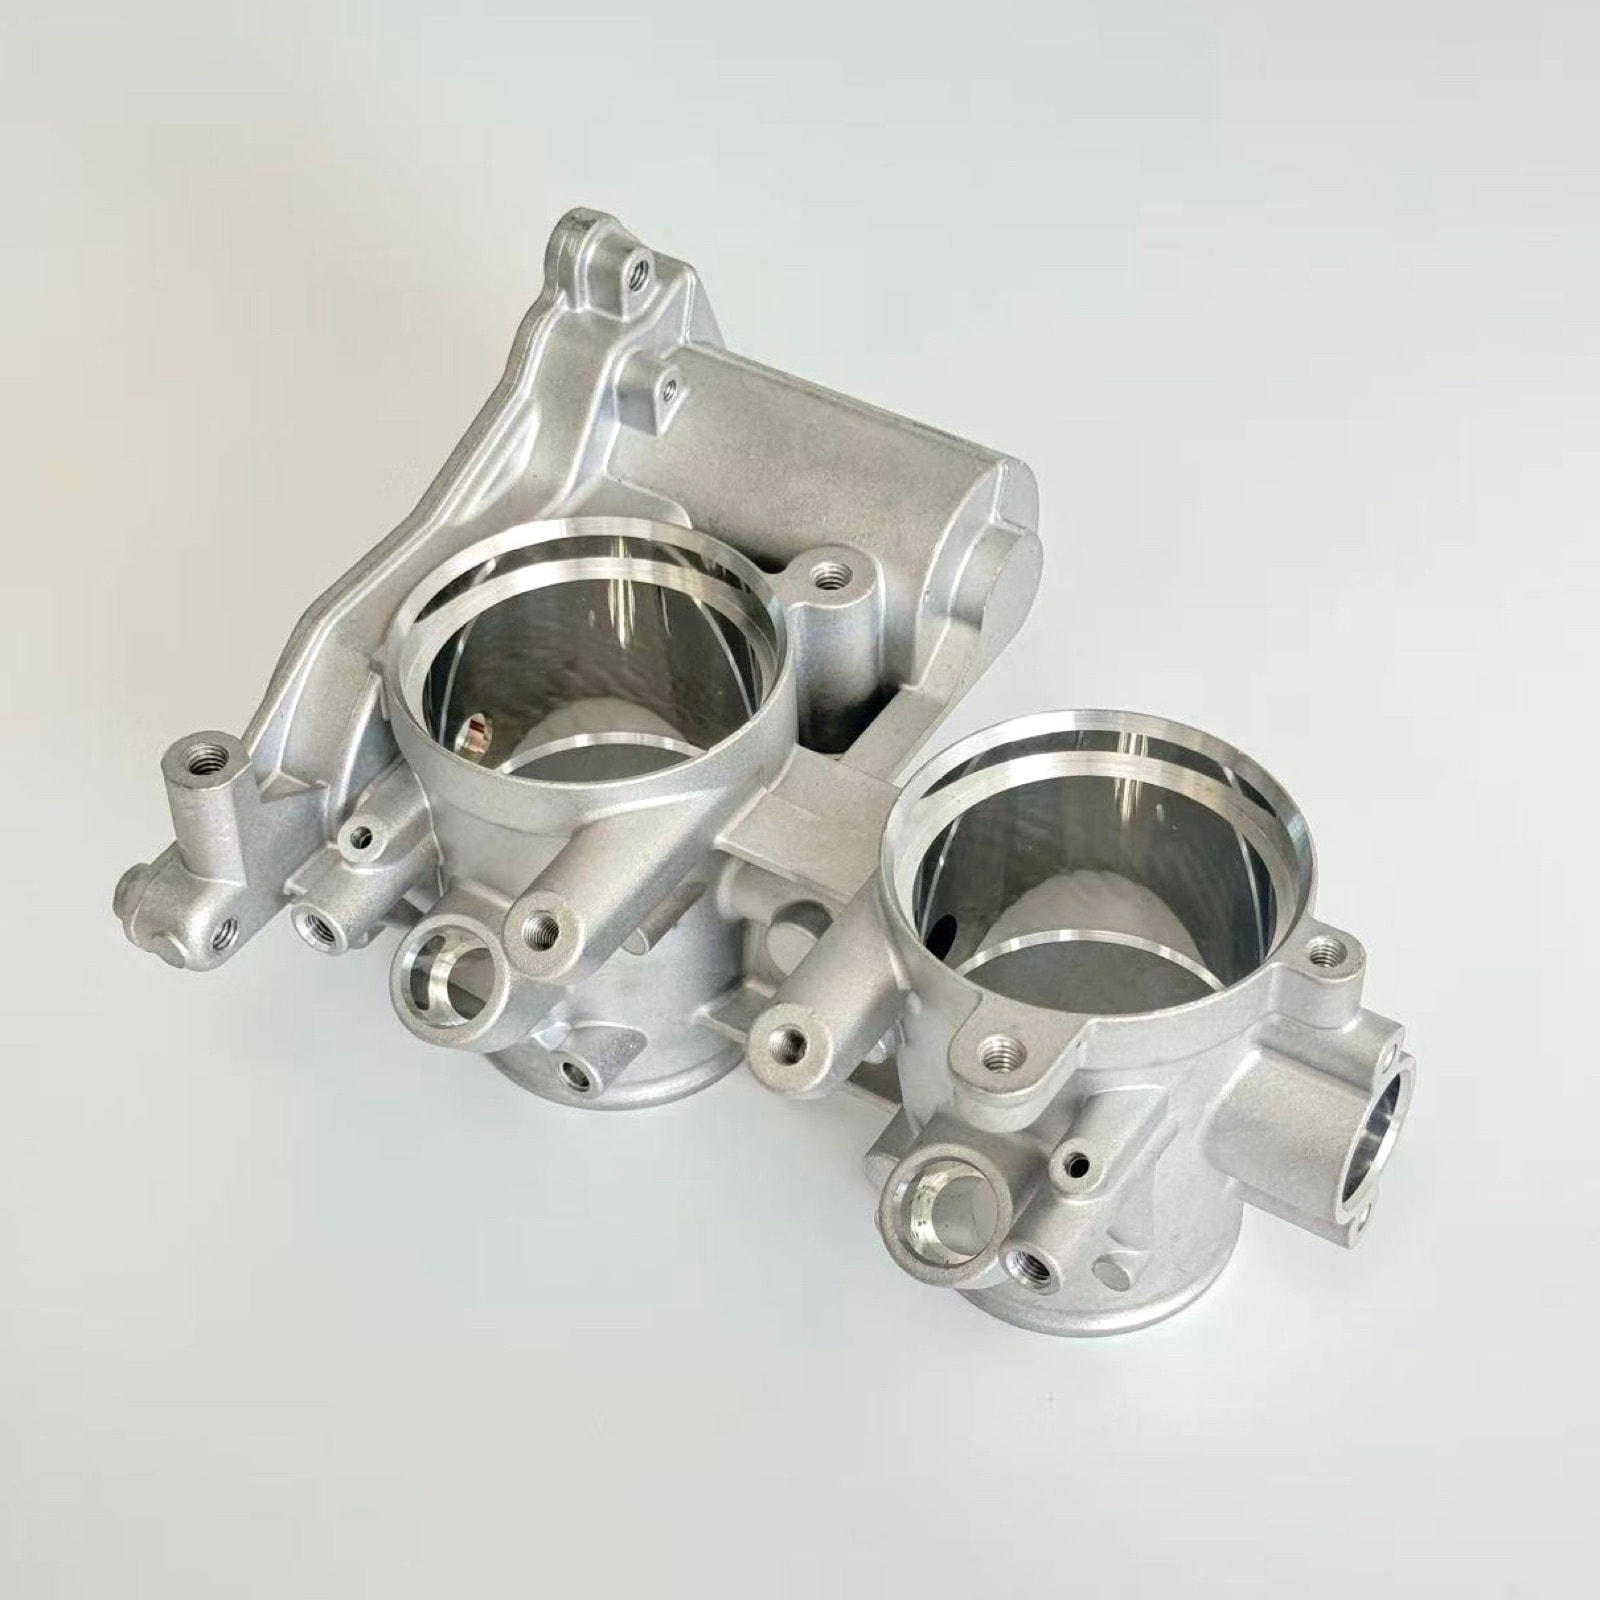
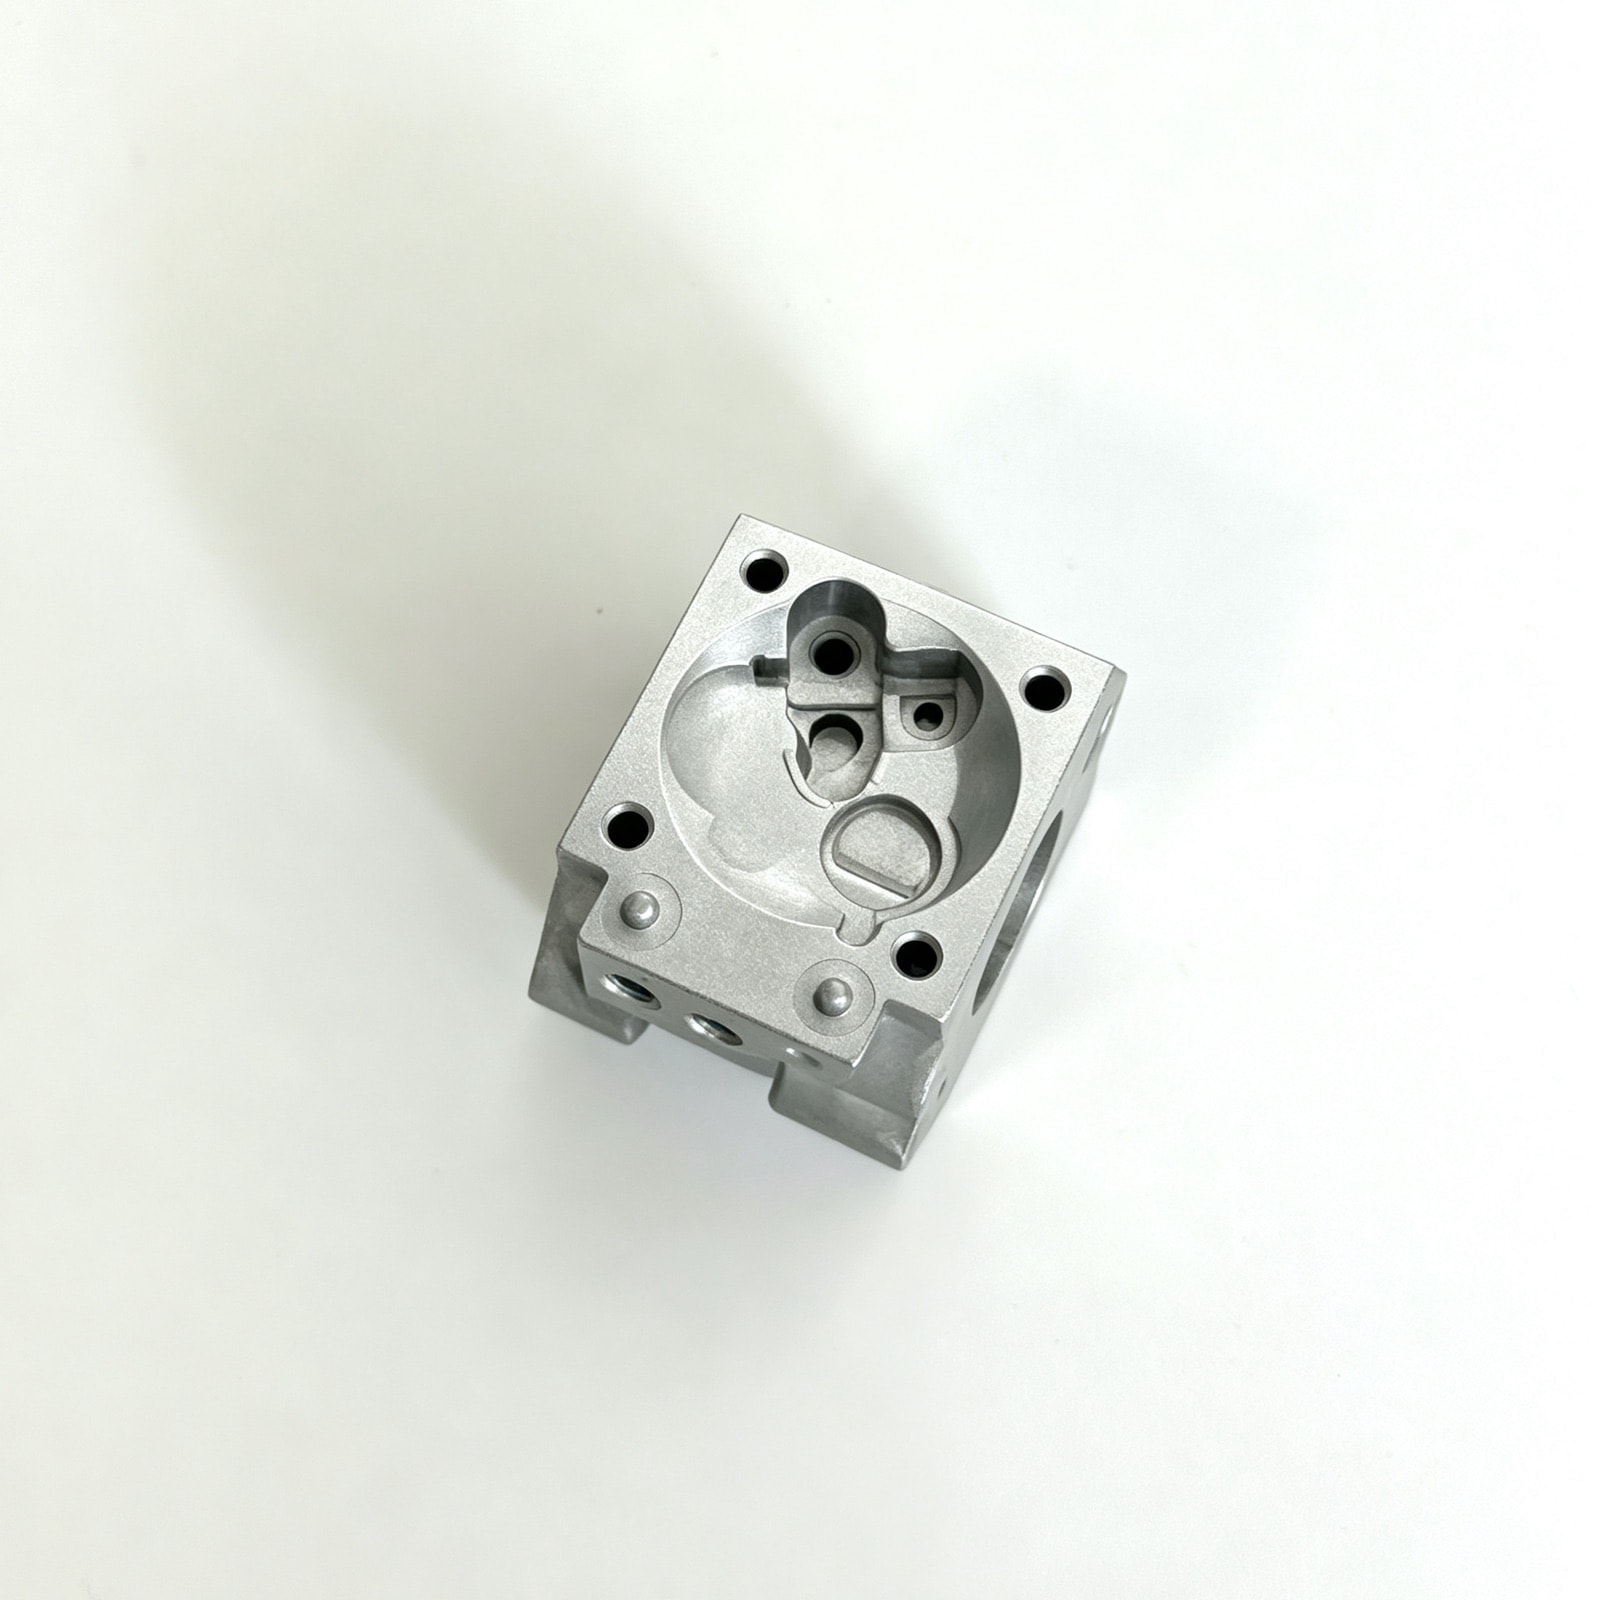
Motorcycle Twin Throttle Body

Motorcycle Twin Throttle Body

AluminumMotorcycle & Two-WheelerDie castingCNC machiningPressure tightPrecision

Machined in two setups, the twin bores differed by up to 0.05 mm and the engine idled rough. One-setup boring and soft jaws now match them within 0.02 mm.

ADC12 (JIS H5302) · 约 520 g
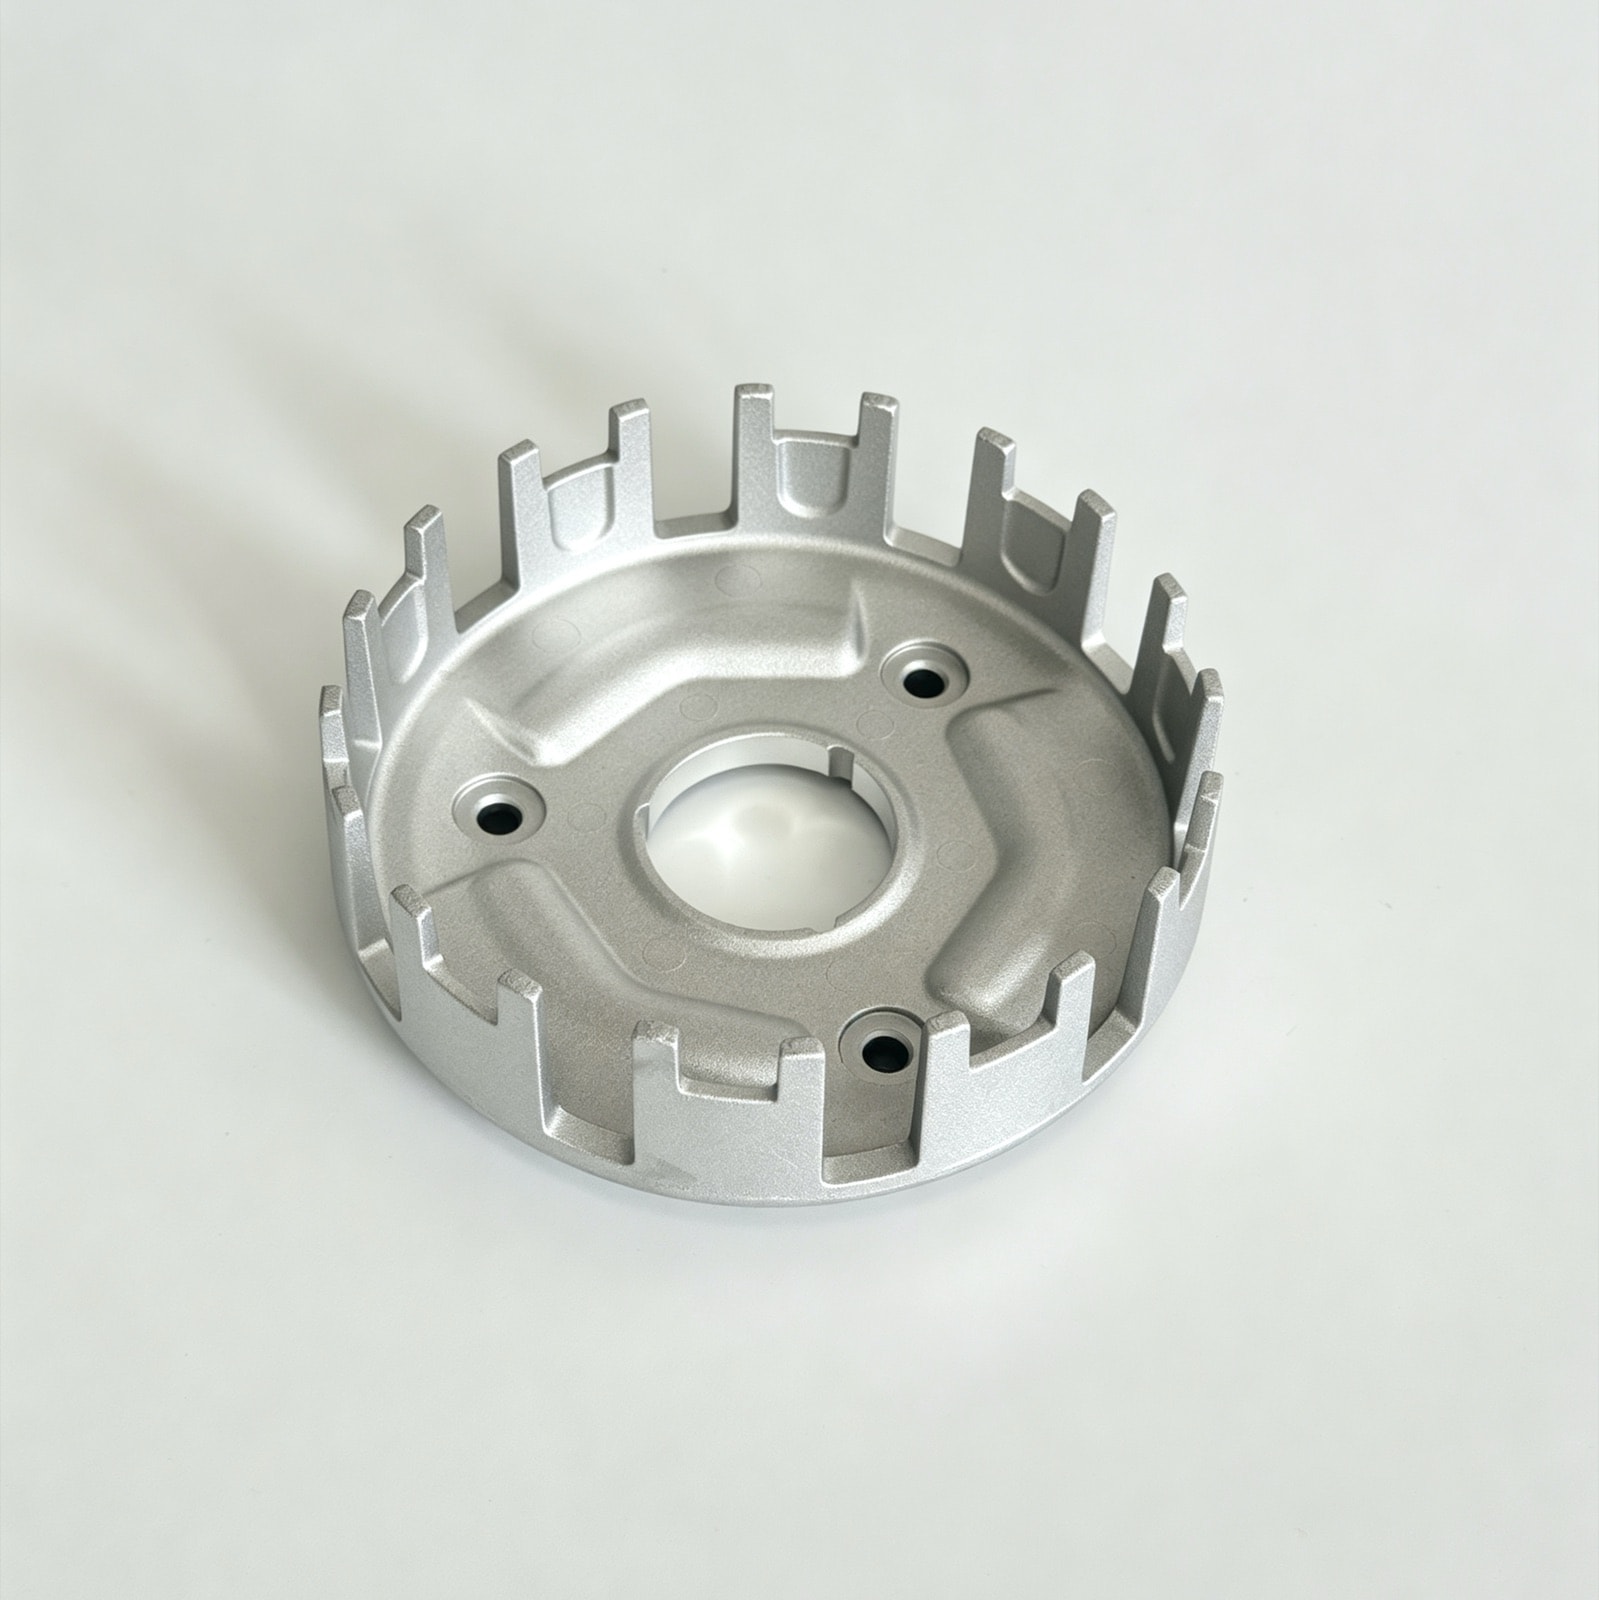
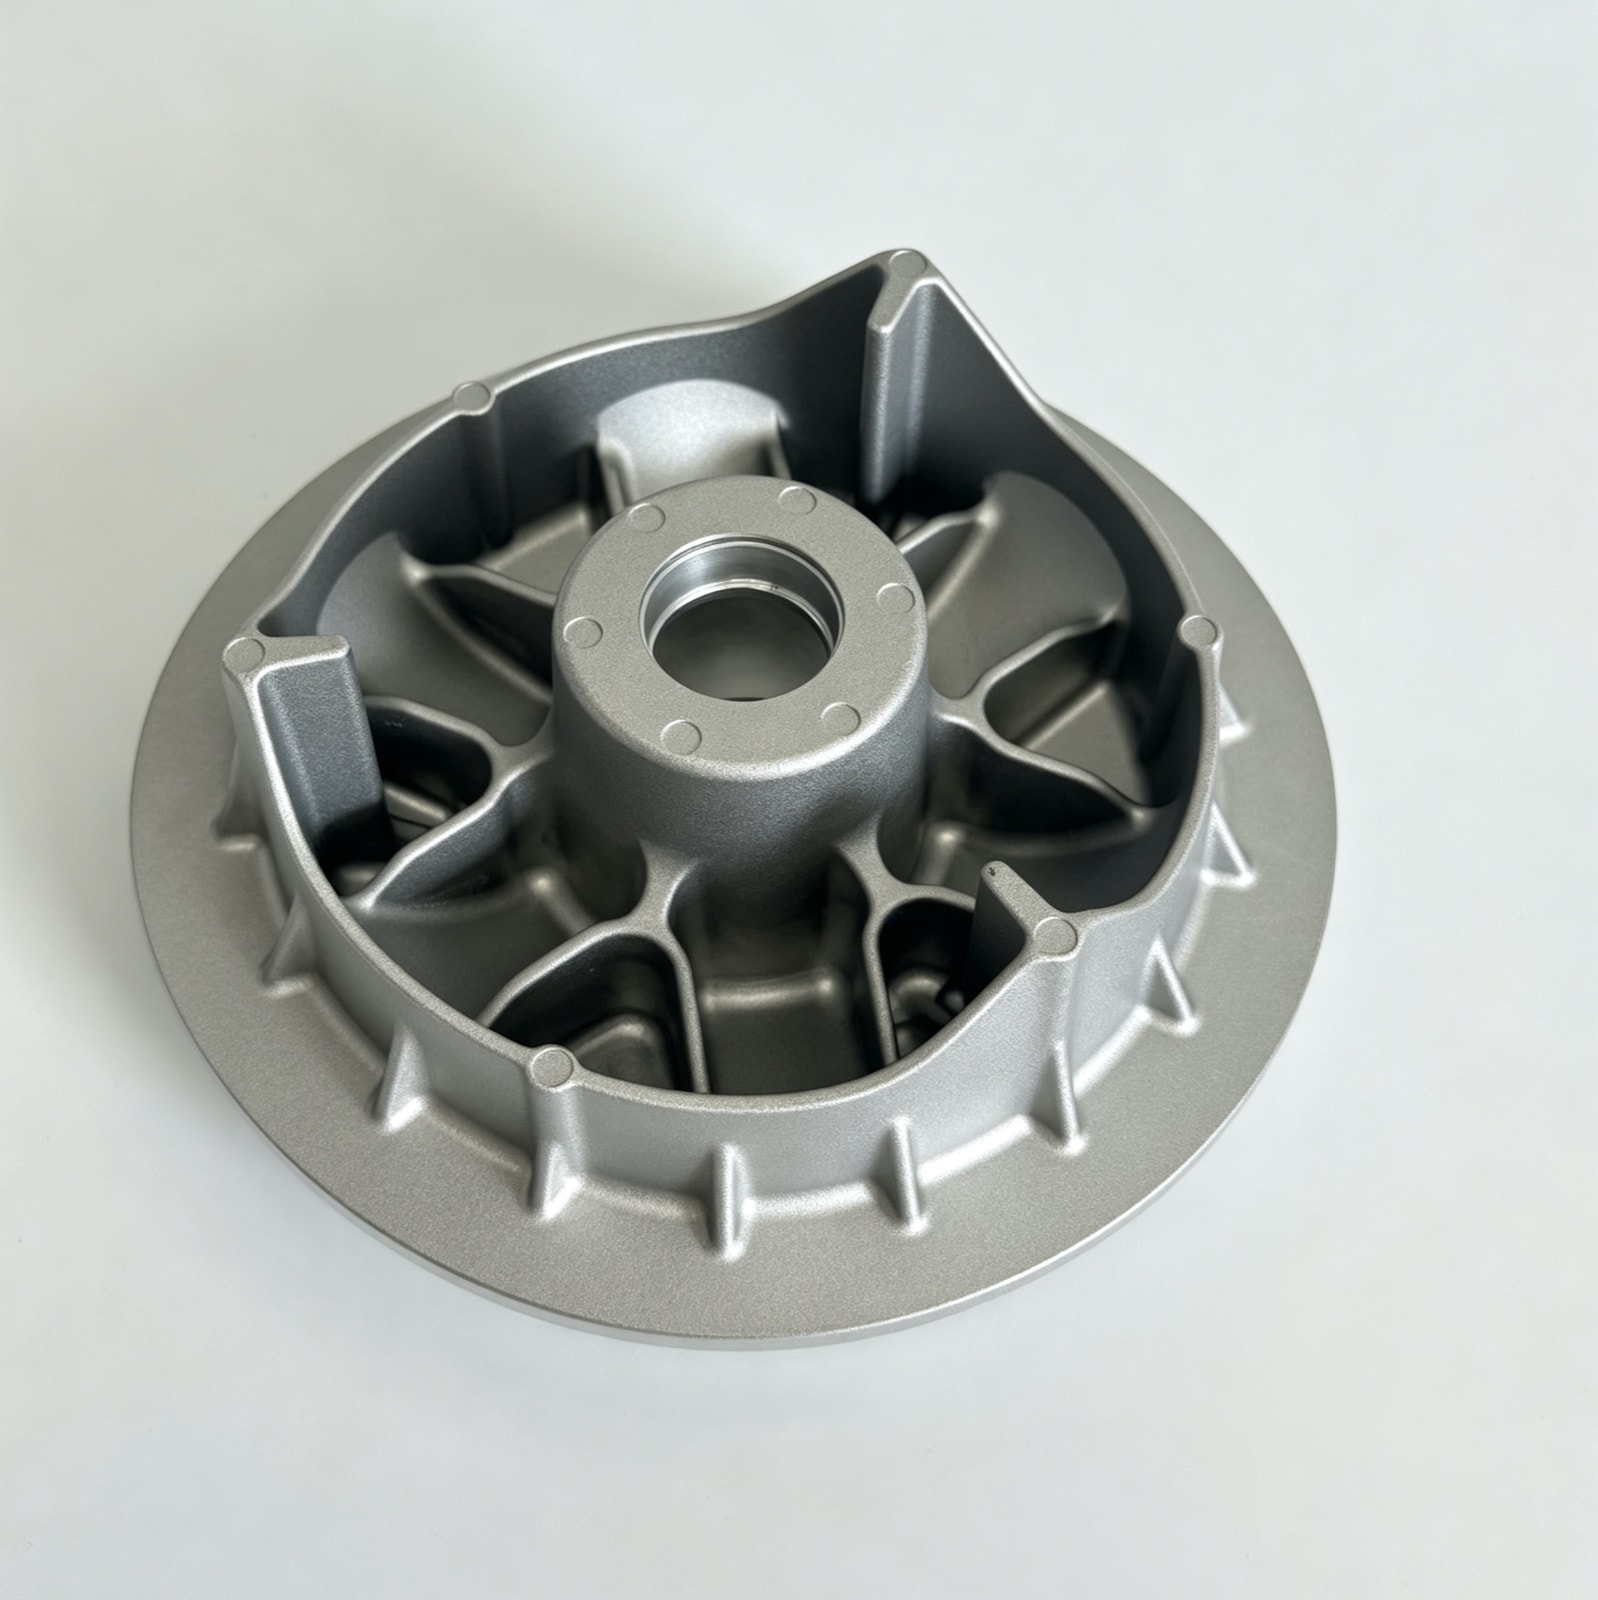
Motorcycle Clutch Basket

Motorcycle Clutch Basket

AluminumMotorcycle & Two-WheelerDie castingCNC machiningFinishingPrecision

Slot widths once varied by 0.08 mm between batches and the friction plates bound. Core cooling, scheduled core changes and 100% gauging now hold ±0.05 mm.

ADC12 (JIS H5302) · 约 330 g
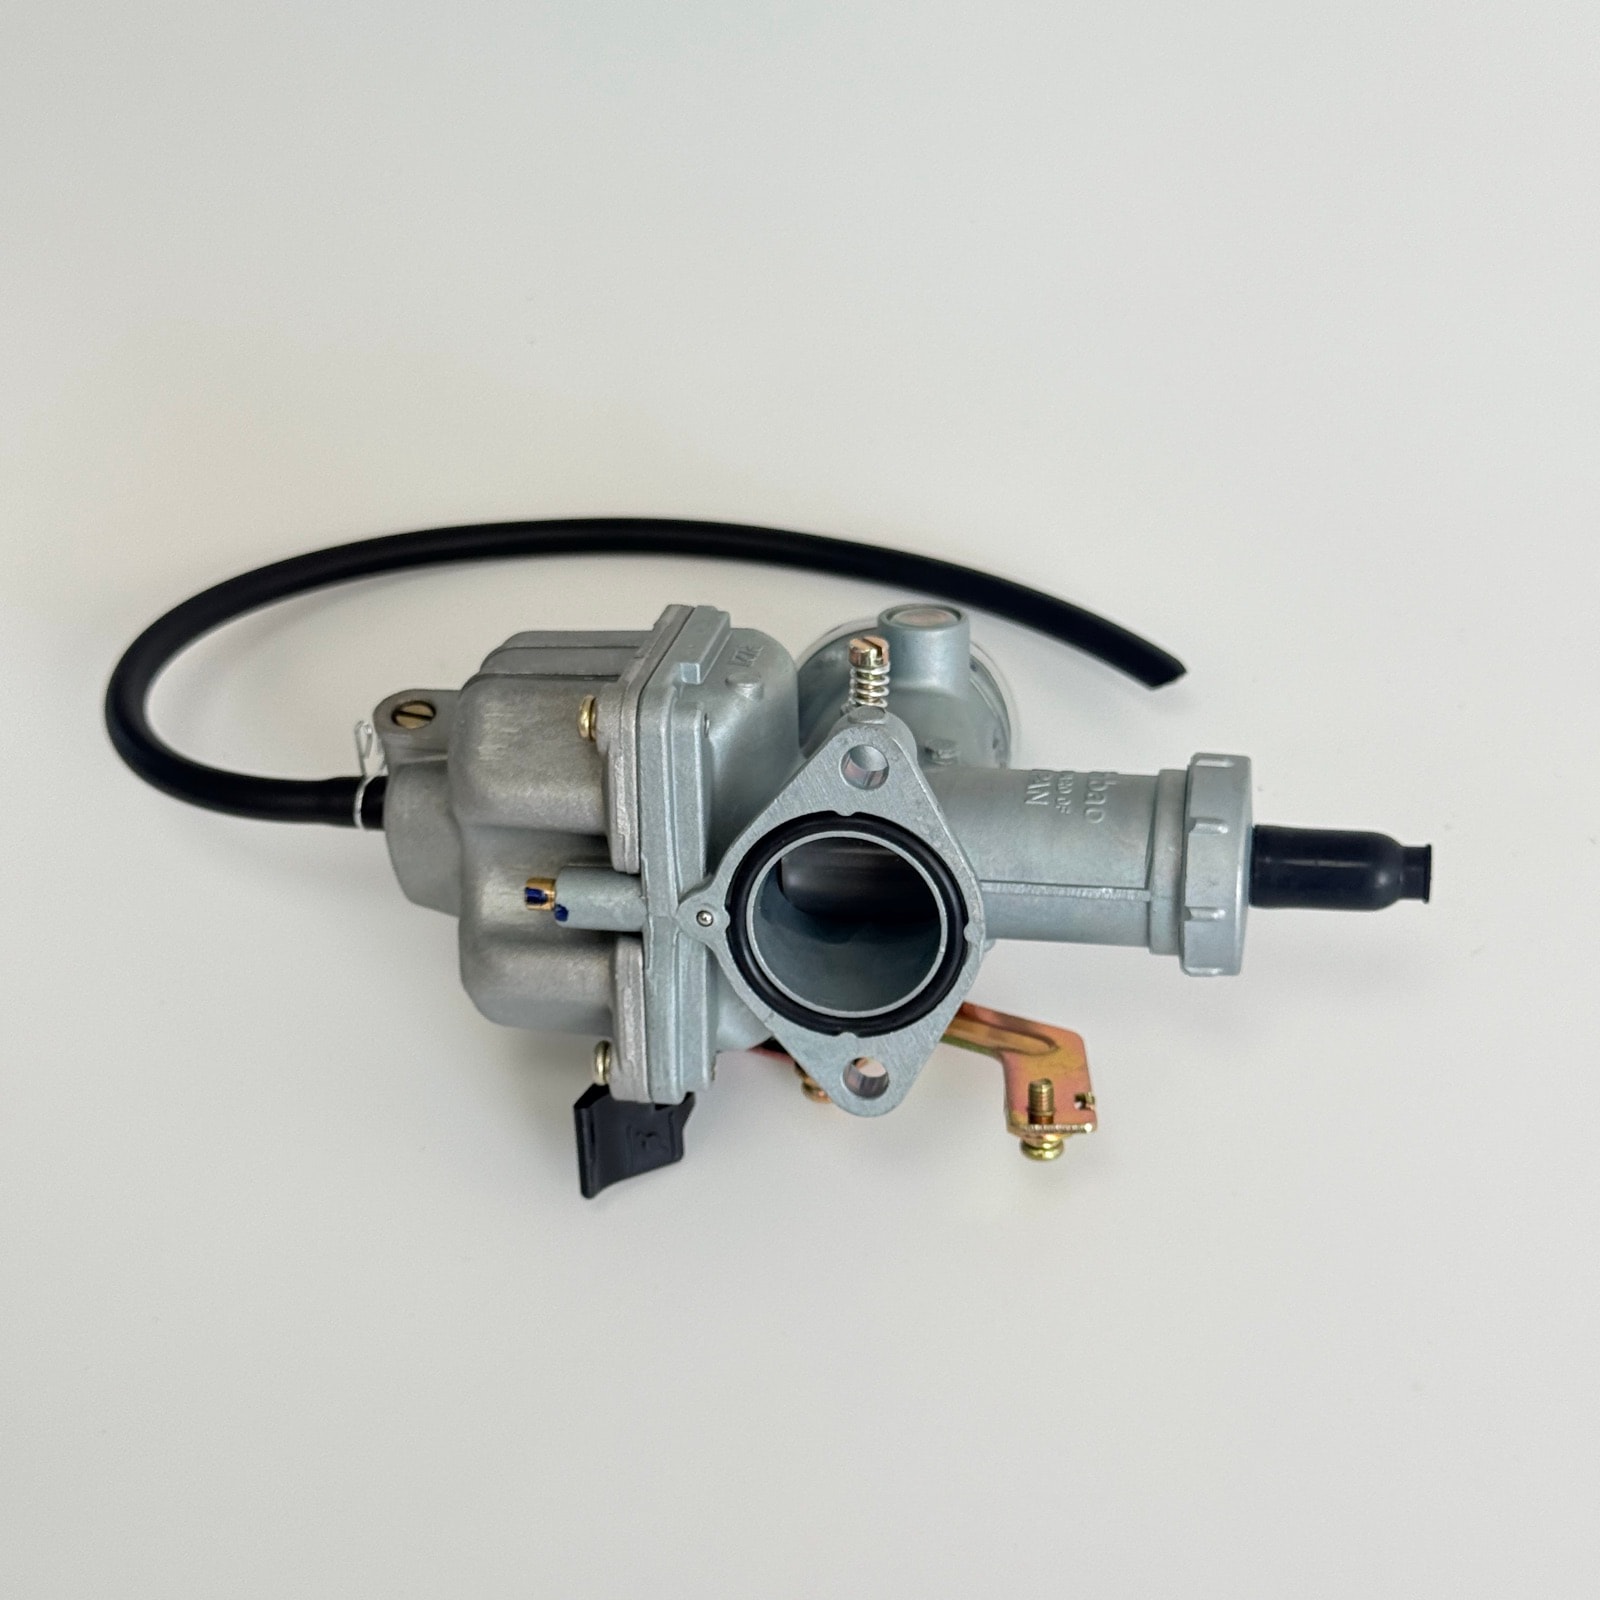
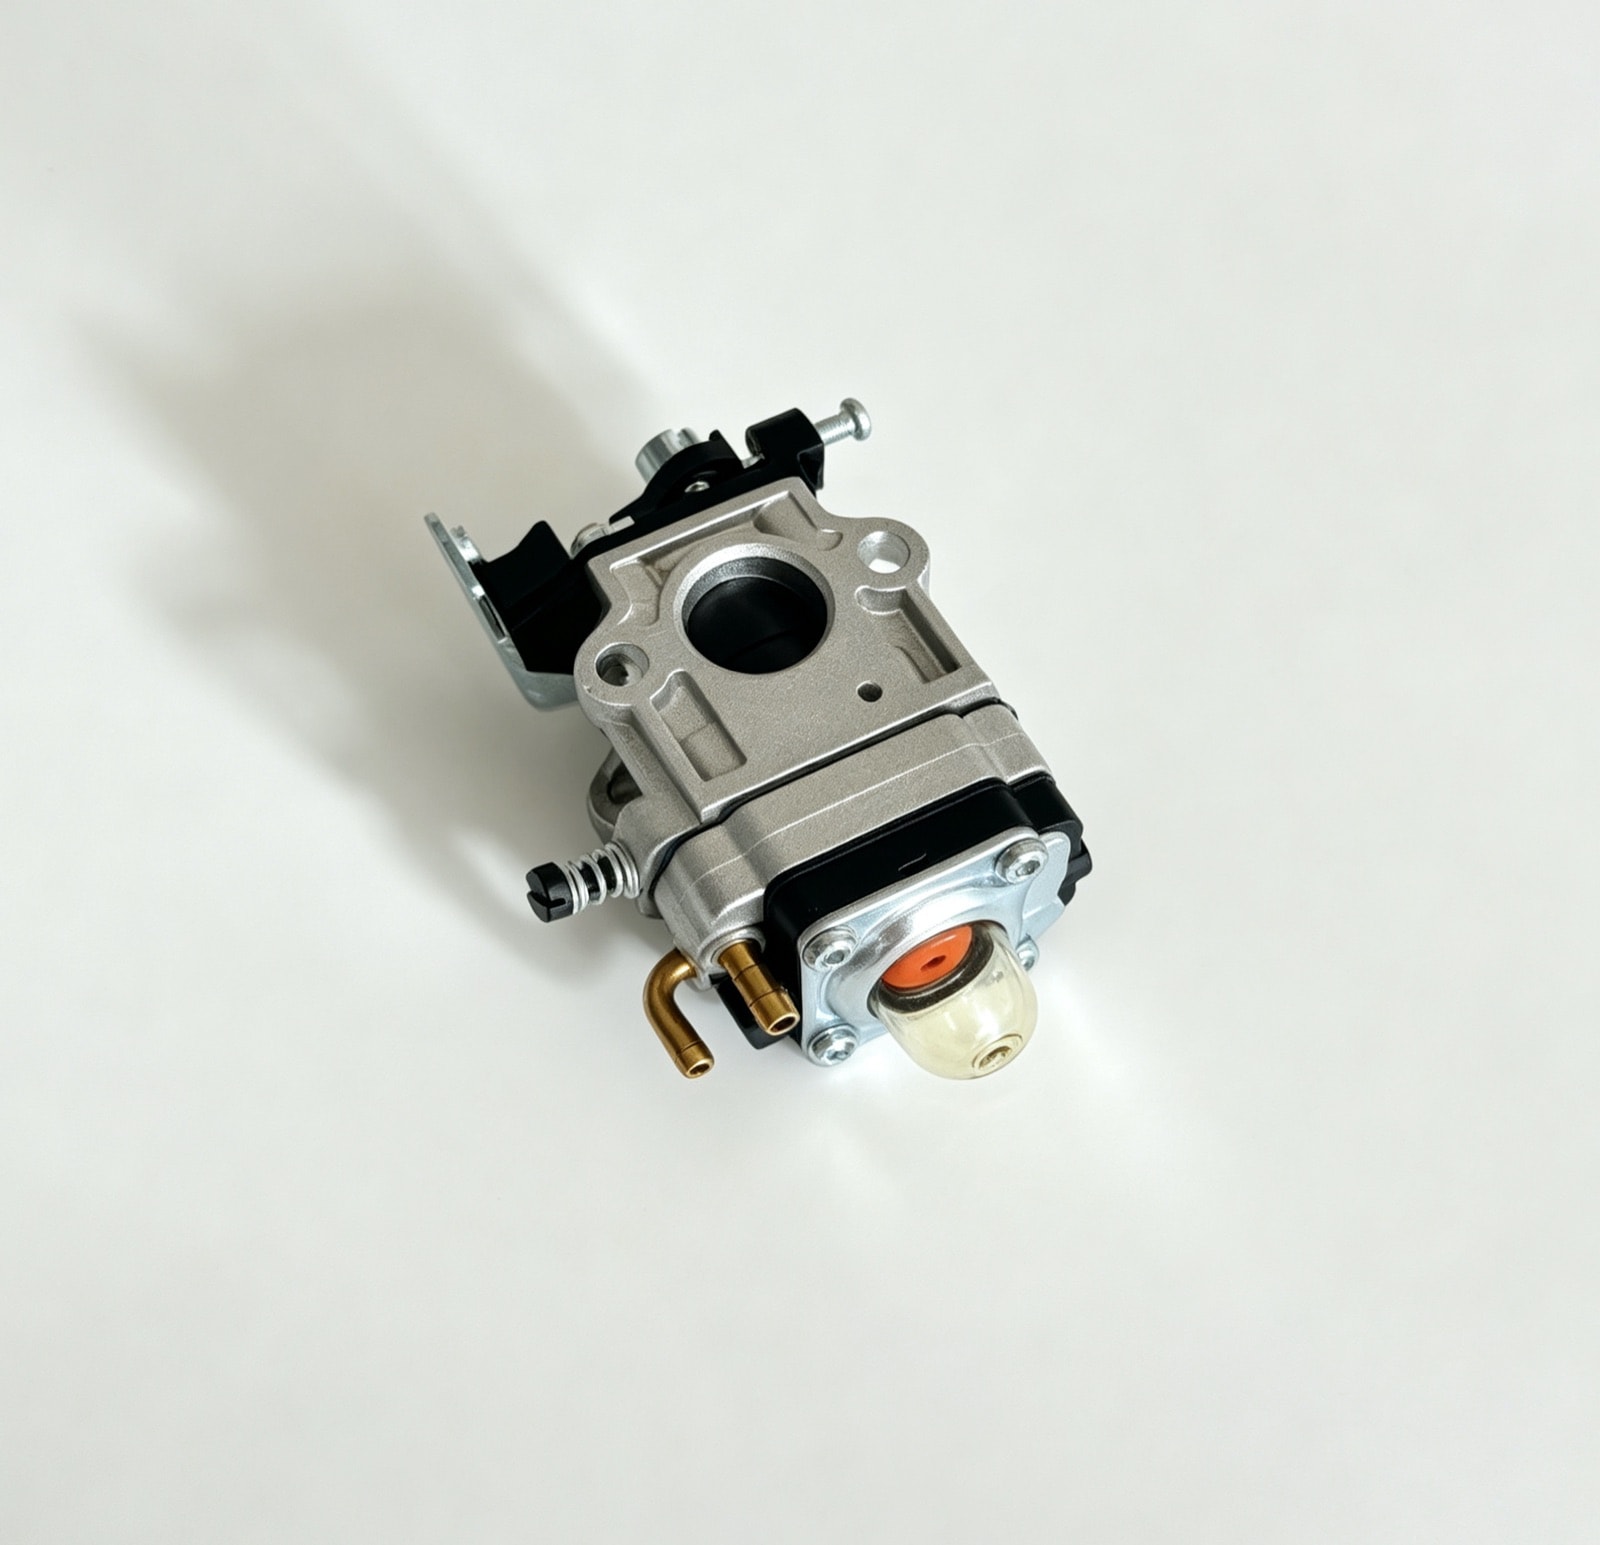
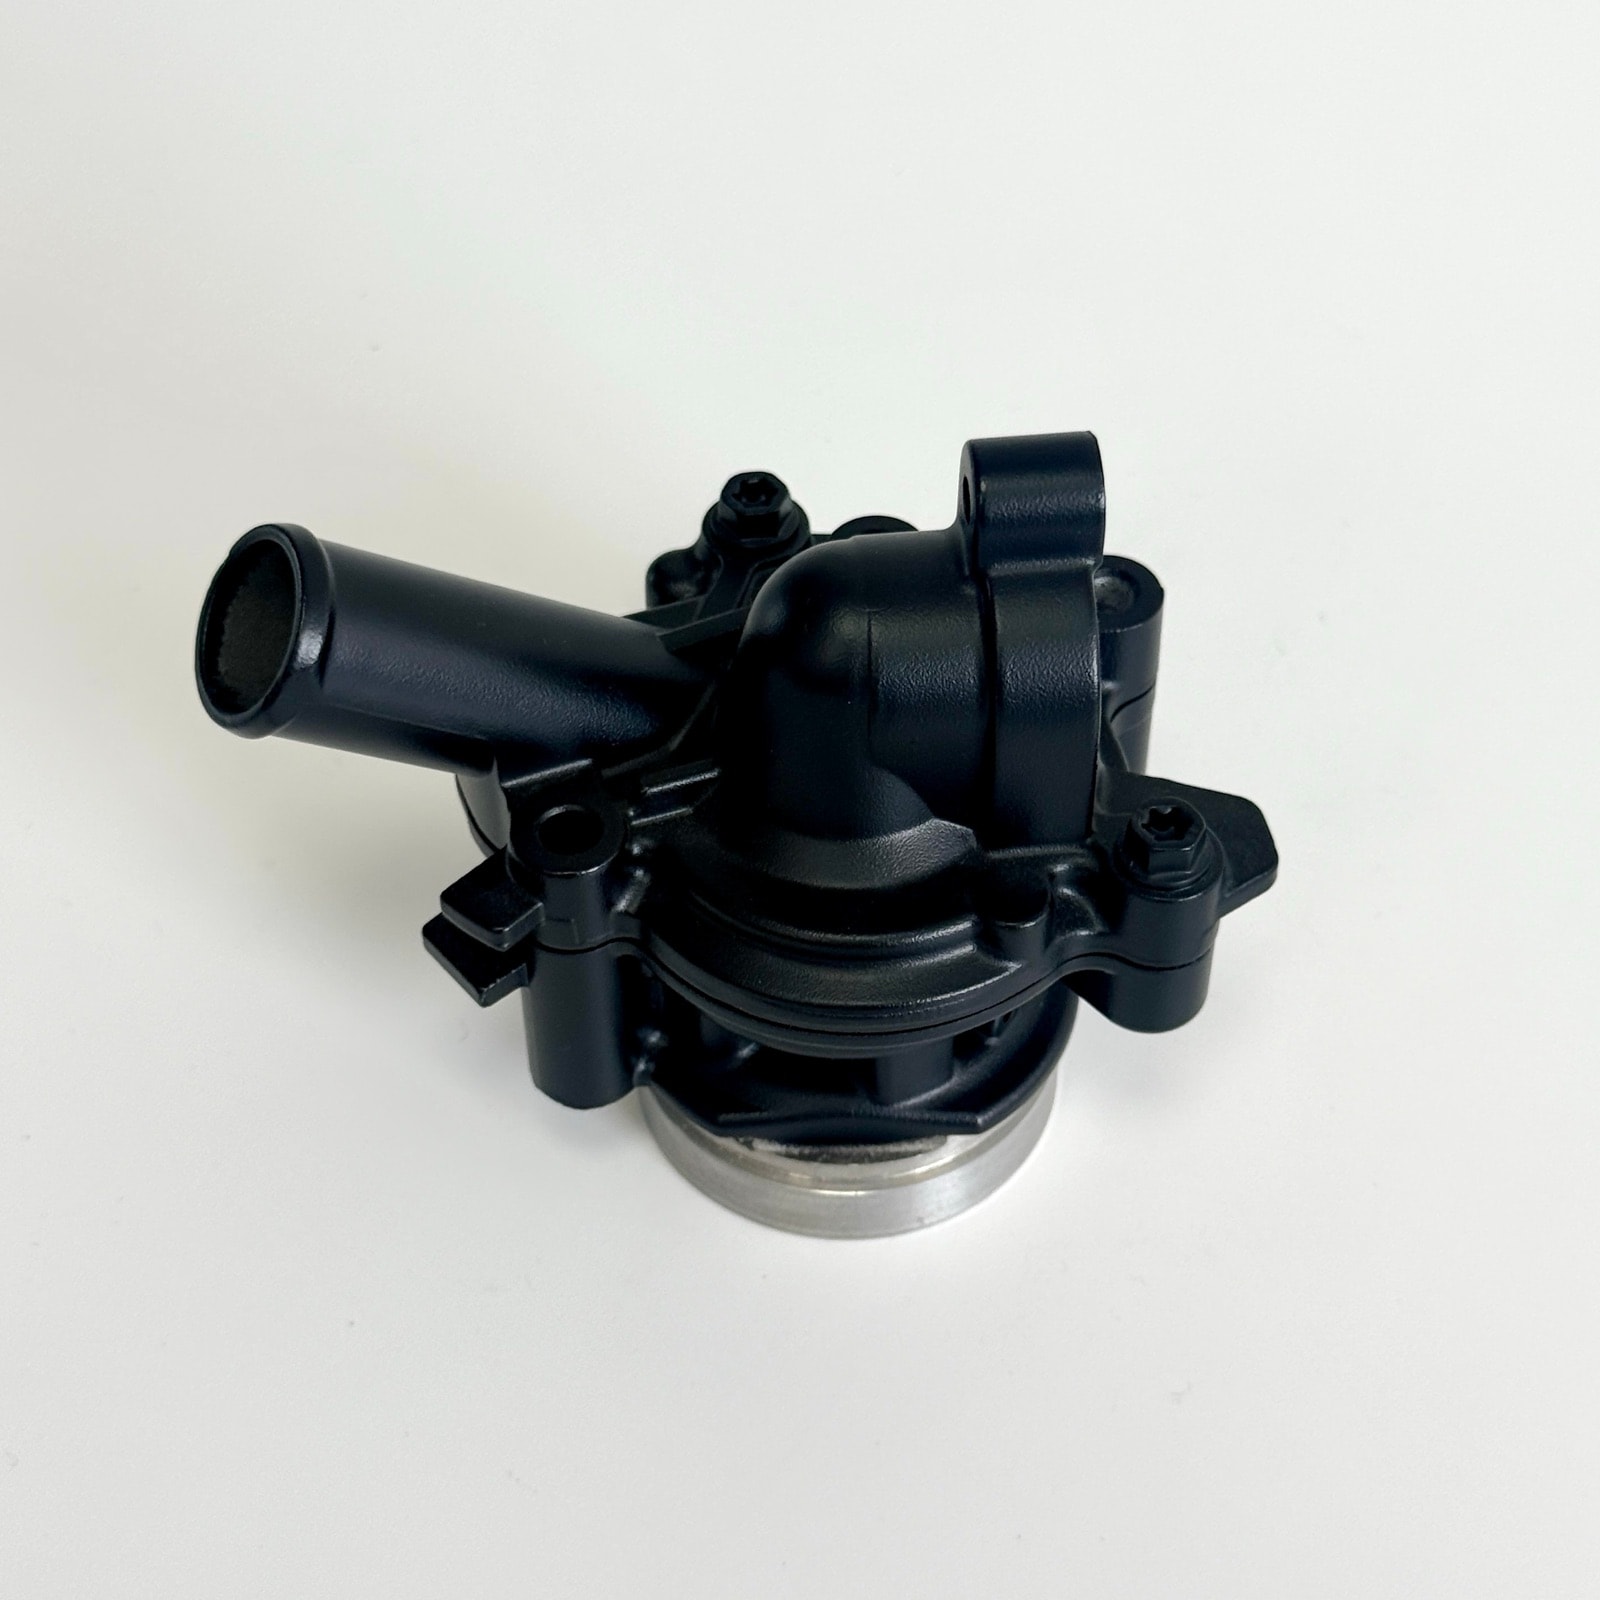
PZ27 Motorcycle Carburetor Assembly

PZ27 Motorcycle Carburetor Assembly

AluminumMotorcycle & Two-WheelerDie castingCNC machiningAssemblyPressure tightPrecision

A 0.1 mm jet shift moves idle flow by over 5%. One-datum machining, flow-sorted jets and 100% bench testing hold ±2%, with over a million delivered.

ADC12 (JIS H5302) · 约 420 g(总成)
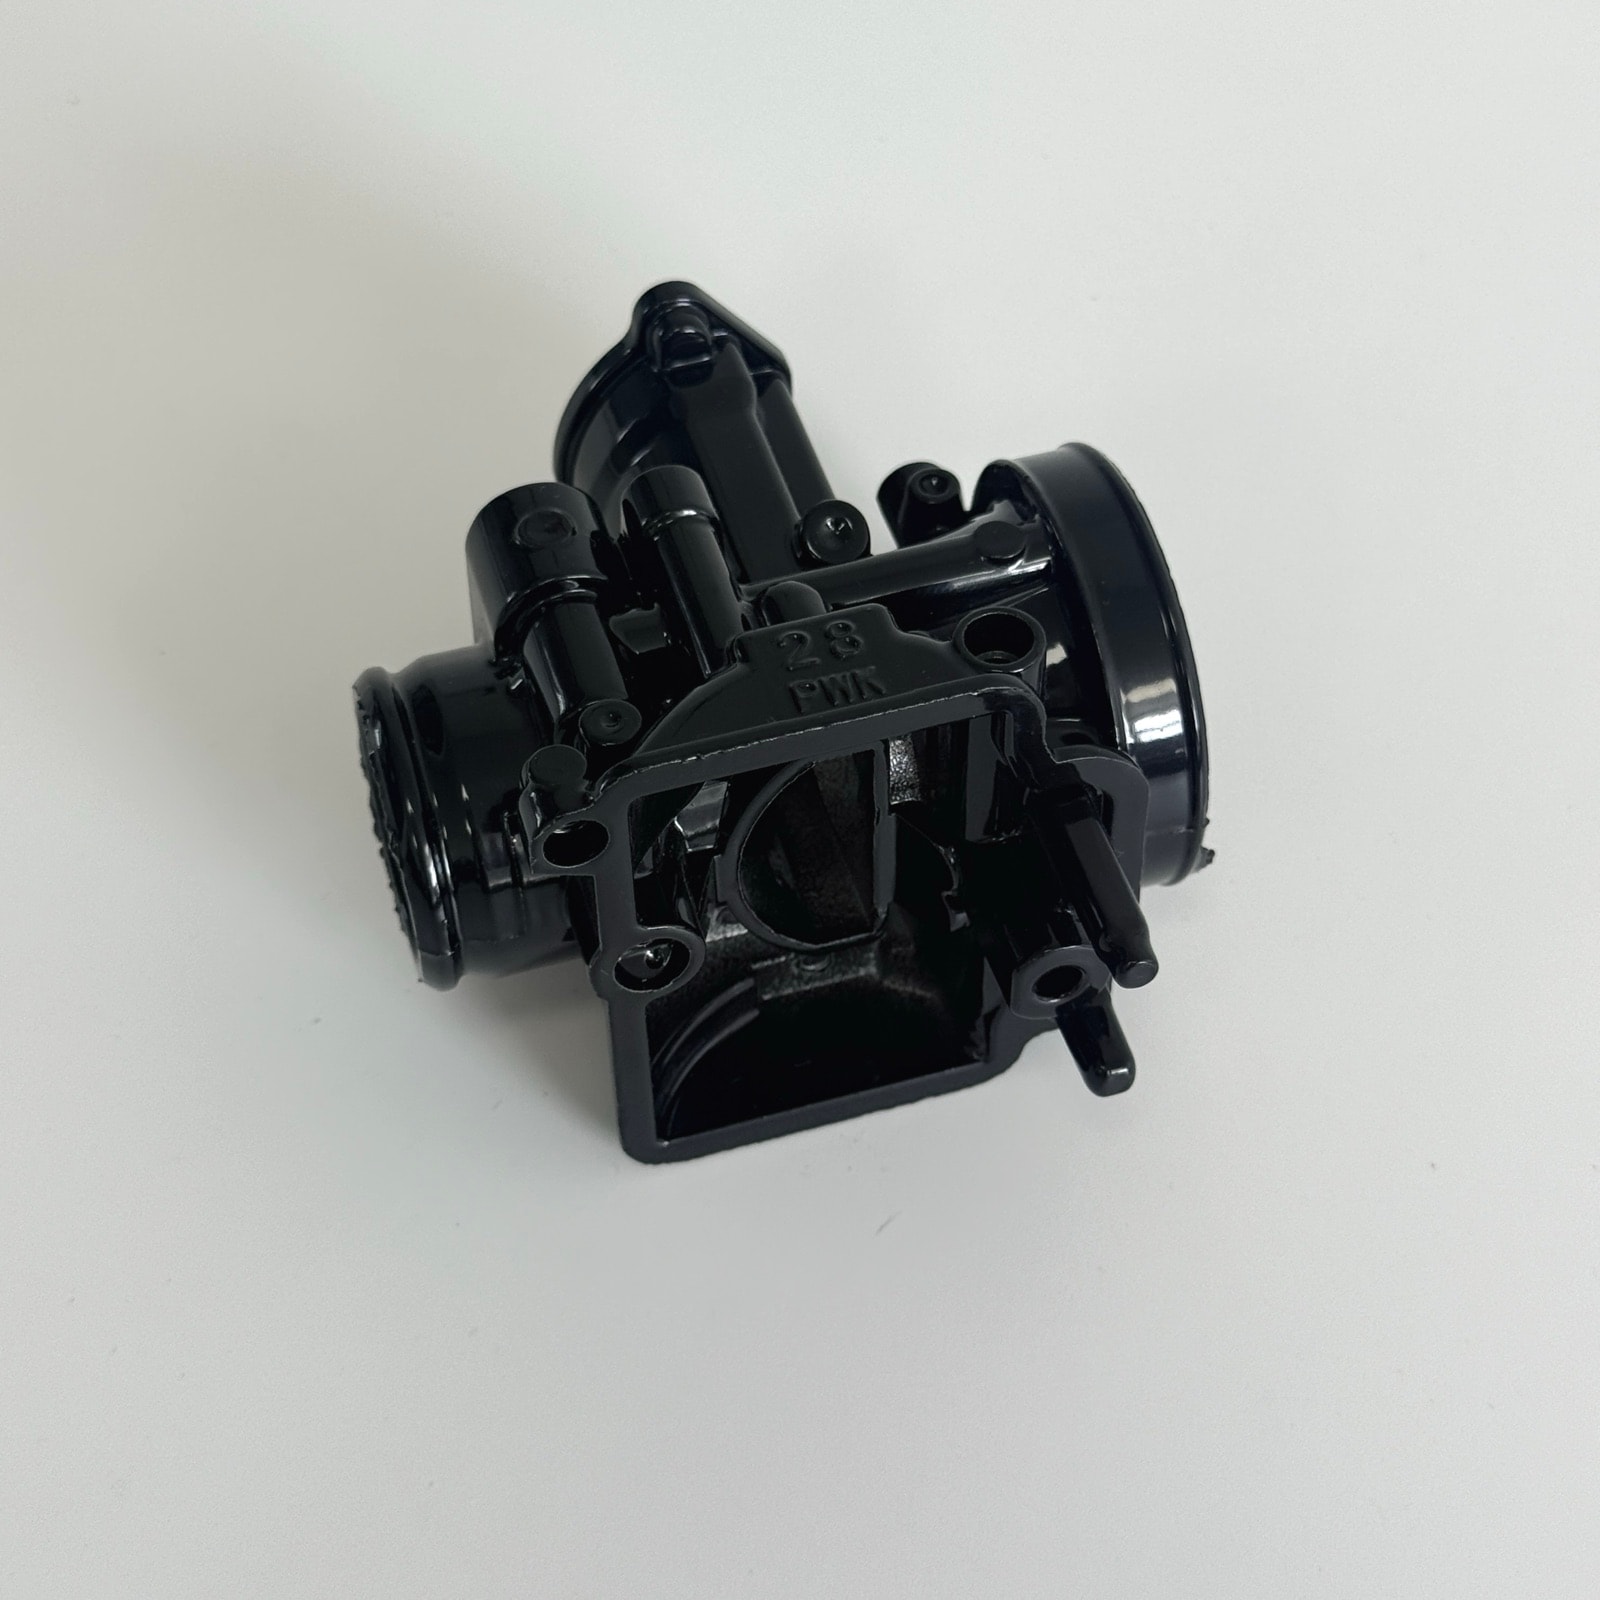
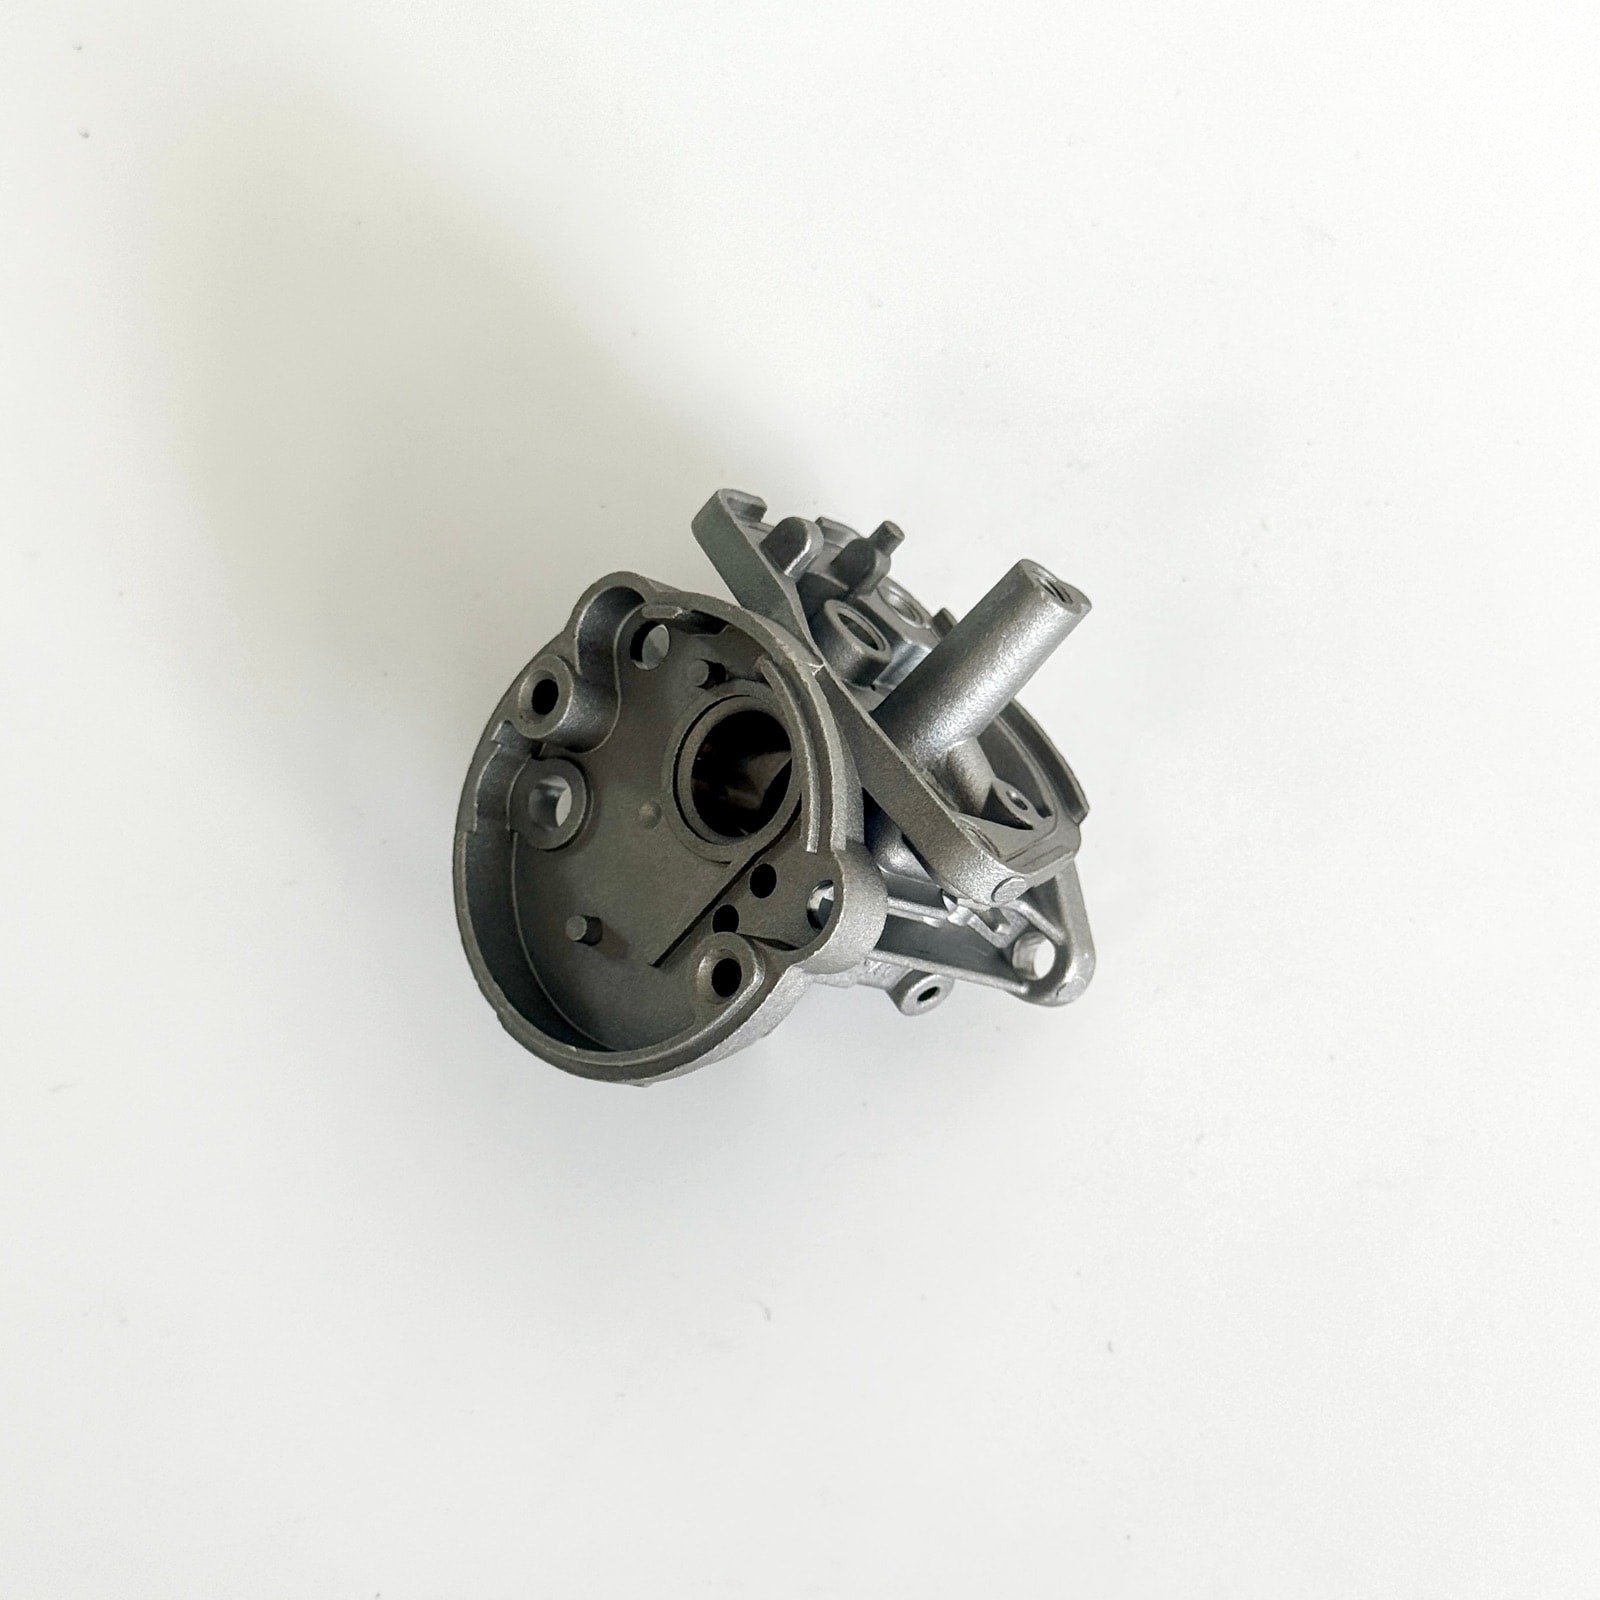
PWK28 Carburetor Body

PWK28 Carburetor Body

AluminumMotorcycle & Two-WheelerDie castingCNC machiningFinishingCosmeticPrecision

A gloss black coat magnifies every flow mark. Knit lines moved off the show faces, 100% pre-coat inspection and fixed blasting keep cosmetic rejects under 1%.

ADC12 (JIS H5302) · 约 300 g
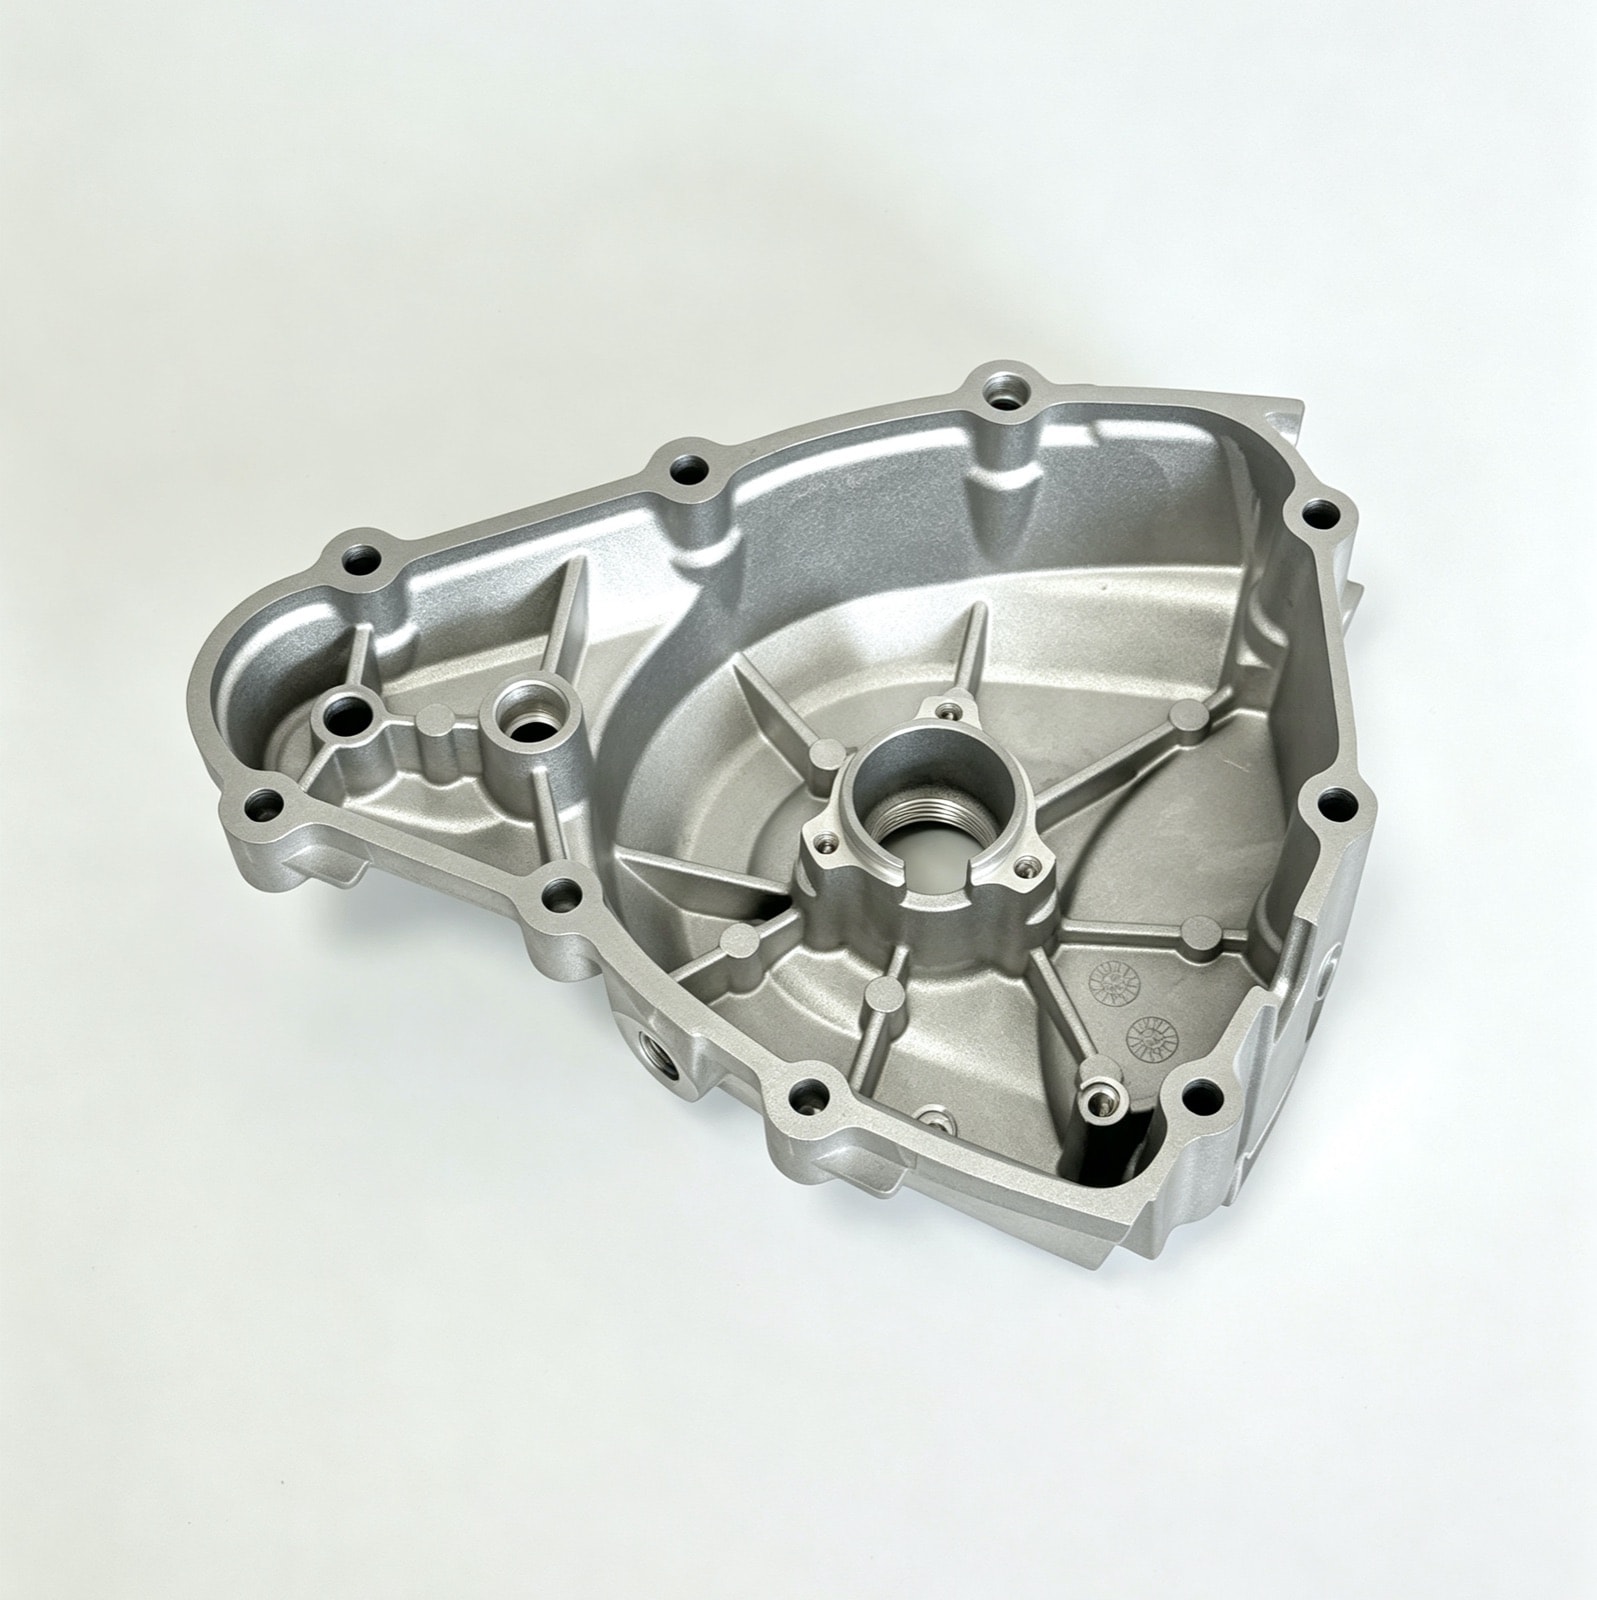
Motorcycle Crankcase Side Cover

Motorcycle Crankcase Side Cover

AluminumMotorcycle & Two-WheelerDie castingCNC machiningFinishingPressure tightPrecision

The 230 mm cover came off the die 0.15 mm out of flat. Even ejection, stress relief and gentle fixturing now hold 0.08 mm; oil-weep complaints are under 0.1%.

ADC12 (JIS H5302) · 约 780 g
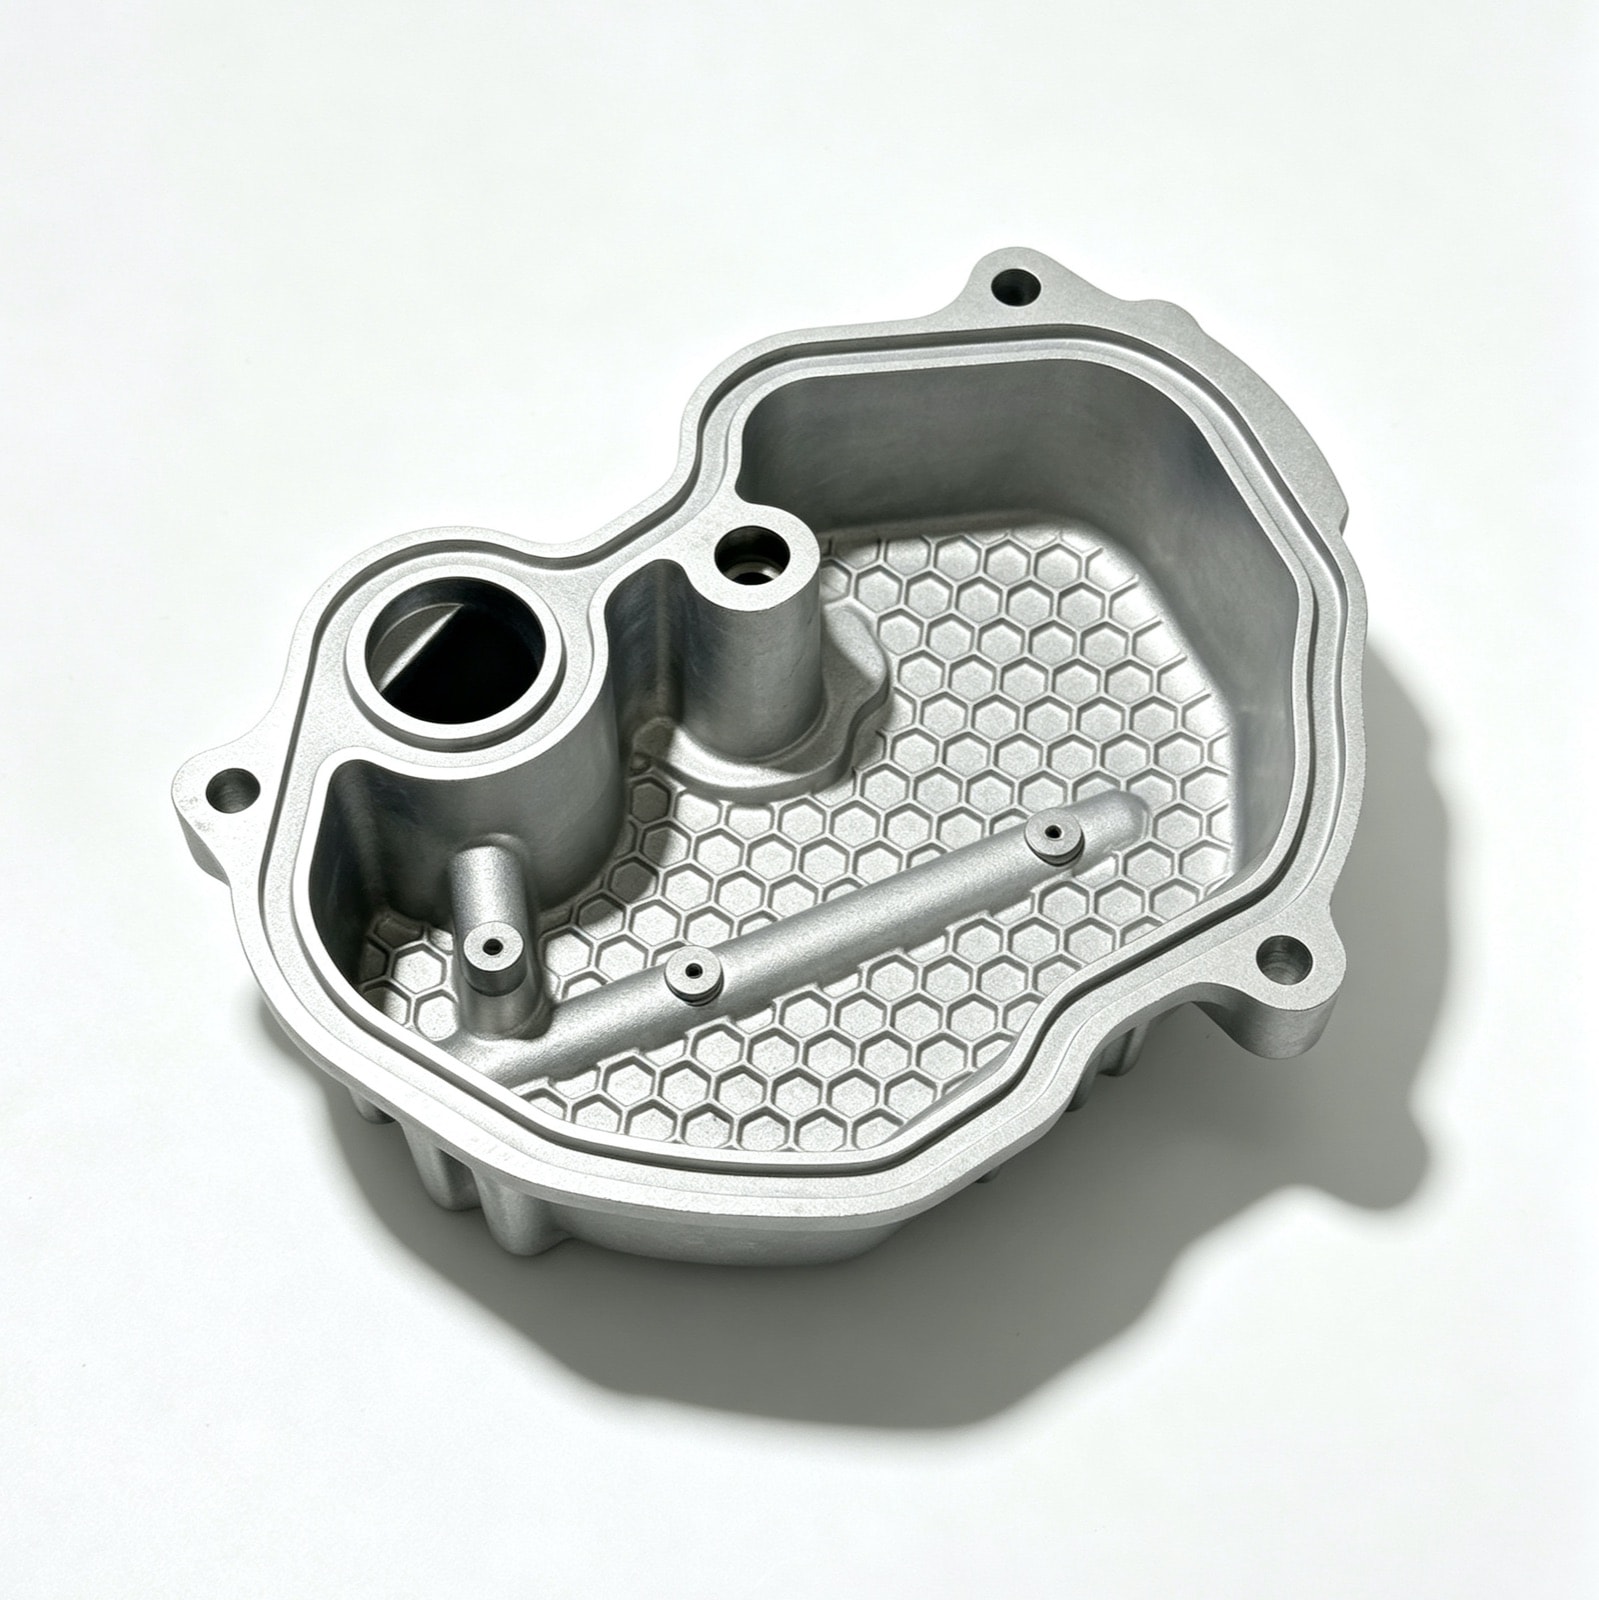
Motorcycle Cylinder Head Cover

Motorcycle Cylinder Head Cover

AluminumMotorcycle & Two-WheelerDie castingCNC machiningPressure tightPrecision

Where honeycomb ribs meet, the metal freezes last and shrinks. Ribs near 0.6× wall, thinned intersections and added venting now pass X-ray at over 99%.

ADC12 (JIS H5302) · 约 460 g
Motorcycle Clutch Pressure Plate

Motorcycle Clutch Pressure Plate

AluminumMotorcycle & Two-WheelerDie castingCNC machiningFinishingThermalPrecision

2 mm fins short-filled at the tips and warped the face. Hotter fin cavities, tip vents and flow-length control now fill over 99%, with runout within 0.05 mm.

ADC12 (JIS H5302) · 约 260 g
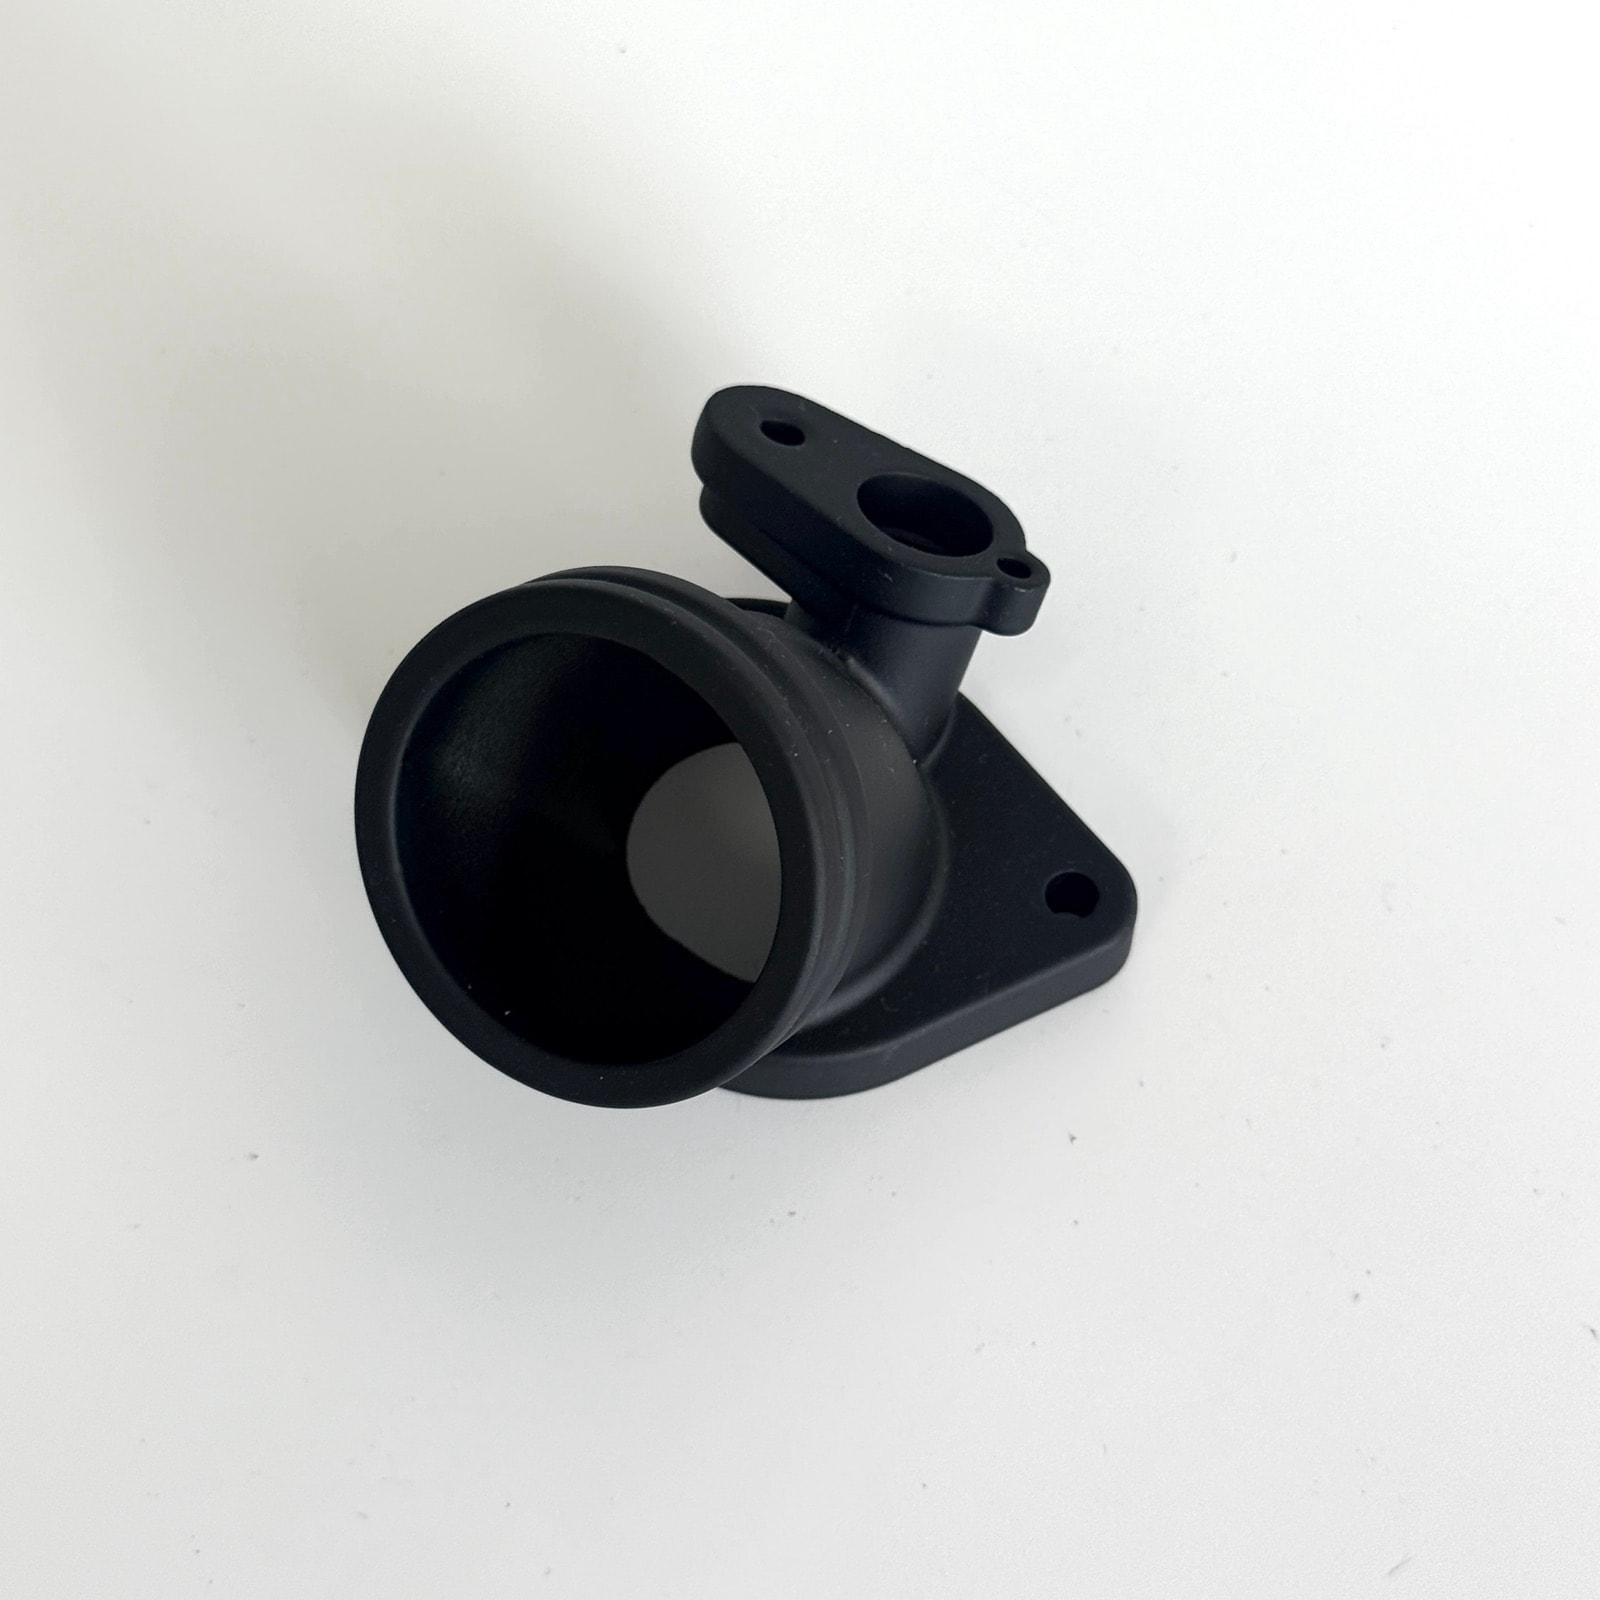
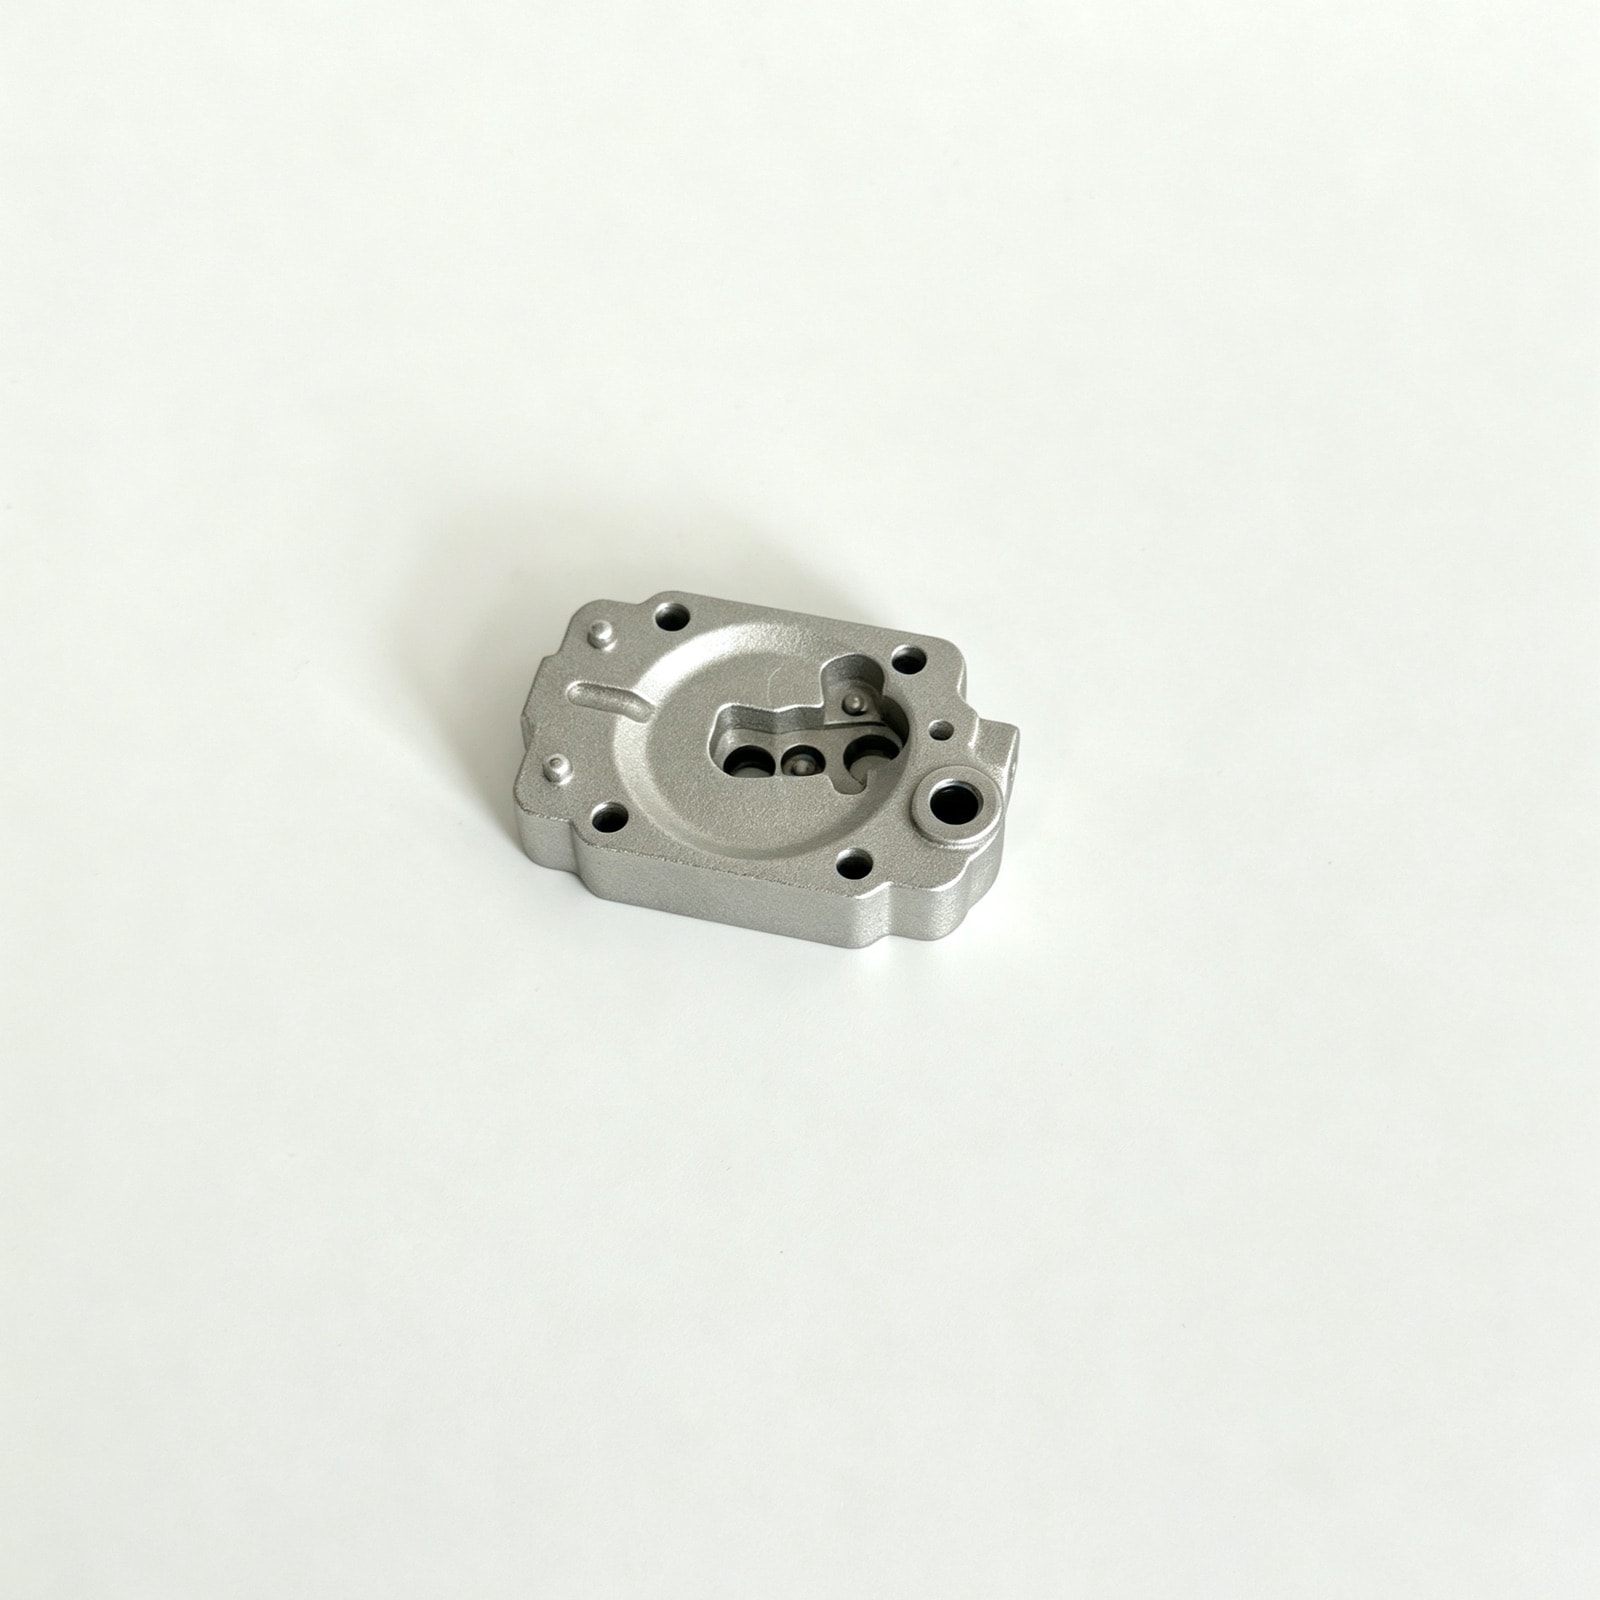
Motorcycle Intake Manifold Adapter

Motorcycle Intake Manifold Adapter

AluminumMotorcycle & Two-WheelerDie castingCNC machiningFinishingPressure tight

Milled in two setups, the flanges ran 0.2 mm out of parallel and the gasket leaked. One-setup machining and 100% leak testing now hold 0.1 mm.

ADC12 (JIS H5302) · 约 150 g
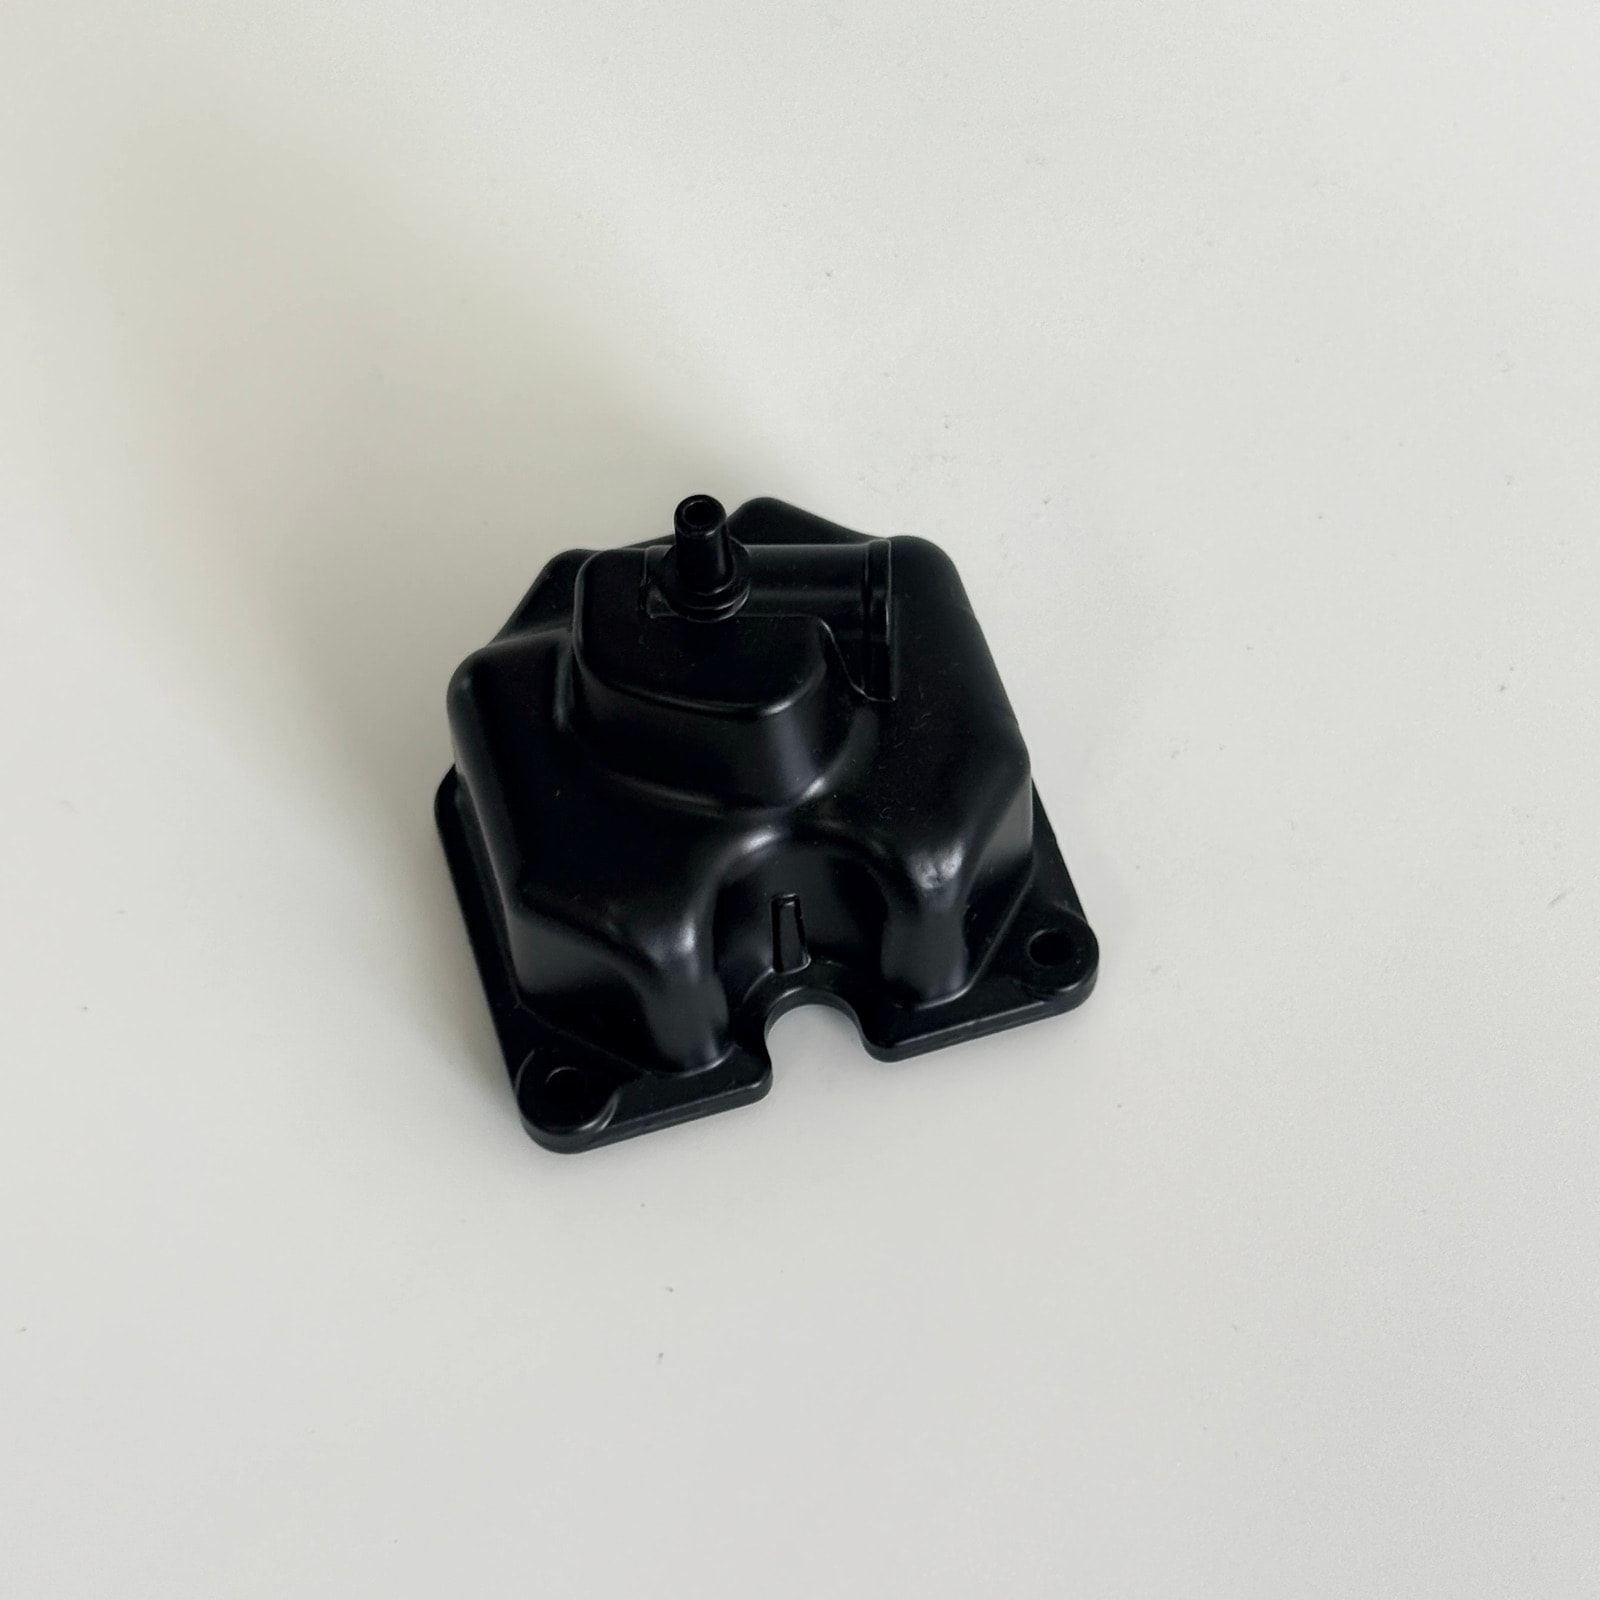
Motorcycle Engine Valve Cover

Motorcycle Engine Valve Cover

AluminumMotorcycle & Two-WheelerDie castingCNC machiningFinishingPressure tightCosmetic

A 6 mm land and a porous breather root caused sporadic leaks. A larger root radius, an overflow and single-pass milling now give 99% first-pass leak yield.

ADC12 (JIS H5302) · 约 130 g